MBBR STP Noida - Sewage Treatment Plant Manufacturers

What-are-the-Applications-of-Commercial-Water-Softeners.webp

September 2, 2026by Netsol Water

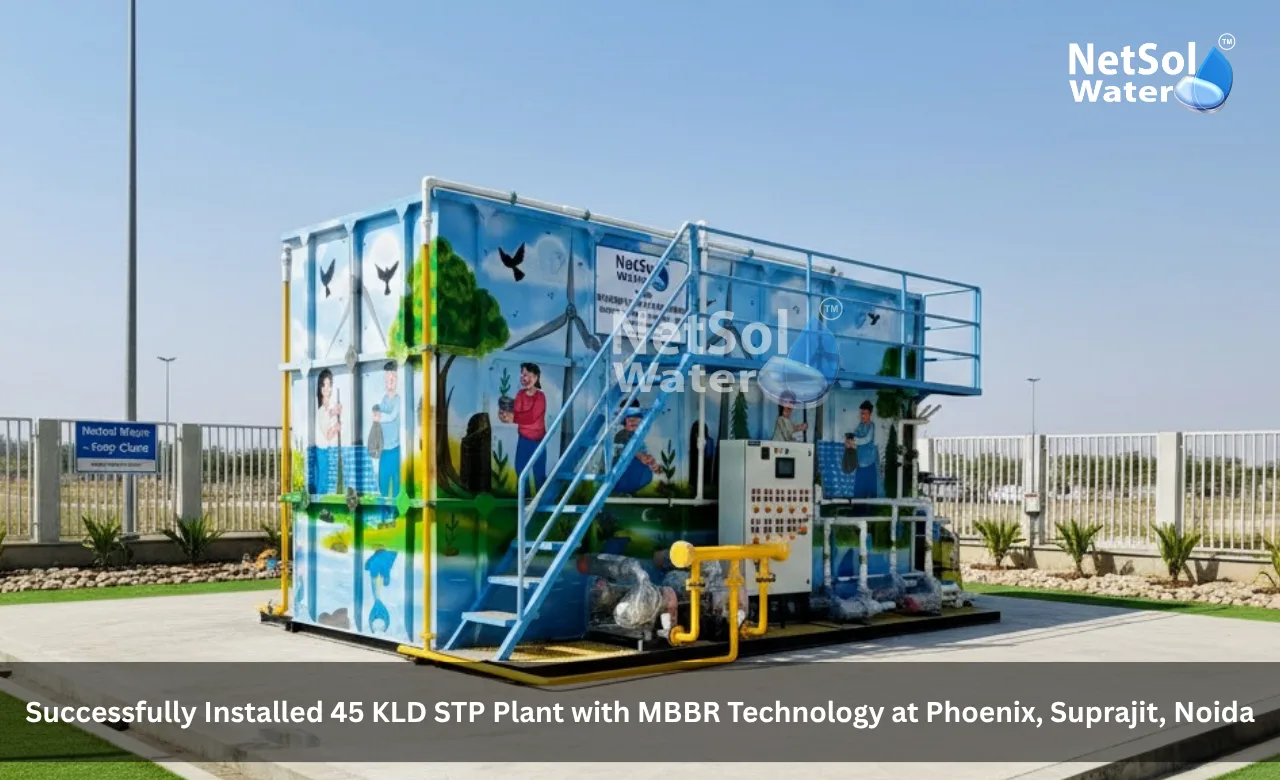
Successfully Installed 45 KLD STP Plant with MBBR Technology at Phoenix, Suprajit, Noida

Effective sewage treatment has become an important requirement for facilities that need to manage wastewater in a responsible and practical manner. At Phoenix, Suprajit, Noida, Netsol Water successfully installed a 45 KLD Sewage Treatment Plant based on MBBR technology. The project was planned to provide a suitable solution for the treatment of sewage generated at the facility and to support better wastewater management.

The client required a treatment plant that could handle the expected sewage load while providing a structured treatment process within the available site conditions. To address this requirement, the project included the design and installation of a 45 KLD sewage treatment system using Moving Bed Biofilm Reactor technology. The selected process offered a biological treatment approach that could be integrated into a compact treatment arrangement.

The project was important because proper sewage treatment helps facilities manage wastewater before it is reused or discharged according to their operational requirements. It also requires careful planning because plant capacity, process arrangement, equipment selection, installation and commissioning all need to work together. This project brought these elements together in one complete treatment solution.

A sewage treatment plant manufacturerĀ in Noida, completed the installation with a focus on creating a functional system that matched the stated project capacity and treatment requirement.

Project Overview

A sewage treatment project must begin with a clear understanding of the wastewater requirement and the operating conditions of the site. The purpose is not simply to place treatment equipment at a location. The complete system must be planned so that wastewater can move through the treatment stages in a controlled manner and receive the required biological and physical treatment.

For Phoenix, Suprajit, Noida, the project focused on installing a 45 KLD Sewage Treatment Plant with MBBR technology. The main objective was to provide an organised treatment system for sewage generated at the facility. The plant was selected according to the stated treatment capacity and was planned as a complete system rather than as an individual piece of equipment.

The scope of the project covered the installation of the treatment plant and the integration of its major process components. This required proper equipment placement, interconnection of the treatment stages and preparation of the plant for operation. Every part of the installation had to support the overall treatment sequence so that the system could operate as one coordinated unit.

The project also required attention to practical site conditions. A treatment plant must fit into the available space and remain accessible for inspection and routine operation. With these considerations in mind, the installation was carried forward through a structured sequence that moved from preparation and equipment placement to connection, testing and commissioning.

Client Details

The client for this project was Suprajit at its Phoenix facility in Noida. The need for a Sewage Treatment Plant generally arises when a facility generates sewage that requires treatment before the treated water can be managed according to its intended use or disposal arrangement. In such situations, the treatment system becomes an important part of the site’s wastewater management infrastructure.

For the client, the requirement centred on a 45 KLD system. This meant that the proposed plant had to be designed around the stated sewage treatment capacity and arranged in a way that supported continuous movement of wastewater through the treatment stages. The project therefore required more than a capacity calculation. It also required a suitable process configuration and proper installation of the supporting equipment.

The client’s requirement was addressed through MBBR-based biological treatment. This approach allowed the plant to use a controlled biological process within the overall sewage treatment arrangement. The installed system was then prepared for operation through systematic testing and commissioning.

Project Location

The project was carried out at Phoenix, Suprajit, Noida. The location was an important part of the planning process because sewage treatment plants must be installed according to the physical conditions of the site. Equipment placement, available working space, connections and access for operation all influence how a plant is installed.

Noida is an active urban and industrial region where facilities may require organised wastewater management systems as part of their infrastructure. For an individual project such as this one, however, the treatment requirement is determined primarily by the sewage generated at the facility and the intended treatment capacity.

At the Phoenix, Suprajit site, the plant therefore had to be positioned and connected in a way that allowed the wastewater treatment process to function properly. The installation had to account for the movement of sewage through the treatment stages while also leaving adequate access for plant operation and maintenance.

The project location also made proper execution important because a treatment plant is a permanent operational system rather than a temporary installation. Once the equipment is positioned and connected, each process stage must work in the intended sequence. This made careful site execution an essential part of the project.

Plant Capacity

Correct plant capacity is one of the first considerations in any sewage treatment project. A plant that is not matched to the intended sewage load can create operational difficulties and reduce the effectiveness of the treatment arrangement. Capacity selection therefore needs to reflect the expected wastewater flow and the purpose for which the plant is being installed.

For the Phoenix, Suprajit project, the installed Sewage Treatment Plant has a capacity of 45 KLD, which means it is designed for a treatment capacity of 45 kilolitres per day. The stated capacity formed the basis for the process arrangement and equipment planning for the project.

The 45 KLD capacity provided the client with a defined treatment framework for managing the sewage generated at the facility. It also established the scale at which the biological treatment system and associated components needed to operate.

Capacity is closely linked with treatment sequence and equipment selection. Each stage has to accommodate the flow entering the plant so that sewage receives adequate treatment as it moves through the system. By installing a system designed for 45 KLD, the project established a treatment arrangement suited to the stated requirement.

Treatment Technology

The choice of treatment technology has a direct effect on how sewage is biologically treated inside the plant. Since the project required a sewage treatment solution with a defined capacity, the treatment process needed to provide effective biological contact within the available system configuration.

The plant at Phoenix, Suprajit, Noida uses MBBR technology, which stands for Moving Bed Biofilm Reactor. MBBR is a biological treatment process in which microorganisms grow on small carrier media placed inside the biological reactor. These microorganisms help break down organic matter present in sewage as the wastewater passes through the reactor.

1. Working Principle of MBBR

The MBBR process creates an environment where microbial growth can take place on the surface of carrier media. Aeration keeps the media moving within the reactor and supplies oxygen for the biological process. As sewage comes into contact with the media, microorganisms attached to the carriers consume and degrade biodegradable pollutants.

The continuous movement of the carrier media helps maintain contact between the wastewater and the biological growth. This allows the biological stage to remain active while the system operates. The process can therefore provide a controlled biological treatment stage within the overall sewage treatment sequence.

2. Role of Aeration

Aeration is an important part of the MBBR process. Air is introduced into the biological tank through an aeration arrangement that provides oxygen for microbial activity. At the same time, the air movement helps keep the carrier media in motion.

The combination of biological growth, wastewater contact and aeration supports the treatment process. Once the biological stage is completed, the treated stream moves forward to the next stage where suspended solids and other remaining materials can be separated.

The use of MBBR technology at the project site therefore provided a clear biological treatment mechanism within the 45 KLD STP arrangement.

Influent Characteristics

Understanding incoming sewage is important before establishing a treatment system because the treatment process must be able to handle the characteristics of the wastewater entering the plant. Parameters such as organic load, suspended solids, turbidity, pH and microbial content can influence treatment requirements.

Sewage typically contains organic matter and suspended impurities that need to be reduced through a controlled treatment sequence before the treated water can be managed further.

The MBBR process was selected to address the biological component of sewage treatment. The treatment system then uses downstream separation stages to help remove the solids generated during the treatment process. This shows why influent understanding and process design are closely connected.

The absence of detailed laboratory figures in the available project brief does not change the installed capacity or technology. It simply means that exact influent values should not be presented as project data unless they are supported by actual test records.

Treatment Process

A sewage treatment plant works through a sequence of stages in which each step prepares the wastewater for the next one. The overall purpose is to gradually remove physical impurities, biodegradable matter and suspended solids so that the treated water reaches the intended quality for its next use or management.

At the Phoenix, Suprajit site, the 45 KLD plant uses MBBR as the central biological treatment technology. The sewage first enters the preliminary treatment stage where larger physical impurities can be removed. This protects the downstream equipment and reduces the chance of blockage in later stages.

Process Stage Description
Preliminary Treatment The incoming sewage is first screened to remove larger materials that should not enter the biological system. Screening helps protect pumps, pipes and other equipment by stopping coarse solids before they move further into the plant. After this stage, the flow moves into the collection and equalisation arrangement. Equalisation helps manage variations in incoming flow and provides a more consistent feed to the biological treatment stage.
Biological Treatment From the preliminary stage, the sewage proceeds to the biological reactor containing MBBR carrier media. Air is supplied to the reactor to support microbial activity and keep the media moving. The microorganisms growing on the carrier surfaces consume biodegradable organic matter in the sewage. As the wastewater remains in contact with the biological media, the organic load is reduced through microbial action. This stage forms the main treatment step in the installed process.
Solids Separation Following biological treatment, the water contains biological solids that need to be separated before the treated stream moves further. The treated mixture therefore passes into a settling stage where heavier solids can separate from the liquid. The settled solids can then be managed through the sludge handling arrangement while the clarified water proceeds to the subsequent treatment stage.
Final Treatment and Treated Water After solids separation, the clarified water can undergo the final treatment steps included in the plant configuration. These stages help improve the treated water quality and prepare it for its intended reuse or disposal arrangement.


The complete process therefore works as a chain. Screening protects the system. Equalisation supports stable flow. MBBR provides biological treatment. Settling separates biological solids. Final treatment prepares the treated water for further use or management.

Major Equipment

Proper equipment selection supports dependable plant operation because every component has a specific role in moving, treating or separating the wastewater. Even when the biological process is the main focus, the supporting equipment must also work correctly for the complete system to perform as intended.

The 45 KLD MBBR STP includes the major equipment and process components required to support the treatment sequence:

Equipment / Component Function
Inlet and Screening Arrangement Forms the first stage by controlling what enters the treatment system.
Pumps and Piping Help move wastewater between the different process sections.
MBBR Biological Reactor The central treatment unit where carrier media and aeration support microbial activity.
Aeration Arrangement Provides the air required for the biological process and also helps maintain movement of the media.
Settling Arrangement Supports separation of biological solids after the MBBR stage.
Sludge Handling Components Used to manage the solids collected during the treatment process.
Interconnecting Pipelines and Valves Link the various sections and control the movement of wastewater between stages.


All of these components contribute to the performance of the plant. A treatment system cannot depend on a single machine or tank. Its operation depends on the combined performance of the process units, pumps, air system, piping and controls.

Installation Process

Successful installation begins with proper planning because treatment equipment must be positioned in a logical sequence and connected correctly. The installation at Phoenix, Suprajit followed a structured approach that allowed the treatment system to be assembled step by step.

The first stage involved preparing the installation area and confirming the placement of the treatment components. The available space had to support equipment installation while also allowing access for operation and maintenance. Once the site arrangement was established, the main process equipment could be positioned according to the planned treatment flow.

The next stage involved connecting the major process units. Piping was used to link the treatment sections so that sewage could travel from the inlet stage to the biological reactor and then toward clarification and treated water handling. Pump connections and other utility connections were also completed as part of the system assembly.

The MBBR reactor and aeration arrangement required particular attention because biological treatment depends on proper air supply and movement of the carrier media. The equipment and connections therefore had to be checked before the plant was prepared for trial operation.

After mechanical and process connections were completed, the system was inspected as a complete installation. This provided a transition from physical installation to commissioning and operational testing.

Plant Commissioning

Commissioning is an important stage because it confirms that the installed plant can operate as a connected treatment system. It provides an opportunity to inspect the equipment, check the connections and verify the movement of wastewater through the process stages before regular operation begins.

For the 45 KLD STP, commissioning involved checking the installed equipment and the connections between the different treatment units. Pumps, aeration equipment and process pathways needed to operate as intended so that wastewater could move through the plant without interruption.

The MBBR section was also checked as part of the commissioning process because the biological reactor is central to the treatment sequence. The aeration arrangement needed to supply air properly while supporting movement of the carrier media inside the reactor.

The commissioning stage also helped identify installation issues that could be corrected before the plant entered regular operation. By testing the system as a complete unit, the project team could confirm that the plant was ready for its intended treatment duty.

This step completed the transition from installation to operational readiness and provided the basis for continued operation of the treatment system.

Treated Water Reuse

Treated water becomes more useful when a facility has a clear plan for how it will manage or reuse the treated stream. Reuse can reduce the need for fresh water for suitable non-potable applications and can form part of a broader wastewater management strategy.

The installed STP provides the client with a treated water stream that can be managed according to the site’s approved requirements and intended reuse practices. The treatment process is designed to reduce pollutants through biological treatment and solids separation before the water moves to its next stage of use or disposal.

The practical value of the plant therefore extends beyond treatment alone. By establishing a dedicated sewage treatment system, the facility has a structured process for managing the wastewater generated at the site.


Results and Performance

Project results help demonstrate whether the installed treatment solution meets its intended purpose. In a sewage treatment project, performance should be assessed through measurable operating data and water quality results rather than broad claims.

The key confirmed outcome for Phoenix, Suprajit is the successful installation and commissioning of a 45 KLD MBBR-based Sewage Treatment Plant. The project established a complete treatment arrangement that moves sewage through preliminary treatment, biological treatment, solids separation and final treated water handling.

The installed capacity provides a defined treatment framework of 45 kilolitres per day. The use of MBBR technology gives the plant a dedicated biological treatment stage in which microbial growth on carrier media supports the reduction of biodegradable pollutants.

The project also resulted in an operational treatment system rather than an incomplete equipment installation. Major equipment was placed and connected so that the treatment stages could function together. Commissioning further prepared the plant for regular operation.

Customer Feedback / Testimonial

Customer feedback provides useful insight into how a completed treatment project is viewed from the client’s side. A direct testimonial can help confirm satisfaction with installation quality, project execution and system performance.

The installation was completed as a 45 KLD MBBR sewage treatment solution for the stated facility. The successful completion of the installation and commissioning indicates that the project moved through the required delivery stages and resulted in a functioning treatment plant.

Read some interesting information for theĀ Effluent Treatment Plant Manufacturer in Delhi

Call to Action

A well-planned sewage treatment system can help facilities manage wastewater through a defined and organised treatment process. The successful installation of the 45 KLD MBBR STP at Phoenix, Suprajit, Noida demonstrates how a project can bring together capacity planning, biological treatment, equipment installation and commissioning to create a complete sewage treatment arrangement.

For facilities that are evaluating similar requirements, choosing the right treatment capacity and process technology is an important starting point. The plant configuration should match the expected wastewater load while allowing the treatment stages and supporting equipment to work together effectively.

Netsol Water, a Sewage Treatment Plant Manufacturer in Noida, provides solutions for sewage and wastewater treatment requirements based on the needs of individual projects. Organisations planning a new treatment plant or looking to improve their wastewater management can contact Netsol Water to discuss their requirements, understand suitable treatment options and request a project consultation.

Contact Netsol Water

Phone: +91-9650608473

Email: enquiry@netsolwater.com

Brine-Management-Options-for-Industrial-RO-Plants.webp

August 31, 2026by Netsol Water

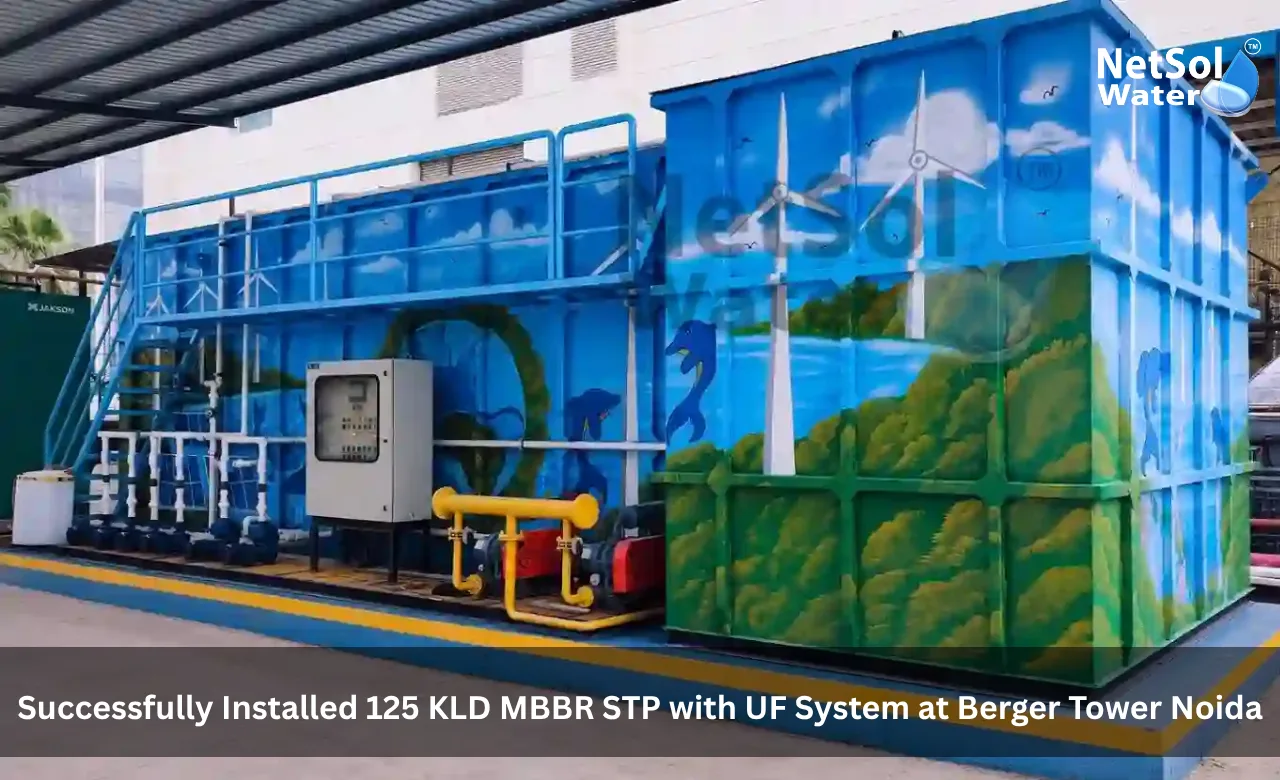
Successfully Installed 125 KLD MBBR STP with UF System at Berger Tower Noida

Managing wastewater is an important part of operating a large commercial facility. A busy building can generate a significant amount of sewage every day from restrooms, housekeeping areas, pantry facilities and other regular activities. Without a suitable treatment plant, this wastewater cannot be managed responsibly or reused for non-potable purposes. This makes a properly designed Sewage Treatment Plant an important part of modern commercial infrastructure.

At Berger Tower in Sector 16B, Noida, Wisdom Colonizers Private Limited required a suitable wastewater treatment solution for its commercial development. The project called for a system that could handle a daily sewage load of 125 KLD while producing treated water suitable for planned reuse. Netsol Water designed and installed a 125 KLD Sewage Treatment Plant based on Moving Bed Biofilm Reactor technology with an Ultrafiltration polishing stage. The project covered design, engineering, manufacturing, supply, installation, testing and commissioning.

The combination of MBBR and UF provided a practical treatment arrangement for a commercial building. The biological treatment stage addressed the main organic load in sewage while UF provided additional filtration before disinfection and reuse. The result was a treatment system designed around the capacity, space and reuse needs of the facility.

Project Overview

A commercial building needs more than a sewage collection system. It needs a treatment process that can manage changing wastewater flow throughout the day and provide treated water at a consistent quality. This project focused on creating such a system for Berger Tower while keeping the treatment arrangement suitable for a commercial site.

Wisdom Colonizers Private Limited engaged Netsol Water for the installation of a 125 KLD STP at Berger Tower in Noida. The project required a complete treatment solution rather than a standalone equipment supply. Netsol Water handled the work from design and engineering through manufacturing, installation, testing and commissioning. The selected treatment arrangement combined MBBR technology with an Ultrafiltration system.

The objective was to treat the sewage generated by the facility and produce water that could support non-potable applications such as flushing and landscaping. The design also considered the practical requirements of a commercial building where water generation can vary depending on occupancy and daily activity.

The project therefore required careful process selection and proper integration of each treatment stage. The treatment sequence had to protect downstream equipment while providing biological treatment and final filtration. With the overall scope established, the next consideration was the client and the nature of the facility where the plant would operate.

Client Details

The client for the project was Wisdom Colonizers Private Limited. Public company records identify Wisdom Colonizers Private Limited as an active private company registered in Noida. Its registered address is in Sector 16B and its business classification falls under real estate activities.

The project was associated with Berger Tower. The commercial development supports office and other commercial activities and therefore requires regular water use across different areas of the facility. Such a building generates wastewater as part of its normal daily operation. Restrooms, housekeeping and other building services contribute to the sewage load that must be collected and treated.

For the client, the treatment plant had to provide a suitable way to manage this wastewater within the facility. The plant also needed to support water reuse where treated water could replace part of the freshwater requirement for non-potable applications.

This requirement made treatment quality an important part of the project. The client was not simply looking for a system that could receive sewage. The plant needed to provide a controlled treatment process that could produce water suitable for the intended reuse applications. The location of the facility added another important consideration.

Project Location

The project was executed at Berger Tower in Sector 16B, Noida, Uttar Pradesh. Public records also associate Wisdom Colonizers Private Limited with Plot No. C-001 A/2 in Sector 16B.

The location is relevant because commercial development in an urban environment often places practical limits on the space available for wastewater treatment equipment. Treatment systems therefore need to use available space carefully while allowing access for operation and maintenance.

Berger Tower is a high-rise commercial building in Noida. Public building information identifies Berger Tower as part of the Delhi One development and places it in Noida. This setting made an organised treatment arrangement important. The system had to fit within the available facility layout and connect properly with the building’s wastewater and treated-water requirements.

The project was therefore approached as a site-specific installation rather than a simple equipment placement exercise. The capacity and treatment technology had to match the wastewater requirement and the conditions of the building. This led directly to the selection of the 125 KLD plant capacity.

Plant Capacity

Plant capacity determines how much wastewater an STP can treat during a normal operating period. Selecting the right capacity is important because the plant must accommodate the expected sewage generation without creating unnecessary treatment capacity. A suitable capacity also helps the treatment process remain stable when wastewater flows vary during different parts of the day.

For Berger Tower, Netsol Water installed a 125 KLD Sewage Treatment Plant. The stated capacity of 125 KLD corresponds to approximately 125,000 litres of sewage treatment capacity per day. The project source identifies the plant as a 125 KLD installation using MBBR technology with UF polishing.

The selected capacity was intended to address the wastewater generated by the commercial facility. Since sewage flow can change with occupancy and daily activity, the treatment arrangement also included an equalization stage. This helped balance variations before the wastewater entered the main biological treatment section.

Capacity alone does not determine plant performance. The treatment technology must also match the wastewater characteristics, available space and quality required at the outlet. For this project, MBBR combined with UF was selected to address those requirements.

Treatment Technology

Selecting the right treatment technology is one of the most important decisions in an STP project. Commercial buildings can experience changing wastewater flows and loads. The treatment process therefore needs to provide effective biological treatment while remaining practical to install and operate.

For Berger Tower, Netsol Water selected Moving Bed Biofilm Reactor technology followed by Ultrafiltration. The system used MBBR as the core biological treatment stage and UF as the polishing stage. Netsol Water identifies this combination as a suitable approach for the commercial tower because it provides advanced treatment without using a complete membrane bioreactor configuration.

1. Moving Bed Biofilm Reactor

The MBBR process uses specially designed carrier media inside the biological reactor. Microorganisms grow on the surface of this media and form a biofilm. When air enters the reactor through the aeration system, the media moves within the wastewater.

The microorganisms use organic matter in the sewage as part of their biological activity. This reduces the organic pollution load and supports the removal of substances such as BOD, COD and ammonia. The moving media also provides a large surface area for microbial growth within the treatment tank.

One practical advantage of MBBR is that the biological treatment stage can provide a high treatment capacity within a relatively compact arrangement. This makes the technology useful for commercial buildings where available plant space may be limited.

2. Ultrafiltration System

The UF system provides an additional filtration stage after biological treatment. Ultrafiltration membranes contain very small pores that physically separate fine suspended matter and microorganisms from the treated water.

At Berger Tower, the UF stage works as a polishing process after the MBBR and clarification stages. This improves the physical quality of the treated water before disinfection and reuse. The project information describes the system as a hollow-fibre UF arrangement.

The combination of biological treatment followed by membrane filtration creates a multi-stage treatment process. Each stage performs a defined function and prepares the water for the next stage. Before selecting these stages, however, the incoming sewage characteristics must be considered.

Influent Characteristics

Understanding the incoming wastewater is necessary before designing any treatment plant. Sewage quality can vary depending on the type of building, the number of users and the activities carried out at the site. Changes in flow can also affect the treatment process.

For a commercial facility such as Berger Tower, the incoming sewage is expected to contain biodegradable organic matter, suspended solids and microorganisms that are commonly associated with domestic sewage. Wastewater from restrooms and other building activities can also contain grease, food-related residues and other contaminants depending on the source.

Treatment system was designed around the expected characteristics of commercial sewage and the required treated-water quality. Pretreatment removed larger materials before the biological stage. Equalization helped balance the hydraulic load. MBBR then reduced the biological pollution load while the UF stage provided additional filtration.

This approach shows why influent assessment and process selection need to work together. Once the incoming wastewater enters the plant, each stage must support the next stage in a controlled sequence.

Treatment Process

A well-planned treatment sequence helps the plant operate consistently. Each stage performs a specific task and prepares the water for the following stage. At Berger Tower, the 125 KLD plant used a sequence that moved the sewage from preliminary screening through biological treatment, clarification, UF filtration and disinfection.

Process Stage Description
Bar Screen Chamber The treatment process begins when incoming sewage enters the bar screen chamber. The screen captures larger solid materials that may be present in the wastewater. Items such as rags, plastic pieces and other coarse debris can create blockages or damage pumps and downstream equipment if they are allowed to pass through. Removing these materials at the beginning protects the rest of the plant. It also makes the following treatment stages easier to operate.
Equalization Tank After screening, the wastewater enters the equalization tank. Commercial sewage does not arrive at a constant rate throughout the day. Flow can rise during busy periods and decrease when building activity is lower. The equalization tank stores the incoming wastewater and helps balance these changes. Mixing keeps the wastewater reasonably uniform and reduces the effect of sudden changes in flow on the biological treatment stage. The balanced flow then moves forward toward the MBBR reactor.
MBBR Tank The MBBR tank serves as the main biological treatment stage. The reactor contains biofilm carrier media that supports the growth of microorganisms. Aeration provides oxygen and keeps the media moving. The microorganisms attached to the carriers use biodegradable matter present in the wastewater. Their biological activity reduces the organic load and supports the removal of pollutants. This stage is central to the overall treatment process because it converts dissolved and biodegradable pollutants into forms that can be separated from the water in later stages.
Secondary Clarifier Following biological treatment, the wastewater contains biological solids and detached biofilm material. The secondary clarifier provides a quiet zone where these solids can settle. As the flow slows down, heavier solids move toward the bottom of the clarifier. The clearer water from the upper part moves toward the next treatment stage while the settled sludge is collected for further handling. This separation is important because the UF system should receive water with reduced suspended solids. The clarifier therefore acts as a bridge between biological treatment and membrane filtration.
Ultrafiltration System The clarified water then passes through the UF system. The hollow-fibre membranes provide fine filtration and remove remaining suspended particles and microorganisms that may still be present after clarification. The project specification identifies UF as the tertiary polishing stage. It also states that the system was designed to produce treated water with low BOD, low TSS and low turbidity for reuse applications. The UF system also includes a membrane backwash arrangement. Regular backwashing helps control membrane fouling and supports stable filtration performance.
Disinfection and Treated Water Storage After filtration, the treated water passes through disinfection. The project uses sodium hypochlorite dosing to reduce remaining pathogens before the water enters treated-water storage. The treated water is then stored and pumped toward the intended reuse points within the building. This final stage completes the treatment chain and makes the water available for suitable non-potable applications.

Major Equipment

Good equipment selection supports reliable treatment and simplifies plant operation. Every major component must perform its intended function while working correctly with the equipment installed before and after it.

The Berger Tower plant included equipment for screening, wastewater equalization, biological treatment, clarification, UF filtration, aeration, disinfection and treated-water transfer.

Equipment / Component Description
MBBR Reactor Used HDPE biofilm carrier media with a high internal surface area. Fine-bubble diffusers and blowers supplied air to the biological stage.
Ultrafiltration Section Used hollow-fibre membranes for final filtration. Automated backwashing helped maintain membrane performance.
Control Panel A PLC-based control panel for automatic start and stop functions, level controls and alarms.
Sludge Handling A gravity thickener and sludge drying bed for sludge management, allowing solids collected during treatment to be handled separately from the treated-water stream.
Chemical Dosing Sodium hypochlorite dosing equipment linked with the treated-water flow so that disinfection could be controlled during plant operation.


Together, these components created a complete treatment system rather than a collection of independent machines. The next challenge was installing them correctly at the project site.

Installation Process

Installation work affects the long-term performance of any wastewater treatment plant. Equipment must be positioned correctly and connected according to the process design. Civil, mechanical, electrical and piping work must also remain coordinated throughout the installation.

At Berger Tower, the project followed a full-scope execution model covering design, engineering, manufacturing, supply, installation, testing and commissioning.

The process began with site planning and preparation. The available installation area was assessed against the plant layout and equipment requirements. The equipment and treatment tanks were then positioned according to the prepared arrangement.

Mechanical connections linked the different treatment stages. Piping connected the wastewater route from screening and equalization to the biological reactor, clarifier and UF system. Treated-water lines connected the final filtration and disinfection stages with the storage and reuse system.

Electrical work connected pumps, blowers, controls and other powered equipment to the control panel. The PLC-based panel provided automatic controls and alarms to support routine operation.

The installation process also included checking equipment alignment, pipe connections and control functions before the plant moved into testing. These checks reduced the risk of avoidable problems during commissioning and prepared the system for controlled startup.

Plant Commissioning

Commissioning is the stage where an installed plant moves from construction into operating condition. It confirms that the equipment works together and that the treatment process functions as intended.

After installation, the project team carried out testing and commissioning of the complete system. Equipment was checked individually and then operated as part of the full treatment sequence. Pumps, blowers, dosing equipment, control systems and membrane operations were examined during the process.

The biological treatment stage required particular attention because MBBR depends on an active microbial population. Operating conditions such as aeration and hydraulic flow have to support the biological process. The UF section was also checked for filtration and backwashing performance.

The commissioning stage provided an opportunity to identify issues before regular operation. Process connections, level controls and alarms were verified and the complete treatment flow was checked from inlet to treated-water storage.

Netsol Water’s published project scope includes testing and commissioning as part of the completed work. This helped establish the operating readiness of the plant before handover.

Treated Water Reuse

Treating wastewater becomes more valuable when the resulting water can be used effectively. Many commercial applications do not require drinking-quality water. Flushing and landscaping are examples where appropriately treated and disinfected wastewater can serve as an alternative water source.

For Berger Tower, the treated-water system was designed to support non-potable reuse. Netsol Water identifies flushing and gardening as reuse applications for the treated water produced by the plant.

This approach allows the facility to make better use of the water already consumed within the building. Instead of treating sewage only for disposal, the plant converts it into a resource for suitable secondary applications.

The UF stage supports this objective by producing clearer water with lower suspended solids and turbidity. Disinfection then provides an additional treatment barrier before reuse. The treated-water storage arrangement makes the water available for distribution according to the facility’s requirements.

The reuse system therefore connects directly with the wider purpose of the STP. It supports wastewater management while creating an opportunity to reduce the use of fresh water for applications that do not require potable water.

Results and Performance

Project results provide a practical measure of whether the treatment solution has addressed the original requirement. For this installation, the main outcomes relate to treatment capacity, process design, filtration quality and water reuse.

The completed plant has a treatment capacity of 125 KLD and uses MBBR followed by UF polishing. The project specification identifies treated-water targets that demonstrate the intended quality level of the treated output and its suitability for designated non-potable reuse:

Parameter Treated-Water Target
BOD Below 10 mg/L
TSS Below 10 mg/L
Turbidity Below 1 NTU


The plant also includes automated controls. A PLC-based control system manages start and stop functions, level controls and alarms. This reduces the need for continuous manual intervention in basic operating functions.

Another important result is the integration of the complete treatment process. Screening protects the equipment. Equalization balances the hydraulic load. MBBR performs biological treatment. Clarification removes settled solids. UF provides fine filtration and disinfection completes the final treatment barrier.

The project also reflects a broader water-reuse objective. Netsol Water lists Berger Tower as a 125 KLD MBBR and UF installation in Noida where treated water is reused for applications including flushing and gardening.

Customer Feedback or Testimonial

Customer feedback can provide useful insight into how a completed treatment system performs from the facility owner’s perspective. It can also help readers understand whether the project addressed the practical needs that existed before installation.

The installation covered design, engineering, manufacturing, supply, installation, testing and commissioning of the 125 KLD MBBR STP with UF. The treatment system was designed to support wastewater management and non-potable water reuse at the commercial facility.

Read some interesting information for theĀ Commercial RO Plant Manufacturer in Delhi

Conclusion

A well-planned sewage treatment system can help a commercial facility manage wastewater in a more organised and useful way. The 125 KLD installation at Berger Tower in Noida demonstrates how biological treatment and membrane filtration can be combined to address the needs of a large commercial facility. MBBR provides the main biological treatment while UF adds a fine filtration stage before disinfection and reuse.

The project also highlights the importance of selecting a treatment system according to capacity, wastewater flow, available space and the intended quality of treated water. By following a complete treatment sequence and integrating automated controls, the plant provides a structured approach to sewage treatment and reuse.

Netsol Water has completed this installation as part of its work in water and wastewater treatment. The company states that it provides design, manufacturing, installation, commissioning and ongoing support for water and wastewater treatment projects. For organisations planning a new facility or upgrading an existing sewage treatment system, working with an experienced Sewage Treatment Plant Manufacturer in Noida can help ensure that the selected technology matches the actual site requirement.

Businesses, commercial developers and facility managers looking for a suitable STP solution can contact Netsol Water to discuss their wastewater generation, available space, treatment goals and water reuse plans. With the right assessment and process design, a sewage treatment plant can become an important part of responsible water management rather than simply a compliance requirement.

Contact Netsol Water

Phone: +91-9650608473

Email: enquiry@netsolwater.com