Commercial RO Plant - Page 2 of 18 - Sewage Treatment Plant Manufacturers

Successfully-Installed-250-LPH-RO-Plant-Water-Cooler-at-Spectrum-Mall-Noida.webp

September 5, 2026by Netsol Water

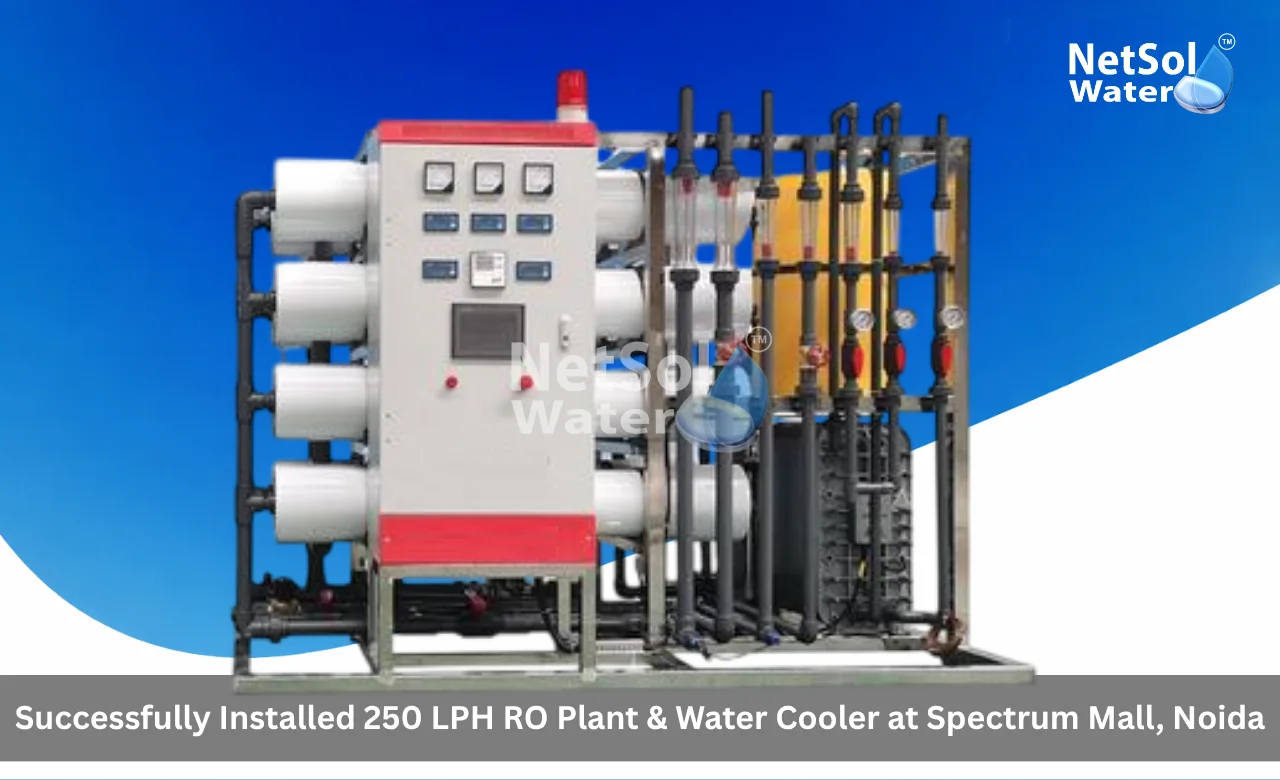
Successfully Installed 250 LPH RO Plant & Water Cooler at Spectrum Mall, Noida

Reliable access to treated drinking water is important for commercial facilities that serve a large number of people every day. Shopping malls need a practical water treatment plant that can support their operational requirements while maintaining a consistent supply of suitable drinking water. For this reason, Spectrum Mall in Noida required a compact and suitable water treatment solution that could provide treated water for its intended use.

Netsol Water successfully completed the installation of a 250 LPH RO Plant along with a water cooler at Spectrum Mall, Noida. The project focused on providing a dedicated reverse osmosis system with suitable cooling support for treated water. The selected capacity was planned according to the stated requirement of the facility and the treatment arrangement was designed to support regular water production.

As a commercial facility, the site needed a solution that could be installed properly and operated in a practical manner. The project therefore involved more than simply supplying an RO unit. It included equipment placement, system connections, testing and commissioning so that the installed setup could function as intended. The combination of RO treatment and a water cooler created a complete drinking water arrangement for the project.

This successful installation reflects Netsol Water‘s approach to delivering practical water treatment plants for commercial applications. As an experienced Commercial RO Plant Manufacturer in Noida, Netsol Water provides treatment solutions based on the required capacity and application. The Spectrum Mall project demonstrates how a properly selected RO system can support the drinking water requirements of a large commercial facility.

Project Overview

A commercial water treatment project must balance water quality, treatment capacity, equipment selection and ease of operation. The Spectrum Mall project was planned with these practical considerations in mind. The primary requirement was to install a water treatment system capable of producing treated water at the required rate while also providing cooled drinking water through a suitable water cooler arrangement.

The project included the installation of a 250 LPH RO plant and water cooler at the mall. The RO system was selected to treat incoming water through the reverse osmosis process. The treated water could then be supplied for the intended drinking water application. The water cooler formed an additional part of the solution by helping provide cooled treated water for users at the facility.

The objective was to deliver a complete and usable water treatment setup rather than an isolated treatment component. The scope therefore covered installation of the RO plant, placement of the related equipment, interconnections and final testing. Each stage was considered as part of the same system so that the treatment and cooling arrangements could work together.

The project also required proper coordination at the site. Commercial premises have fixed spaces and operational activities, so equipment installation needs to be carried out in an organised manner. Once the project requirements were established, the team could proceed with the installation and commissioning activities.

Client Details

Spectrum Mall in Noida is a commercial shopping facility that serves visitors, shoppers and the people working within the premises. Such a facility requires access to convenient drinking water as part of its day-to-day operations. Since the project was intended for a commercial environment, the water treatment system needed to support regular usage through a dedicated treatment and cooling arrangement.

The requirement at the site was focused on treated water production through an RO plant along with a water cooler. The installation was therefore intended to address the facility’s need for a suitable drinking water solution. Instead of depending only on untreated incoming water, the site could use a dedicated treatment process before making the water available for the intended purpose.

The project’s requirements also made equipment selection important. A system with an appropriate treatment capacity could help maintain a consistent supply without introducing unnecessary plant capacity. The chosen 250 LPH RO system provided a defined production rate for the application and was paired with a water cooler to complete the setup.

Netsol Water approached the requirement as a practical commercial water treatment project. The emphasis remained on providing the required treatment capacity and installing the system correctly within the client’s facility.

Detail Information
Client Spectrum Mall, Noida
Facility Type Commercial shopping mall
Requirement Treated drinking water with cooling for visitors and staff
Solution Provided 250 LPH RO Plant with Water Cooler
Installed By Netsol Water


Project Location

Location plays an important role in the planning of any commercial water treatment project. The system must fit within the available site conditions while also supporting the operational needs of the facility. In this project, the installation was completed at Spectrum Mall, Noida, which is a commercial environment with regular human activity.

The nature of a shopping mall makes convenient drinking water an important facility requirement. Visitors and staff use the premises throughout the day, which creates a need for an organised drinking water arrangement. A dedicated RO plant and water cooler can help the facility manage this requirement through a defined treatment and cooling system.

The Noida location also makes local project execution important. Equipment needs to be delivered and positioned at the site with proper planning. Connections between the treatment system and associated components must be completed carefully so that the plant can operate as intended.

For a local installation such as this one, working with an experienced Commercial RO Plant Manufacturer in Noida can help simplify coordination between system design, equipment supply and installation. Netsol Water completed the project by bringing these activities together at the client’s site.

Plant Capacity

Plant capacity determines how much treated water a system can produce within a given period. Selecting the right capacity helps ensure that the equipment is suited to the intended application without unnecessarily increasing the size of the treatment system. For a commercial facility, the selected capacity should match the expected requirement and the planned use of treated water.

The Spectrum Mall project used a 250 LPH RO plant, where LPH means litres per hour. This means the installed RO unit was designed around a rated treatment capacity of 250 litres per hour. The capacity provided a clear production rate for the intended drinking water application.

The use of a 250 LPH system also made the treatment arrangement suitable for a defined commercial requirement. The plant could process incoming water through the RO system and provide treated water for subsequent use through the water cooler arrangement.

Capacity alone does not determine plant performance. The quality of the incoming water, the condition of the equipment and regular operation also affect the overall output. However, selecting an appropriate rated capacity provides the foundation for a suitable treatment solution. In this project, the 250 LPH capacity formed the core of the installed drinking water system.

Parameter Specification
Installed Capacity 250 LPH (Litres Per Hour)
Treatment Technology Reverse Osmosis (RO)
Additional Equipment Water Cooler
Project Site Spectrum Mall, Noida
Plant Type Commercial RO Plant


Treatment Technology

The project used RO as the primary water treatment technology. RO is widely used for water purification because it can reduce dissolved substances from water through a membrane-based separation process. The technology is particularly useful when the incoming water contains dissolved salts and other impurities that need to be reduced before use.

In the Spectrum Mall installation, the RO plant formed the main treatment stage. Incoming water passed through the treatment system and reached the RO membrane after the required pre-treatment stages. The membrane allowed water to pass through while restricting many dissolved impurities.

1. Reverse Osmosis Process

The working principle of RO depends on pressure. The system applies pressure to the incoming water so that it passes through a semi-permeable membrane. The membrane separates a portion of the dissolved material from the water and produces treated water known as permeate.

This process is important because it does not depend only on physical straining. The RO membrane also helps reduce dissolved salts and other dissolved contaminants that conventional filtration may not remove effectively. The result is treated water with reduced dissolved impurity levels.

2. Water Cooling Arrangement

The project also included a water cooler. While the RO plant focused on treatment, the water cooler addressed the temperature and user convenience aspect of the drinking water arrangement. Treated water could be directed into the cooling system so that the facility could provide cooled drinking water for the intended users.

The RO plant and water cooler therefore served different but connected purposes. One handled purification while the other handled cooling. Together they created a more complete drinking water facility for the commercial site.

Influent Characteristics

Understanding the incoming water is an important part of water treatment planning. The design of an RO system depends not only on the required output but also on the quality of the feed water entering the plant. Parameters such as total dissolved solids, hardness, turbidity, iron and microbial content can influence the treatment arrangement and membrane performance.

For the Spectrum Mall project, the available project information does not provide specific laboratory test values for the incoming water. It would therefore not be appropriate to assign exact TDS, hardness, turbidity or microbial figures to the site without supporting test data.

The incoming water for an RO system may contain dissolved salts and other suspended or dissolved impurities. Such characteristics make pre-treatment important because RO membranes require suitable feed conditions for proper operation. The pre-treatment stage helps reduce substances that may affect the membrane and prepares the water for the RO process.

The actual influent characteristics should always be confirmed through proper water analysis when designing or modifying an RO plant. This ensures that the selected equipment and operating conditions match the real site conditions rather than assumed values.

Treatment Process

A properly arranged treatment sequence helps each stage perform its intended function. The treatment journey in an RO plant begins with raw water and continues through filtration and membrane treatment before the water reaches the final user point. In the Spectrum Mall project, the treatment system was installed as an integrated arrangement in which each part supported the next stage.

1. Raw Water Entry

The treatment process starts when incoming water enters the system. Raw water contains the characteristics of the source and may carry suspended particles, dissolved substances and other impurities. The first objective is to condition this water before it reaches the sensitive RO membrane.

2. Pre-Treatment

Pre-treatment prepares the water for membrane treatment. Depending on the system configuration and feed water quality, this stage can include filtration and other conditioning steps. The purpose is to reduce suspended matter and other substances that could interfere with downstream treatment.

The pre-treated water then moves towards the RO unit. Proper pre-treatment helps the membrane receive water in a more suitable condition and supports stable plant operation.

3. RO Membrane Treatment

After pre-treatment, the water enters the RO section. A high-pressure pump provides the pressure required to push the feed water through the RO membrane. The membrane separates a portion of dissolved impurities from the feed stream.

The treated permeate forms the main product water stream. Another stream carries the concentrated portion of the rejected dissolved material away from the membrane section. This separation is a central part of reverse osmosis operation.

4. Treated Water Collection

The treated water is then collected and made available for the next stage of use. Proper storage and transfer arrangements help maintain the flow of treated water from the RO plant to the final drinking water point.

5. Cooling and Final Use

The treated water is connected to the water cooler so that cooled drinking water can be provided at the intended point of use. This completes the treatment journey from raw water entry to final cooled water availability.

Each stage therefore contributes to the overall function of the plant. The pre-treatment prepares the water, the RO membrane performs the main purification step and the water cooler provides the final temperature adjustment required for convenient drinking water use.

Stage Function
Raw Water Entry Incoming water enters the system carrying source characteristics and impurities
Pre-Treatment Reduces suspended matter before water reaches the RO membrane
RO Membrane Treatment High-pressure pump pushes feed water through the membrane; separates permeate and reject
Treated Water Collection Treated water is collected and transferred for the next stage of use
Cooling and Final Use Treated water is connected to the water cooler for cooled drinking water


Major Equipment

Proper equipment selection supports consistent treatment and helps the plant perform according to its intended design. Every major component has a specific role. When the components are selected and connected correctly, the complete system can operate as one treatment unit rather than as separate pieces of equipment.

1. RO Plant

The 250 LPH RO plant is the main treatment equipment in the project. It contains the treatment components required to process the incoming feed water and produce treated water through reverse osmosis.

2. RO Membrane

The RO membrane is the central separation component of the system. It allows water to pass through while restricting a significant portion of dissolved impurities. The quality and condition of the membrane directly affect the treatment performance of the RO unit.

3. High-Pressure Pump

The high-pressure pump provides the pressure needed for membrane operation. Without sufficient pressure, water cannot pass through the RO membrane at the required rate. The pump therefore supports the membrane separation process and contributes to the production of treated water.

4. Pre-Treatment Filters

Pre-treatment filters help prepare incoming water before it reaches the RO membrane. Their function is to reduce suspended material and other impurities that may affect downstream treatment.

5. Water Cooler

The water cooler forms the final part of the installed solution. It receives treated water and provides cooled water for the intended drinking application. Its inclusion made the project more suitable for a facility where treated drinking water also needed to be conveniently cooled.

Equipment Role in the System
RO Plant (250 LPH) Main treatment equipment; processes feed water through reverse osmosis
RO Membrane Central separation component; restricts dissolved impurities
High-Pressure Pump Provides pressure needed to push water through the RO membrane
Pre-Treatment Filters Reduce suspended material before water reaches the membrane
Water Cooler Receives treated water and provides cooled drinking water


Installation Process

Successful installation depends on proper planning before the equipment is put into operation. The site must provide enough space for equipment placement and the required connections must be arranged carefully. For a commercial project, the installation process also needs to fit within the practical conditions of the facility.

The work began with preparation of the installation area. The team assessed the designated space and arranged the equipment so that the RO plant and water cooler could be positioned appropriately. Proper placement helps technicians access the system for operation and future maintenance.

Once the equipment positions were established, the major plant components were placed at their planned locations. The RO unit and related components were aligned according to the treatment flow. Attention was then given to the required water and interconnecting lines.

The team connected the raw water feed to the treatment system and completed the necessary connections between the pre-treatment stages and RO section. The treated water outlet was then connected to the downstream arrangement leading towards the water cooler.

After mechanical and piping connections were completed, the electrical and operational connections were checked. This stage ensured that pumps and other powered components could work correctly with the installed system.

The final part of installation involved inspecting the complete arrangement. Connections were checked for proper fit and the system was prepared for testing. This systematic approach helped move the project from physical installation to operational commissioning.

Plant Commissioning

Commissioning is necessary before a treatment plant begins regular operation. It allows the installation team to confirm that the equipment, connections and controls function correctly. It also provides an opportunity to identify and correct installation issues before the client begins routine use.

For the Spectrum Mall project, commissioning involved starting the installed system and checking its operation under working conditions. The team verified the functioning of the treatment components and observed the water flow through the plant.

The RO section was checked to ensure that the high-pressure system and membrane treatment process were operating properly. The treated water flow was also reviewed as part of the commissioning activity. The water cooler was checked to ensure that the downstream cooling arrangement worked with the treated water supply.

The complete system was inspected for proper operation and the necessary connections were reviewed during the testing process. These checks helped confirm that the installed plant was ready for its intended commercial application.

Commissioning therefore acted as the final technical stage before regular use. It linked the completed installation with actual operating conditions and allowed the system to move into service with the required checks completed.

Treated Water Reuse

Treating water is most useful when the resulting water can be put to practical use. In a commercial facility, the final purpose of treatment should remain connected to the original requirement. For this project, the installed system was intended to support the drinking water arrangement at Spectrum Mall.

The treated water produced by the RO plant could be supplied to the associated water cooler. This allowed the facility to combine purification and cooling within the same setup. The resulting arrangement provided treated and cooled water for the intended drinking application.

The value of the system therefore extended beyond the RO membrane itself. By connecting the treated water stream with the water cooler, the project addressed both water treatment and user convenience. This integrated approach made the installation more practical for the commercial environment.

Results and Performance

Project results provide a practical measure of whether the installed system meets its intended purpose. For the Spectrum Mall installation, the key outcome was the successful completion and commissioning of a 250 LPH RO plant along with a water cooler.

The project delivered a dedicated treatment setup rather than relying on a simple drinking water arrangement without purification. The RO plant introduced membrane-based treatment into the facility’s water supply process. The addition of the water cooler then provided cooled treated water as part of the final user arrangement.

One of the measurable project parameters is the installed treatment capacity of 250 litres per hour. This established a clear production rate for the RO unit and aligned the system with the defined project requirement.

The installation also brought together treatment equipment and cooling equipment within the same project. This reduced the need to treat purification and cooling as separate facility requirements. The completed setup therefore provided a more coordinated approach to the stated drinking water requirement.

Confirmed Outcome Status
Installation of 250 LPH RO Plant Completed
Water Cooler Installation & Connection Completed
System Testing & Commissioning Completed
Laboratory/TDS Data Not provided — not included in this case study


Customer Feedback/Testimonial

Customer feedback is useful because it reflects the practical response to a completed installation. It can indicate whether the delivered system matched the original requirement and whether the overall project was handled satisfactorily.

250 LPH RO plant and water cooler were successfully installed at Spectrum Mall, Noida. The successful completion of the installation was executed according to the available requirement. The treatment system and water cooler were brought together as the intended commercial drinking water solution.

Call to Action

A properly planned commercial drinking water system can help a facility address its treatment needs through a defined and organised process. The successful installation at Spectrum Mall, Noida shows how a 250 LPH RO plant and water cooler can be combined to create a practical treatment and drinking water arrangement for a commercial site.

Netsol Water provides water treatment solutions for different commercial applications and focuses on selecting systems according to the required capacity and intended use. As a Commercial RO Plant Manufacturer in Noida, Netsol Water can support clients with RO plant selection, equipment supply, installation and commissioning based on project requirements.

For organisations looking for a suitable RO solution for a commercial facility, the first step is to assess the required water capacity, incoming water quality, intended use and available installation space. These factors help determine the right treatment configuration.

Contact Netsol Water to discuss your commercial water treatment requirement and request a suitable RO plant solution for your facility. A project-specific consultation can help identify the appropriate treatment capacity and equipment arrangement for your application.

Read some interesting information for the Sewage Treatment Plant Manufacturer in Noida

Contact Netsol Water

Contact Details
Phone +91-9650608473
Email enquiry@netsolwater.com


What-are-the-Applications-of-Commercial-Water-Softeners-2.webp

September 3, 2026by Netsol Water

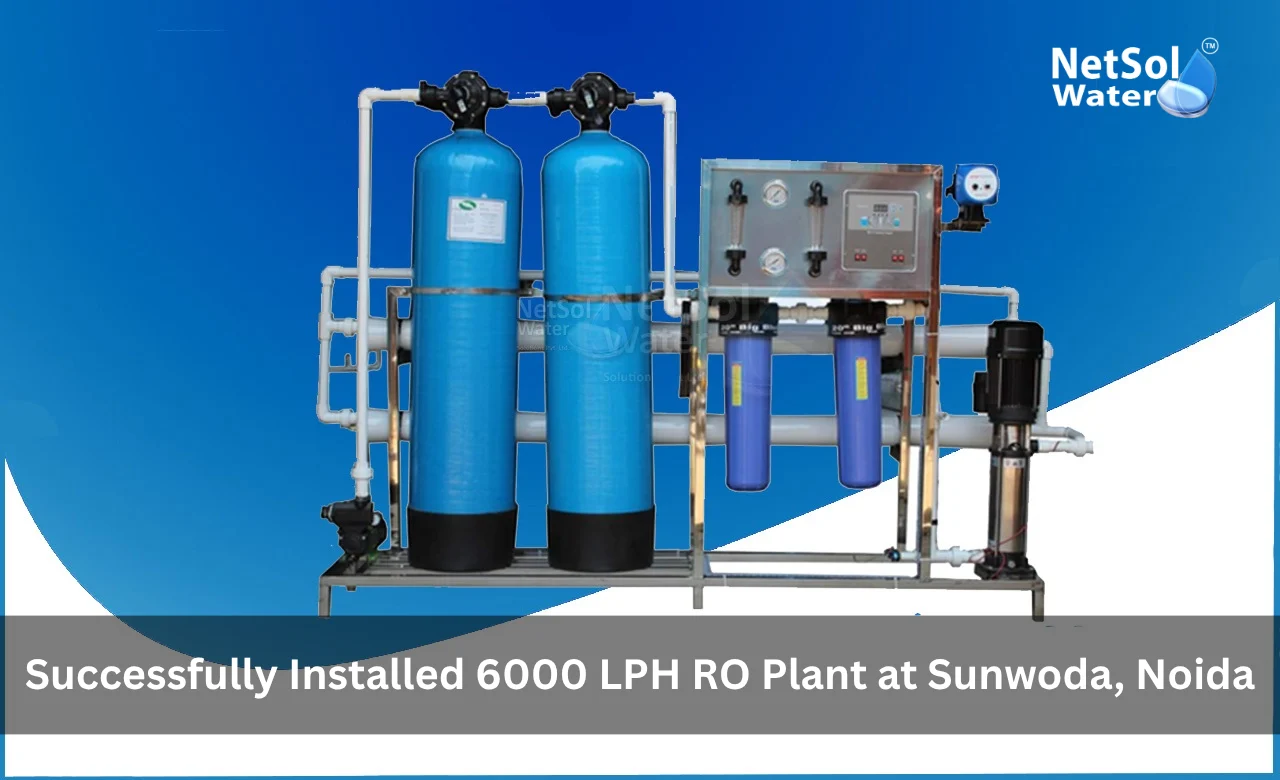
Successfully Installed 6000 LPH RO Plant at Sunwoda, Noida

Reliable water treatment is important for facilities that need a steady supply of treated water for their daily operations. At Sunwoda in Noida, a 6000 LPH RO plant was successfully installed to address the site’s requirement for treated water. The project focused on providing a suitable water purification system with the required treatment capacity while maintaining a practical process for regular operation and maintenance.

Sunwoda is part of Sunwoda Electronic Co., Ltd. which operates in the lithium-ion battery and new energy sector. The company has established operations in India and has maintained an international manufacturing and business presence. Sunwoda’s first overseas production base was established in India in 2017.

For a facility where water is required as part of ongoing operations, selecting an appropriately designed treatment system is important. The installed RO plant was planned around the required capacity and the need to convert incoming water into treated water suitable for the intended application. The project therefore involved more than simply placing an RO unit at the site. It required proper equipment selection, plant installation, interconnections, testing and commissioning so that the system could operate as an integrated treatment unit.

The successful installation demonstrates how a properly selected RO system can address a commercial or industrial water treatment requirement without adding unnecessary complexity to the operating process. It also highlights the role of an experienced commercial RO plant manufacturer in Noida in delivering a treatment solution according to the practical needs of a project.

Project Overview

A commercial water treatment project must begin with a clear understanding of the required water quantity and the intended use of the treated water. The Sunwoda project was developed with this basic principle in mind. The main objective was to install a 6000 LPH RO plant that could provide the required treated water capacity for the facility.

The scope of work involved the installation of the RO treatment system at the client’s site in Noida. The project required the treatment equipment to be positioned correctly and connected so that raw water could move through the treatment stages before reaching the treated water outlet. Attention to plant arrangement was important because every stage had to work in the correct sequence.

The project also required practical coordination between equipment installation and system commissioning. A water treatment plant is expected to operate as one connected system rather than as separate pieces of equipment. Therefore, pumps, filters, membranes, valves, pipework and electrical connections need to function together.

The 6000 LPH capacity provided a defined treatment output for the project. This made it possible to design the plant around a clear production rate instead of using an unnecessarily large system. For the client, the objective was to have an appropriate water treatment arrangement that could support its operational requirement while remaining manageable for routine use.

This approach reflects the working method expected from a professional Commercial RO Plant Manufacturer in Noida. The focus is not only on supplying the RO equipment but also on ensuring that the complete installation works as an operational water treatment system.

Client Details

Sunwoda is a global company operating in the lithium battery and new energy sector. Sunwoda Electronic Co., Ltd. was established in 1997 and has developed businesses covering 3C batteries, power batteries, energy storage batteries, energy services and smart hardware. The company has also established production and business locations outside China including India.

The presence of Sunwoda in India creates a requirement for supporting infrastructure that can serve its local operations. Water treatment is one such requirement where the quality and availability of treated water need to match the practical needs of the facility.

For this project, the requirement was addressed through the installation of a 6000 LPH RO plant. The system provided a dedicated treatment process for incoming water. Instead of depending on untreated water for the intended application, the facility could process the incoming water through a defined purification system.

The project therefore addressed an important part of the facility’s water management requirement. By installing the treatment plant at the site, the client gained a dedicated system designed around a known treatment capacity. This also created a structured process for handling the incoming water before it was directed to the intended point of use.

Detail Information
Client Name Sunwoda (Sunwoda Electronic India Pvt. Ltd.)
Parent Company Sunwoda Electronic Co., Ltd.
Sector Lithium-ion battery and new energy sector
Company Established 1997
First Overseas Production Base (India) 2017
Business Coverage 3C batteries, power batteries, energy storage batteries, energy services, smart hardware


Project Location

The project was completed at Sunwoda in Noida, Uttar Pradesh. Noida is an important industrial and commercial centre in the National Capital Region and hosts facilities belonging to companies from different sectors. Sunwoda Electronic India Pvt. Ltd. is publicly listed with locations in Noida and Greater Noida.

The location of a treatment plant matters because the system has to fit into the available site conditions. Equipment placement, access for operation, pipe routing, electrical connections and maintenance space all influence how a plant can be installed.

At an operating industrial or commercial facility, installation work also needs to be coordinated with the existing site environment. The treatment system must be placed in a practical position while allowing operators and maintenance personnel to reach the major components when required.

For the Sunwoda installation, the site requirement was addressed by arranging the 6000 LPH RO plant as a connected treatment system. The work focused on creating the required connections between the raw water source, treatment equipment and treated water discharge point.

The Noida location also highlights the importance of working with a supplier that understands local project execution requirements. A Commercial RO Plant Manufacturer in Noida can coordinate the design, installation and commissioning process with greater attention to the practical conditions of the project site.

Plant Capacity

Plant capacity is one of the most important considerations when selecting a water treatment system. A plant that is too small may not provide the required amount of treated water. A plant that is much larger than the requirement may increase equipment size, cost and operating requirements without providing a practical advantage.

For the Sunwoda project, the installed capacity was 6000 litres per hour (6000 LPH). This means the RO system was designed to produce treated water at a nominal rate of 6000 litres per hour under the applicable operating conditions.

The selected capacity provided a clear treatment output for the facility. It allowed the system to be planned around a defined flow rate rather than relying on an unspecified or variable treatment arrangement.

Capacity also affects the sizing of associated equipment. The feed system, pre-treatment arrangement, RO membrane assembly, high-pressure pump and treated water connections must all support the required flow. Proper coordination between these components is necessary for the plant to perform as intended.

The 6000 LPH capacity therefore served as the central design point for the installation. It guided the selection and arrangement of the major treatment components and established the expected production capacity of the system.

Parameter Specification
Installed Capacity 6000 LPH (Litres Per Hour)
Treatment Technology Reverse Osmosis (RO)
Project Site Sunwoda, Noida, Uttar Pradesh
Plant Type Commercial / Industrial RO Plant
Design Basis Defined flow rate matched to facility requirement


Treatment Technology

Reverse Osmosis was selected as the main treatment technology for the project. RO is a membrane-based purification process that separates dissolved substances from water by applying pressure to push water through a semi-permeable membrane.

The technology is widely used when the objective is to reduce dissolved salts and other impurities from incoming water. However, the RO membrane performs best when the water entering it has already passed through suitable pre-treatment. This is why the overall plant design needs to include more than the RO membrane itself.

1. Reverse Osmosis Process

During RO treatment, feed water is pressurised and directed towards the membrane assembly. The membrane allows a portion of the water to pass through while restricting many dissolved salts and other contaminants. The water that passes through the membrane is collected as permeate or treated water.

The remaining water contains a higher concentration of rejected substances and leaves the membrane system as reject or concentrated water. The exact recovery and rejection values depend on feed water characteristics, membrane selection, operating pressure and plant design.

For the Sunwoda project, the RO system formed the main purification stage after the incoming water had passed through the required pre-treatment arrangement. This sequence helped protect the RO membranes and supported consistent operation.

2. Importance of Pre-Treatment

Pre-treatment is necessary because suspended particles, turbidity, hardness and other unwanted substances can affect membrane performance. Depending on the incoming water characteristics, filtration and conditioning stages may be used before the RO membranes.

The purpose of pre-treatment is not to replace RO. Instead, it prepares the feed water so that the membrane stage can perform effectively. This relationship between pre-treatment and RO is an important part of proper plant design.

3. Treated Water Production

After the feed water passes through the RO membranes, the treated stream is collected and directed towards the treated water storage or use point. The final arrangement depends on the specific site connections and the intended application.

The selected RO process therefore provided a structured method of reducing dissolved impurities from the incoming water and producing treated water at the required plant capacity.

Influent Characteristics

Understanding the incoming water quality is essential before designing or operating an RO plant. Water can contain different levels of dissolved salts, hardness, suspended particles and other impurities. The treatment system must be selected according to these characteristics.

For this project, detailed laboratory values for parameters such as TDS, hardness, turbidity, iron and microbial content were not provided. Therefore, no specific test figures are assigned to the Sunwoda installation.

Instead, the treatment arrangement should be understood in general terms. Incoming water to an RO plant may contain suspended matter and dissolved substances that can affect the performance of the treatment equipment. If such contaminants reach the membrane without adequate pre-treatment, they may cause fouling, scaling or a reduction in membrane performance.

The pre-treatment arrangement therefore acts as an important protective stage. Filtration can reduce suspended material before the water reaches the RO system. Where hardness or scaling potential is a concern, suitable conditioning can also be incorporated according to the actual water analysis.

A proper RO design should always consider the source water characteristics before final equipment selection. The absence of exact influent values in the available project information means that this case study does not assign numerical values that cannot be verified.

Treatment Process

A successful RO plant depends on a properly arranged treatment sequence. Each stage has a specific purpose and prepares the water for the next stage. A clear treatment sequence also makes it easier to monitor plant performance and identify operating problems.

1. Raw Water Entry and Pre-Treatment

The process begins when incoming water enters the treatment system. Before reaching the RO membranes, the water passes through the necessary pre-treatment stages. The aim is to remove or reduce contaminants that could affect downstream equipment.

Filtration is an important part of this stage because suspended material can damage or foul the RO membranes. Depending on the actual raw water quality, different filtration and conditioning arrangements can be used.

The pre-treated water then moves towards the RO feed system. At this stage, the objective is to provide water with suitable characteristics for membrane treatment.

2. Pressure Generation

RO requires pressure to overcome the natural movement of water across the membrane. A high-pressure pumping arrangement therefore feeds the conditioned water to the RO membrane assembly.

The pump provides the required pressure and flow so that the membranes can perform the separation process. Proper pump selection is important because insufficient pressure can affect production while unsuitable operating conditions can increase stress on the system.

3. Membrane Separation

The pressurised water enters the RO membrane vessels. Inside the membrane assembly, water is separated into permeate and reject streams.

The permeate passes through the membrane and is collected as treated water. The rejected portion carries a higher concentration of dissolved substances and is discharged through the reject line according to the site arrangement.

This is the main purification stage of the plant. The membrane system therefore determines much of the treated water quality and production performance.

4. Treated Water Collection

The treated water leaving the membrane system is directed towards the designated treated water collection arrangement. It can then be stored or supplied to the intended point of use according to the facility’s requirements.

The complete process creates a controlled water treatment path from raw water entry to treated water production. Each stage supports the next and helps maintain the overall operation of the plant.

Stage Function
Raw Water Entry & Pre-Treatment Removes/reduces contaminants and suspended material before water reaches the RO membranes
Pressure Generation High-pressure pump feeds conditioned water to the RO membrane assembly
Membrane Separation RO membrane vessels separate water into permeate and reject streams
Treated Water Collection Permeate is collected and directed to storage or the point of use


Major Equipment

Proper equipment selection is necessary for stable plant operation. Every major component has to match the required treatment capacity and work correctly with the other parts of the system.

1. Pre-Treatment Equipment

The pre-treatment section supports the RO membranes by reducing suspended particles and other contaminants from the incoming water. Filtration equipment forms an important part of this section and helps protect the downstream membrane stage.

The specific arrangement depends on the quality of the incoming water. A correctly designed pre-treatment section reduces the load placed on the RO membranes and can support more consistent operation.

2. Feed and High-Pressure Pumps

Pumps move water through the treatment system. The feed arrangement delivers water to the treatment stages while the high-pressure pump provides the pressure required for membrane separation.

The performance of these pumps directly affects the flow reaching the RO membrane assembly. Correct sizing is therefore important for maintaining the required treatment capacity.

3. RO Membrane Assembly

The RO membrane system is the central purification component. It receives pressurised water and separates the permeate stream from the reject stream.

Membrane selection and arrangement must correspond to the required plant capacity and the characteristics of the feed water. The membrane vessels also need proper connections to allow pressure, flow and maintenance requirements to be managed.

4. Control and Piping Arrangement

Valves, pipelines and control components connect the different sections of the plant. These components guide water through the required path and allow the operators to control the treatment process.

A properly installed piping arrangement also supports maintenance because individual sections can be accessed and isolated when required.

Together, these components form the working structure of the 6000 LPH RO plant. The role of a Commercial RO Plant Manufacturer in Noida extends to coordinating these components so that the complete system functions as one treatment unit.

Equipment Role in the System
Pre-Treatment Equipment Reduces suspended particles and contaminants, protecting the RO membranes
Feed Pump Delivers incoming water to the treatment stages
High-Pressure Pump Provides the pressure required for membrane separation
RO Membrane Assembly Central purification component; separates permeate from reject stream
Valves, Pipelines & Controls Guide water through the required path and allow process control


Installation Process

Plant installation requires careful planning because treatment equipment has to be positioned correctly and connected according to the process design. Poor equipment placement or incorrect connections can affect both operation and maintenance.

The installation process began with site preparation. The available area was assessed for equipment placement and access. The objective was to establish a practical layout in which the treatment components could be connected in the correct sequence.

Once the installation area was prepared, the major equipment was positioned according to the planned arrangement. Pumps, filtration equipment and the RO unit were placed so that water could move through the system without unnecessary routing.

The next stage involved connecting the water pipelines. Raw water connections were linked to the treatment system while the treated water outlet and reject lines were arranged according to the process requirements.

Electrical connections were also completed for the pumps and control components. These connections were checked to ensure that the equipment could be operated in the required sequence.

After the physical installation was completed, the team inspected the connections and equipment alignment. This stage helped identify any installation issues before the plant moved into commissioning.

The complete installation process was therefore treated as an integrated activity rather than simply placing individual machines at the facility.

Plant Commissioning

Commissioning is the stage that confirms whether an installed treatment plant can operate properly. It allows the project team to test the system under operating conditions and identify issues before regular operation begins.

For the 6000 LPH RO plant, commissioning involved checking the installed equipment, water connections, electrical systems and process flow. The pumps and associated components were operated to confirm that water moved through the intended treatment path.

The team also checked the RO section to make sure that feed water reached the membrane assembly and that the permeate and reject streams followed the designed routes.

Operating parameters were reviewed during testing. This type of verification is important because a plant can appear correctly installed while still having problems with pressure, flow, leakage, electrical connections or equipment sequence.

Commissioning also provides an opportunity to confirm that the plant operates according to the project requirement. Once the system was checked and the installation was found to be functioning as intended, it could move towards regular operation.

Treated Water Reuse

The value of a treatment plant depends not only on how the water is purified but also on how the treated water is used after production. Effective use of treated water can help a facility make better use of its water treatment infrastructure.

For the Sunwoda project, the 6000 LPH RO plant provides treated water for the intended site requirement. However, detailed information about the exact end-use application and internal reuse pattern was not provided.

Therefore, it would not be appropriate to assign a specific reuse process without confirmation from the client. The available project information confirms the installation of a dedicated RO treatment system designed to produce treated water at 6000 LPH.

The treated water can be directed towards the designated site application through the plant’s outlet arrangement. This provides the facility with a controlled source of treated water rather than sending untreated incoming water directly to the intended use point.

Where the site has suitable provisions, treated water can also be integrated with storage and distribution arrangements. The actual reuse pattern should be determined according to the client’s operational requirements and water quality specifications.


Results and Performance

Project results provide the clearest indication of whether a treatment installation has addressed its intended purpose. For the Sunwoda project, the main measurable outcome was the successful installation and commissioning of a 6000 LPH RO treatment system.

The plant established a dedicated water purification process at the site. The installed capacity provides a nominal treated water production rate of 6000 litres per hour. This gives the facility a defined treatment capability that can be managed according to its operational requirement.

The project also resulted in an integrated treatment arrangement in which the pre-treatment, pumping, RO membrane and supporting components work together. This improves the structure of the water treatment process by providing a clear path from incoming water to treated water.

Another important result is the completion of the installation and commissioning process. The system was checked after installation so that the equipment and connections could be evaluated before regular use.

No detailed laboratory results, recovery figures, TDS reduction data or operating cost figures were provided for this project. For that reason, the performance discussion does not include unverified percentages or numerical claims.

The project can therefore be evaluated on the confirmed outcomes: successful installation of the 6000 LPH RO plant, completion of the treatment system connections and commissioning of the plant for operation.

These results reflect the practical value of working with an experienced Commercial RO Plant Manufacturer in Noida that can manage the project from equipment installation through system commissioning.

Confirmed Outcome Status
Installation of 6000 LPH RO Plant Completed
Treatment System Connections (piping, electrical) Completed
Plant Commissioning Completed
Laboratory/TDS/Recovery Data Not provided — not included in this case study


Customer Feedback or Testimonial

Customer feedback is useful because it provides an external view of the completed installation. It can show whether the supplied system met the client’s expectations and whether the installation process was handled satisfactorily.

The successful installation and commissioning of the 6000 LPH RO plant at the Sunwoda facility in Noida was done by Netsol Water. The defined installation scope was carried out and the treatment system was brought into operation.

Read some interesting information for the Industrial RO Plant Manufacturer in Delhi

Conclusion

The successful installation of the 6000 LPH RO plant at Sunwoda in Noida demonstrates the importance of matching treatment capacity, equipment selection and installation practices with the actual needs of a facility. The project created a dedicated RO treatment plant with a defined capacity of 6000 litres per hour and a structured process for converting incoming water into treated water.

The project also shows why proper execution matters at every stage. Pre-treatment supports the membrane system. Pumps maintain the required water movement and pressure. The RO membranes carry out the main purification process. Piping, electrical connections and controls bring these components together into one operating system. Testing and commissioning then provide the final check before regular operation.

For businesses and industrial facilities looking for a suitable RO solution, selecting an experienced Commercial RO Plant Manufacturer in Noida can simplify the process from system selection and equipment supply to installation and commissioning. A properly designed plant can provide a practical treatment solution while keeping capacity and operating requirements aligned with the facility’s needs.

Netsol Water provides RO plant solutions for commercial and industrial water treatment requirements. Businesses that need a new RO plant or want to discuss a suitable treatment capacity can contact Netsol Water for project consultation and technical guidance based on their water source, required capacity and application.

Contact Netsol Water

Contact Details
Phone +91-9650608473
Email enquiry@netsolwater.com


Successfully-Installed-3000-LPH-RO-Plant-at-SMC-Corporation-Noida.webp

August 25, 2026by Netsol Water

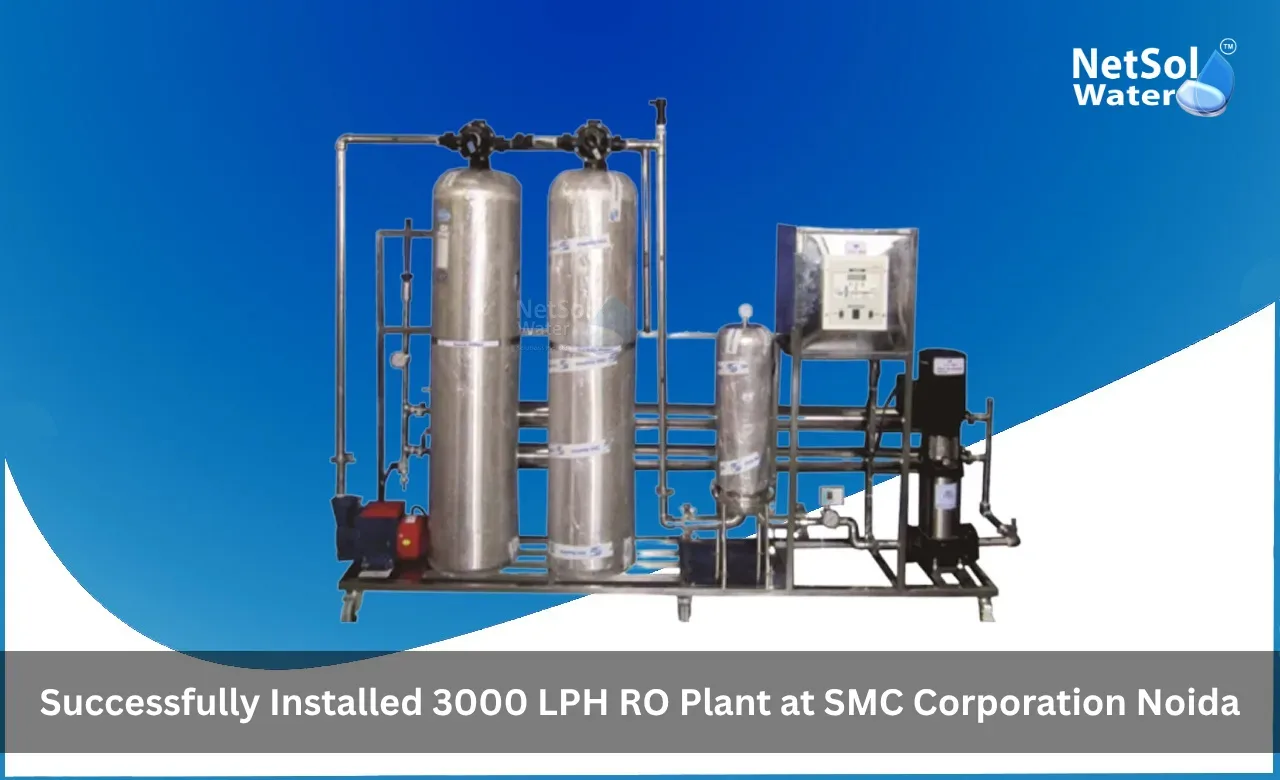
Successfully Installed 3000 LPH RO Plant at SMC Corporation Noida

Reliable water treatment plays an important role in facilities where a regular supply of suitable-quality water is needed for day-to-day operations. For SMC Corporation in Noida, the requirement was to install a commercial RO plant that could provide treated water at a suitable operating capacity. To meet this need, Netsol Water completed the installation of a 3000 LPH RO plant at the client’s Noida facility.

Netsol Water is a leading water and wastewater treatment company in the Noida region. The company manufactures commercial and industrial RO plants in different capacities and provides design, installation and commissioning support for water treatment projects.

The project focused on providing SMC Corporation with an RO-based water treatment solution that could support its operational water requirements. A properly selected RO system helps reduce dissolved impurities from feed water and produces treated water for suitable applications. The 3000 LPH capacity also provided a defined treatment rate for the facility. This project shows how a Commercial RO Plant Manufacturer in Noida can support a commercial facility through planned system selection, installation and commissioning.

Project Overview

A commercial water treatment project requires more than the supply of an RO machine. The treatment capacity must match the intended demand and the system must fit the available facility and operating conditions. The installation at SMC Corporation was planned around these basic requirements.

The project involved the installation of a 3000 LPH Reverse Osmosis plant at SMC Corporation in Noida. The main objective was to provide a dedicated water treatment system that could process incoming water and produce treated water through the RO process. The selected capacity gave the facility a treatment output of up to 3,000 litres per hour under the rated operating conditions of the plant.

The scope of the project centred on the installation of the RO treatment plant and the activities required to bring the plant into operation. This included positioning the treatment equipment, completing the required connections and carrying out testing before regular operation. Since water treatment performance depends on correct installation as well as the treatment process itself, the project required attention to both equipment setup and commissioning.

Netsol Water‘s commercial RO systems are offered across a wide range of capacities. Its published commercial RO range includes systems from small commercial units to much larger installations. The 3000 LPH plant selected for this project therefore formed part of a broader commercial water treatment capability.

Client Details

SMC Corporation is the Indian subsidiary of SMC Corporation Japan and operates in the field of pneumatic and automation technology. SMC India was incorporated in 1995 and has its head office at A-4, Sector-88, Noida. The company operates manufacturing facilities in India and maintains a network that supports its industrial customers.

The Noida facility provides an industrial setting where a dependable utility water supply can support normal facility operations. In such an environment, water quality must be considered when selecting a treatment system because untreated water may contain dissolved salts, suspended matter or other impurities that make it unsuitable for a specific application.

The project information available for this installation does not provide detailed information about SMC Corporation‘s exact end use of the RO water. Therefore, it would not be correct to assign a specific application such as drinking, process water, boiler feed or cleaning water without supporting documentation. The confirmed requirement was the installation of a 3000 LPH RO plant at the client’s Noida facility.

With the client requirement established, the location became an important part of the project planning and execution.

Project Location

The project was carried out at SMC Corporation, A-4, Sector-88, Noida. SMC Corporation‘s official corporate information identifies this address as its Noida head office and factory location.

Noida is a major industrial and commercial area within the Delhi-NCR region. An industrial facility in this setting may have continuous utility requirements and limited tolerance for interruptions in essential services. Water treatment equipment must therefore be installed in a way that suits the available site and allows the system to operate as intended.

The project location also offered a practical advantage for Netsol Water because the company operates in Noida and the wider Delhi-NCR region. Netsol Water is a water and wastewater treatment company and provides commercial RO solutions for customers in the region.

With the site and facility requirements understood, the next consideration was choosing a treatment capacity that matched the intended demand.

Plant Capacity

Plant capacity determines how much water a treatment system can process within a given period. Selecting an appropriate capacity helps ensure that the system can support the required water demand without being significantly undersized or unnecessarily oversized.

For this project, Netsol Water installed a 3000 LPH RO plant, where LPH means litres per hour. At its rated capacity, the system is designed to treat up to 3,000 litres of feed water per hour. If operated continuously at its rated flow, this corresponds to a theoretical gross treatment throughput of 72,000 litres over 24 hours. Actual daily production can vary according to operating hours, feed-water conditions, recovery, membrane performance, cleaning cycles and other plant conditions.

Parameter Value
Rated Capacity 3000 LPH (Litres Per Hour)
Theoretical Gross Throughput (24 hrs continuous) 72,000 litres


The 3000 LPH specification provided SMC Corporation with a defined treatment capacity for its facility. It also established a clear operating benchmark for the installed equipment.

Netsol Water‘s published commercial RO range includes capacities from 50 LPH to 10,000 LPH and beyond for larger requirements, showing that commercial systems can be selected according to the expected water demand.

Capacity alone, however, does not determine treatment performance. The quality of the incoming water and the selected treatment technology also influence the design.

Treatment Technology

Reverse Osmosis is widely used when a water treatment system needs to reduce dissolved salts and other impurities from water. The process uses pressure to push feed water through a semi-permeable membrane. Water passes through the membrane while a significant portion of dissolved substances and other contaminants remains in the reject stream.

For the SMC Corporation project, the selected technology was Reverse Osmosis. The basic purpose of the RO stage was to convert incoming feed water into treated water through membrane-based separation.

1. Reverse Osmosis Working Principle

The RO process starts when feed water reaches the membrane under pressure. The pressure must be sufficient to overcome the natural osmotic pressure of the feed water. As the pressurised water moves across the membrane surface, water molecules pass through the membrane while many dissolved salts and other unwanted substances are retained.

This process makes RO different from simple filtration. A conventional filter mainly removes suspended particles based on their physical size. RO also addresses many dissolved impurities that cannot be removed through ordinary mechanical filtration.

Netsol Water explains that its RO plants use membrane treatment to reduce impurities from incoming water and produce purified water.

2. Importance of Pretreatment

RO membranes need suitable feed-water conditions to maintain performance. Suspended particles, excess turbidity, chlorine and other substances can affect membrane life and operating efficiency. For this reason, commercial RO plants commonly use suitable pretreatment before water reaches the RO membrane.

The exact pretreatment arrangement installed at SMC Corporation has not been provided in the available project information. Therefore, specific filter models, dosing arrangements, membrane models or chemical treatment values cannot be confirmed for this project. The treatment discussion remains focused on the confirmed RO technology and the normal role of pretreatment in protecting the membrane.

Influent Characteristics

Understanding the incoming water quality is an important part of RO system planning. Water sources can contain different levels of dissolved solids, hardness, turbidity, iron, organic matter and microbial content. The treatment design should consider these characteristics before the equipment is selected and commissioned.

For this project, no detailed feed-water laboratory report or exact influent values have been provided. There are therefore no confirmed project-specific figures for TDS, hardness, turbidity, iron, pH or microbial load that can be reported.

The absence of these figures does not change the purpose of the installed RO system. Rather, it means that the case study should not assign numerical values that have not been documented. In a normal RO design process, these parameters help determine pretreatment requirements, membrane selection, operating pressure and expected performance.

The incoming water first needs suitable conditioning so that it can enter the membrane stage under appropriate conditions. From there, the treatment process can continue toward the production of treated water.

Treatment Process

A successful RO installation depends on a properly arranged treatment sequence. Each stage supports the next by preparing the water for the following treatment step. This reduces the load placed on the RO membrane and supports stable operation.

1. Raw Water Entry and Pretreatment

The treatment journey begins when raw or feed water enters the treatment system. Before the water reaches the RO membrane, the system normally prepares the feed through pretreatment. This stage can remove suspended matter and reduce substances that may create problems for the membrane.

The exact pretreatment equipment used at SMC Corporation has not been specified in the project details. However, the principle remains the same. Water must reach the membrane in a condition suitable for RO operation.

2. Pressure and Membrane Treatment

After the necessary pretreatment, feed water moves toward the high-pressure section of the RO system. The pump provides the pressure needed to drive water through the semi-permeable RO membrane.

The membrane separates the incoming stream into two paths. The permeate contains the water that passes through the membrane. The reject stream carries a higher concentration of retained dissolved substances and does not form part of the treated-water output.

3. Treated Water Collection

The permeate then moves toward the treated-water collection or subsequent use point. The final arrangement depends on the site’s piping and storage configuration.

This sequence provides a clear connection between the raw water source and the treated-water output. Proper operation of each stage helps the plant maintain the intended treatment function.

Major Equipment

Proper equipment selection supports consistent plant operation. An RO plant needs several components to move water, condition the feed, apply pressure and carry out membrane separation.

For this project, the confirmed major treatment equipment is the 3000 LPH RO plant itself. The plant includes the RO treatment assembly required to process feed water at its rated capacity. Netsol Water‘s commercial RO systems commonly use components such as membranes, high-pressure pumps, pressure vessels, control panels and dosing pumps, depending on the plant configuration.

Equipment Function
RO Membrane Assembly Performs the main separation process. It allows water to pass through under pressure while retaining a substantial portion of dissolved impurities.
High-Pressure Pump Provides the pressure needed for membrane separation. Its operation is directly linked to maintaining the pressure conditions required by the RO process.
Control Panel Helps the operator manage the plant and monitor its operating sequence. The exact control philosophy and automation level installed at SMC Corporation have not been provided.
Pretreatment and Supporting Components Protects the RO membrane and helps prepare the feed water. The specific filter vessels, dosing units, valves and instruments used for this project are not documented in the information available.


As a result, no unverified equipment list is presented as a project fact.

Installation Process

Plant installation requires careful planning because the equipment must fit the site while maintaining proper connections between the different treatment stages. The work should also allow operators to access the system for normal inspection and maintenance.

The installation at SMC Corporation involved placing the 3000 LPH RO system at the client’s Noida facility and preparing it for operation. The equipment had to be positioned appropriately before the required piping, water connections and electrical connections could be completed.

Once the equipment position was established, the installation team could connect the treatment sections so that water could move through the intended process. Electrical and control connections were also required to prepare the plant for testing.

The final stage of installation involved checking the physical setup and confirming that the system was ready for commissioning. This step was important because a treatment plant must be mechanically and electrically prepared before performance testing can begin.

Plant Commissioning

Commissioning confirms whether an installed treatment system is ready for regular operation. It provides an opportunity to check the plant under operating conditions and identify installation issues before the system enters normal service.

After installation, the RO plant was prepared for testing and commissioning. The commissioning process involved checking the operating sequence and confirming that the equipment could function as intended. Water movement through the treatment system had to be verified along with the operation of the principal components.

The commissioning stage also provided an opportunity to observe the plant’s treatment behaviour at its intended operating capacity. A proper commissioning process helps confirm that the system is connected correctly and that the plant can move from installation into routine operation.

The available project information does not include detailed commissioning readings such as recovery percentage, feed pressure, permeate TDS or hourly production records. These figures have therefore not been added to the project results.

Treated Water Reuse

Treating water becomes more useful when the resulting water can support an appropriate application within the facility. RO-treated water can be directed to a designated use point depending on the quality requirement and the site’s internal water management arrangement.

For the SMC Corporation project, the confirmed scope establishes the installation of a 3000 LPH RO plant but does not specify the exact final use of the treated water. It would therefore be inappropriate to state that the water was used for a particular process without supporting information.

The practical value of the system lies in creating a dedicated source of treated water for the client’s identified requirement. When used appropriately, such a system can help provide greater control over the quality of water supplied to the intended application.

Results and Performance

Project results provide a practical measure of whether the installed system met its intended purpose. In this installation, the major confirmed outcome was the successful installation and commissioning of a 3000 LPH RO plant at SMC Corporation‘s Noida facility.

The system established a dedicated RO-based treatment capacity of 3,000 litres per hour. This provided the client with a defined water treatment system rather than depending only on untreated incoming water for the relevant requirement.

The treatment technology also created a process for reducing dissolved impurities through membrane separation. Netsol Water identifies RO as one of its core commercial water treatment solutions and offers commercial systems in different capacities for varied applications.

No project-specific laboratory figures, before-and-after water quality results or long-term operating data were provided. The performance discussion is therefore limited to the confirmed installation, capacity and successful movement of the plant into operation. This approach keeps the project record factual and avoids presenting unverified performance claims.

Customer Feedback/Testimonial

Customer feedback helps demonstrate how a completed project performs from the client’s perspective. It can also provide useful information about installation quality, plant operation and overall project satisfaction. The 3000 LPH RO plant was successfully installed at the specified Noida facility and taken through the required commissioning stage.

Read some interesting information for the Industrial RO Plant Manufacturer in Gurgaon

Call to Action

Netsol Water‘s completed installation at SMC Corporation shows how a properly selected RO system can provide a dedicated water treatment solution for a commercial facility. The project combined a defined treatment capacity with membrane-based purification and onsite installation support. Netsol Water operates from the Noida region and provides commercial RO systems in a range of capacities for different water treatment requirements.

Businesses looking for a Commercial RO Plant Manufacturer in Noida can consult Netsol Water to discuss their feed-water source, treatment capacity and application requirements. A suitable system should always be selected after understanding the site’s water quality and expected demand rather than simply choosing a standard capacity.

Netsol Water is the leading commercial RO plant manufacturer, supplier and exporter based in Noida, according to its published company information, and provides commercial RO systems across a broad capacity range.

For organisations planning a new RO installation or upgrading an existing water treatment system, professional consultation can help define the right treatment approach. Contact Netsol Water to discuss your requirement and request a suitable commercial RO plant solution for your facility.

Contact Netsol Water at:

Contact Details
Phone +91-9650608473
Email enquiry@netsolwater.com


Successfully-Installed-2000-LPH-RO-Plant-at-Godrej-Zenith-Gurgaon.webp

August 18, 2026by Netsol Water

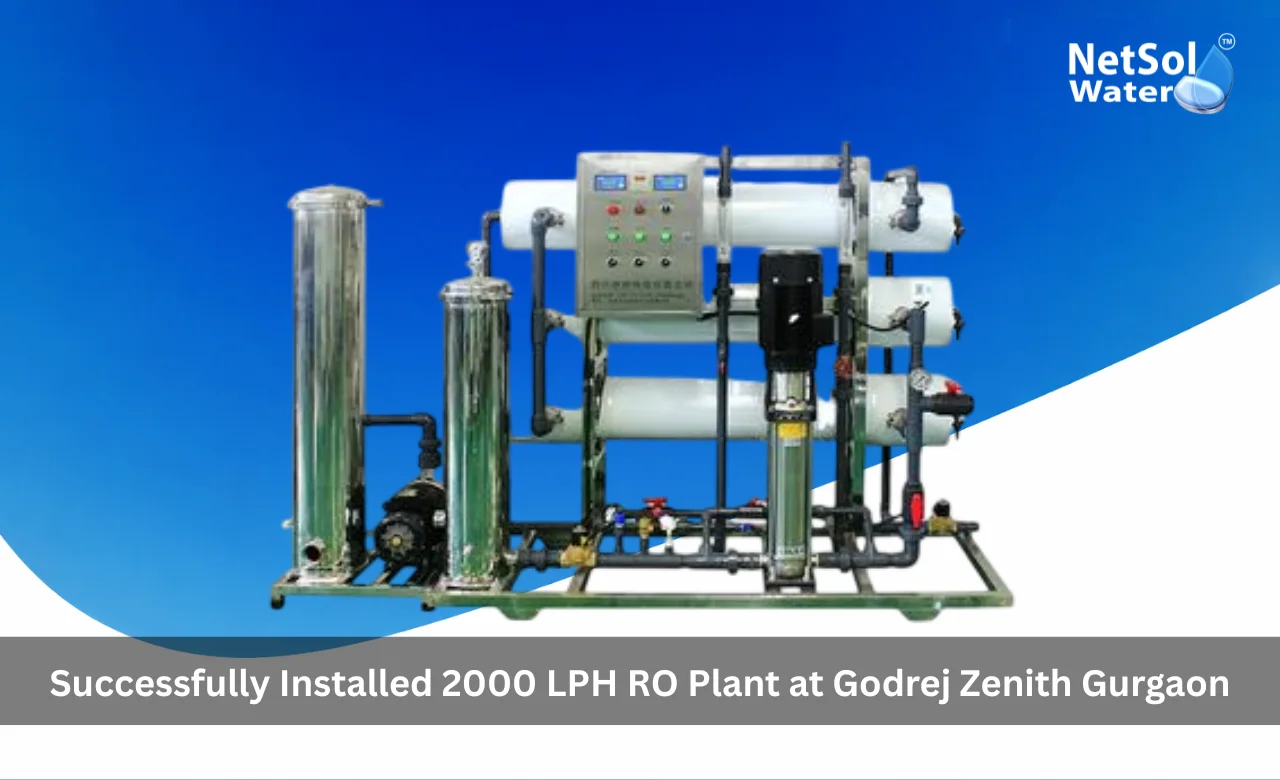
Successfully Installed 2000 LPH RO Plant at Godrej Zenith Gurgaon

The provision of good and properly treated water is a key requirement for today’s residential and commercial developments. Water quality can vary due to raw-water quality and/or dissolved solids, hardness, suspended matter, and other contaminants, which can have an impact on water usability, plumbing systems, equipment performance, and overall facility operations. In order to overcome these challenges, a suitable water-treatment plant should incorporate an efficient pretreatment process as well as a robust membrane filtration process.

A 2000 LPH Reverse Osmosis Plant was installed at Godrej Zenith, Gurgaon successfully, to ensure a reliable supply of treated water while sustaining the efficient running of the plant and the consistent quality of the water produced.

The project comprised the following activities: Water-treatment requirement assessment, selection of appropriate treatment technology, fabrication of the plant, transportation, installation, testing, commissioning and performance verification. The system was designed based on the reverse osmosis technology, which is protected by proper pretreatment stages and has high treatment efficiency.

This project showcases our capabilities as a leading Commercial RO Plant Manufacturer in Gurgaon and delivers customized RO solutions to residential complexes, commercial buildings, institutions, industries, hotels, hospitals, corporate buildings, and more, that demand reliable water purification.

Project Overview

The project entailed the supply, installation, testing and commissioning of a 2000 litres per hour (LPH) commercial RO plant for Godrej Zenith, Gurgaon.

The main goal was to implement a well-designed water-treatment method that could remove dissolved contaminants and enhance the water quality of the raw water. The performance of an RO membrane is highly dependent on the quality of water fed to the membrane system, so the project was planned as an integrated treatment system rather than just putting up an RO membrane unit.

All of these features – pretreatment, filtration, high pressure pumping, reverse osmosis membrane separation, instrumentation, flow control mechanisms, and collected treated water – constituted the full treatment arrangement.

The following were given special consideration:

  • Consistent treated-water production
  • Decrease in dissolved salts and undesirable impurities
  • Protection of RO membranes
  • Operational reliability
  • Ease of maintenance
  • Use of available space is maximized.
  • Maintains a stable system pressure and flow.
  • Convenient operator access
  • The ability to install in a safe and systematic manner
  • Long-term plant performance

The 2000 LPH capacity is based on the treated water demand of the site and anticipated operating conditions.

Its successful installation enables Godrej Zenith to have a water-treatment system that is planned to give its customers treated water of 2,000 litres per hour for the above stated operating conditions and parameters.

Client Details

Project Detail Information
Client/Project Godrej Zenith
Water Resources Water Resources Management, Water Treatment, Water Quality Management
Type of RO plant Commercial.
Rated Capacity 2000 LPH
Location Gurgaon, Haryana


Godrej Zenith needed a water treatment system that could supply a reliable amount of treated water, with consistent quality.

When choosing a RO for projects like this, the right choice of RO capacity is just part of the equation. Other factors to consider include water chemistry, operating hours, recovery expectations, pressure requirements, feed-water characteristics, pretreatment requirements, equipment accessibility and future maintenance requirements.

These requirements were analyzed by our technical team as part of the treatment configuration development.

This led to the development of a tailor-made 2000 LPH commercial RO unit, which is optimized for a combination of water quality enhancement, plant efficiency, protection of RO membranes and ease of maintenance.

Project Location – Godrej Zenith, Gurgaon

The RO plant was commissioned in Godrej Zenith at Gurgaon, Haryana.

Gurugram, popularly known as Gurgaon, has undergone a large scale residential, corporate, institutional and commercial growth. The region’s large properties need reliable water-management systems to keep them running.

Ground water and other sources of water may contain various amounts of dissolved minerals, hardness, suspended materials, and other contaminants. Other sources of water, seasonal changes, storage conditions, and area water supply systems can also impact water quality.

Therefore, plant capacity is not the only criterion to consider when choosing a water-treatment system. Water quality and water quantity must both be taken into account for proper treatment design.

Being one of the leading Commercial RO Plant Manufacturer in Gurgaon, we do not use a one size fits all approach for all projects, but customize the design of RO systems for each site.

Plant Capacity – 2000 LPH

The treated water production capacity of the RO system installed is:

2000 Litres Per Hour (LPH)

Plant size typically means that it is designed to give a purified water output of around 2,000 litres an hour under the plant design conditions.

The chosen capacity offers an ideal combination of:

  • Required treated-water demand
  • Available feed-water quantity
  • Operating duration
  • RO recovery
  • Membrane loading
  • Pump capacity
  • Storage requirement
  • Space availability
  • Expected future usage

When a RO plant is installed correctly, it does not result in the problems caused by under sizing or oversizing the plant.

An undersized system can be running all the time and could come up short of meeting peak demand. A system that is too large, however, will waste money on capital expense, equipment size and power use.

The configuration of 2000 LPH was therefore chosen, to provide an effective solution for the water-treatment requirement of the site, yet maintain the ability to operate and maintain the system.

Treatment Technology

This project employs the main treatment technology of RO.

Reverse osmosis is a pressure driven membrane-separation process, which is widely used for removal of dissolved salts and other undesirable component from water.

In RO water treatment, feed water is pumped at high pressure through semi-permeable membranes, which are treated beforehand. As the water molecules cross the membrane, they leave behind a high concentration of salts and other rejected components as the concentrate stream.

But an effective commercial RO plant is more than just an RO membrane.

The treatment system installed at Godrej Zenith consists of various stages to ensure that the RO membranes receive the feed water suitably treated.

The overall technology is comprised of:

  • Feed-water handling
  • Pressure boosting
  • Multimedia/sand filtration
  • Activated carbon filters
  • Micron cartridge filtration
  • Chemical conditioning – as appropriate.
  • High-pressure pumping
  • Reverse Osmosis Membrane Separation
  • Product-water collection
  • Monitoring the flow and pressure.
  • Influent Characteristics

The source or feed water had impurities that required further treatment prior to use.

In the context of local source and supply conditions, raw water from Gurgaon may pose treatment issues like:

  • Dissolved salts or elevated TDS
  • Hardness
  • Fine suspended matter
  • Turbidity
  • Calcium and magnesium compounds
  • Chlorides and other dissolved ionic constituents
  • Colour or odour-causing substances
  • Organic impurities
  • Fine particles capable of fouling RO membranes

Wherever possible, the design of any RO system should be based on a water analysis.

The treatment train is designed for this installation to allow the removal of the contaminants from the water before it reaches the membranes and to create water with a much better quality.

Direct feeding of untreated water into RO membranes can lead to:

  • Membrane scaling
  • Fouling
  • Reduced permeate flow
  • Increased pressure requirement
  • Reduced salt rejection
  • More frequent membrane cleaning.
  • Shortened membrane life

The influent water conditions thus influenced the type and configuration of the pretreatment equipment.

Treatment Process

Godrej Zenith Gurgaon installed 2000 LPH commercial RO plant which has a systematic treatment sequence.

Step 1: Feed Water Collection

Water that comes from the designated raw water source or water storage facility to the treatment system.

To maintain the continuous operation of the RO plant it is essential to have enough feed-water.

Step 2: Feed/Raw Water Pumping

The pretreatment units require a certain flow and pressure, which is achieved using a feed pump.

Feed pressure stability is crucial because fluctuations in feed pressure can impact the filtration process downstream and RO performance.

Step 3: Multimedia/Sand Filtration

Water for the feed is passed through a filtration unit which removes:

  • Suspended particles
  • Sediment
  • Silt
  • Turbidity
  • Coarser particulate matter

These contaminants are removed to ensure protection of subsequent treatment stages.

Step 4: Activated Carbon Filtration

Activated carbon filtering to remove compounds that cause an undesirable colour, odour and some organic contaminants is required by the feed-water characteristics in most cases.

It can also serve as a protection for downstream membranes where there are oxidizing compounds to be controlled.

Step 5: Chemical Conditioning

Appropriate dosing can be added to prevent scaling and optimize membrane performance, depending on the chemistry of the feed water.

Dissolved minerals can be deposited on the surface of the membrane, causing scale formation, which is a critical issue in RO systems.

Chemical conditioning minimizes precipitation and can increase the operating life of the membrane.

Step 6: Micron Cartridge Filtration.

Water is filtered through small cartridge filters prior to entering the high pressure RO section.

This filtration stage serves as an extra layer of protection by getting rid of fine particles that might have gotten through the preceding filtration stages.

Step 7: High-Pressure Pumping

The feed water is pumped up to the required pressure for membrane separation by a high-pressure pump.

The pump is one of the most significant parts of the commercial RO plant as the required pressure should be sufficient to overcome the osmotic pressure for the desired product-water production.

Step 8: Reverse Osmosis Membrane Treatment

Feed water is pressurized and fed into the RO membrane housings.

The membrane system splits the feed stream into:

Permeate/Product Water: Water that goes through the RO membrane and has much lower concentration of dissolved impurities.

Rejected/Concentrated Water: Salt and impurities rejected by the membranes, while the water is concentrated.

Step 9: Product water collection tank

The purified permeate is fed to the treated-water storage facility, from where it is used.

Step 10: Monitor and control

Essential operating parameters can be monitored via pressure gauges, flow meters, valves and other instrumentation.

This allows the detection of plant performance changes before they become serious maintenance problems.

Major Equipment for 2000 LPH RO Plant.

The entire plant design includes equipment chosen based on the required treatment conditions, operating pressure and flow.

Major Equipment Purpose / Description
Raw Water/Feed Pump Provides sufficient water flow and pressure to the pretreatment section.
Multimedia/Sand Filter Minimizes suspended matter, silt, sediment and turbidity of incoming water.
Activated Carbon Filter Removes undesirable organics, odours, colour and other contaminants.
Chemical Dosing System Used for water conditioning and/or membrane-scale control based upon the characteristics of the raw water.
Micron Cartridge Filter Fine filtration directly in front of the RO section.
High-Pressure Pump Produces the operating pressure for efficient reverse osmosis.
RO Membrane Housings Hold the reverse osmosis membrane elements and be able to resist the operating pressure of the system.
RO Membranes Carry out the main dissolved-solids separation operation.
Flow Meters Allow product-water and reject-water flow to be observed by operators.
Pressure Gauges Assist in measuring pressure at significant treatment points and detect abnormal operating conditions.
Control Panel Central Controls for electricity and helps in safe operation of pumps and other equipment.

IPV is the process of connecting pipes and valves together.

Regulates and regulates water flow between treatment processes.

All major components have been installed to ensure ease of operation and future maintenance.

Installation Process

The installation of a commercial RO plant involves appropriate planning because even the well-designed RO plant can perform poorly if there is improper piping, electrical connection, foundation alignment, foundation preparation, or improper commissioning.

The installation of Godrej Zenith project was a systematic process.

1. Site Assessment

Prior to the final position of the equipment the available installation space and utility arrangements were evaluated.

Considerations included:

  • Available floor area
  • Water inlet location
  • Drainage arrangement
  • Electrical supply
  • Treated-water outlet
  • Operator movement
  • Maintenance clearance
  • Equipment accessibility
  • Equipment Positioning

Key treatment components were placed in a logical sequence that started at the raw water intake and ended at the treated water discharge.

Equipment spacing was observed to allow for routine inspection and servicing as much as possible.

2. Piping Connections

The piping between the feed-water section, filters, dosing arrangement, cartridge filtration system, high-pressure pump, membrane system, reject line and permeate outlet was installed.

3. Electrical Connections

Electrical connections were made to pumps and control systems based on the plant operating criteria.

4. Instrument Installation

Monitoring equipment such as pressure, flow, valves, etc. placed at appropriate locations.

5. Leakage and Connection Checks

Inspection for leaks and alignment of piping joints, membrane housings, valves and connections were performed prior to regular operation.

Plant Commissioning

One of the most critical phases of any water-treatment system installation is commissioning.

It is not just about starting the RO plant, but it is about checking whether all the treatment stages are working properly or not and whether the whole system is working in an integrated manner.

The commissioning of the 2000 LPH RO plant at Godrej Zenith Gurgaon was a commissioning exercise that involved the following:

  • Inspection of installed equipment
  • Verification of piping connections
  • Checking electrical connections
  • Confirmation of valve positions
  • Filter flushing
  • Cartridge-filter inspection
  • Pump operation checks
  • High-pressure section inspection
  • Membrane-system startup
  • Pressure adjustment
  • Flow-rate adjustment
  • Permeate-flow monitoring
  • Reject-flow monitoring
  • Product-water quality checking
  • System leakage inspection
  • Overall operational testing

It was initially under a controlled operation until the pressure and flow of the system was stabilized.

The RO system was then tested to verify the production of the treated water is in line with the rated capacity and operating conditions of the plant.

The plant was successfully tested and put into operation for regular use.

The one of the biggest benefit of an onsite commercial RO plant is that you can generate treated water as per the operational requirements of the property.

Some potential applications of treated RO water are:

  • Domestic water requirements
  • Cleaning applications
  • Utility requirements
  • Process-water applications
  • Food processing equipment that uses low TDS water

We also accept other alternative uses for property, as outlined below:

Treatment levels should always match the use(s) of the treated water and the regulatory/operational requirements.

The water quality of RO reject water may also be considered for potential non-potable reuse opportunities, when water quality, infrastructure, and local needs allow.

Applications may be selected cleaning, flushing or other non-critical uses, following suitability determinations.

This re-use can help to achieve more responsible water management and minimise unnecessary water waste.


Results and Performance

Godrej Zenith 2000 LPH RO plant was successfully installed and commissioned and it was found to be operating very stable with the designed parameters.

The main outcomes of the project were:

1. Consistent Treated-Water Production

Under the design operating conditions, the system was designed to produce about 2000 litres per hour of treated water.

A substantial decrease in the concentration of dissolved impurities.

The dissolved salts and other membrane-rejectable components of the feed water were significantly decreased through the use of the RO membrane stage.

2. Improved Water Quality

The treated water was significantly better than the untreated feed water and is suitable to the intended site use.

3. Stable Operating Pressure

The high pressure system was tuned during the commissioning process to obtain stable operation of the membrane.

4. Effective Pretreatment

The particulate and contaminant load entering the RO membrane section is reduced by the use of the pretreatment units.

5. Membrane Protection

The system minimizes the chances of fouling and scaling of the membranes by using the right pretreatment and chemical conditioning.

6. Reliable System Operation

Dependable day to day operation relies on correct size, systematic piping, instrumentation and commissioning.

7. Maintenance-Friendly Layout

The equipment layout enables filters, valves, gauges, pumps and membrane housings to be easily accessed for routine inspection and maintenance.

This successful installation proves that the proper combination of selection, pretreatment and the professional commissioning is of key importance.

Customer Feedback / Testimonial

Godrej Zenith’s commissioned 2000LPH RO plant is a testament to the client’s need for a reliable and professionally set up commercial water treatment system.

Client testimonial:

*The LPH RO plant was installed at our site successfully and the system is operating with a regular rate of treated water production. Technical team provided proper support during installation, testing and commissioning.*

The successful completion of this project further highlights our commitment for designing, fabricating, installing, commissioning, and after-sales technical support of not only RO equipment, but an entire water treatment solution.

Why opt for us as your Commercial Ro Plant Manufacturer in Gurgaon?

Capacity and price are not the only two criteria that should be used to select an RO plant.

The lifespan of a commercial RO system is determined by a number of factors such as:

  • Raw-water analysis
  • Appropriate plant sizing
  • Pretreatment design
  • Membrane selection
  • Pump sizing
  • Operating pressure
  • Recovery percentage
  • Instrumentation
  • Installation quality
  • Preventive maintenance
  • Technical support, availability of support.

We are a Commercial RO Plant Manufacturer in Gurgaon and offer plants according to site specific needs.

RO solutions that are commercial and industrial, can be made to fit various capacities and applications such as:

  • Residential societies
  • Commercial complexes
  • Corporate offices
  • Hotels
  • Hospitals
  • Educational institutions
  • Restaurants
  • Manufacturing facilities
  • Food-processing units
  • Industrial plants
  • Construction projects
  • Institutional buildings
  • Warehouses
  • Shopping complexes

RO plants can be combined with other technologies like multimedia filtration, activated carbon filtration, softening, antiscalant dosing, UV treatment, ozone treatment, ultrafiltration and other water-treatment technologies, depending on the water characteristics and application.

Project Summary

Details of the project: Installation of Commercial RO Plant.

Project Detail Details
Client Godrej Zenith
Location Gurgaon, Haryana
Plant Capacity 2000 LPH
Primary Technology Reverse osmosis.
Pretreatment Filtration and water conditioning according to the needs of the feed water.
Treatment The use of treated water for plant needs.
Project Scope Design, supply, installation, test and commissioning.
Install and Commission Status Successfully Installed and Commissioned;

The project illustrates the potential of a well-designed RO plant to be a reliable solution for consistent treated water quality for commercial and residential developments.

Every stage of the treatment requirement to the final commissioning was completed with a focus on operational reliability, membrane protection, efficiency and maintainability over time.

Call to Action

In cases where the issues are high TDS, hardness, dissolved salt, water quality, or intermittent availability of treated water in residential societies, commercial buildings, hotels, hospitals, institutions, offices, restaurants or industrial facilities, the right commercial RO system will be able to help.

We produce and install the customized RO plant as per your requirement:

  • Raw-water quality
  • Required treated-water capacity
  • Daily water consumption
  • Available installation space
  • Operating conditions
  • Intended application
  • Budget
  • Automation requirements

The system can be designed to meet the specific requirements of the project, whether for a 5000 LPH or any other higher capacity RO plant, or a 5000 LPH, 3000 LPH, 2000 LPH, 1000 LPH or 500 LPH RO plant.

Read some interesting information for the Industrial RO Plant Manufacturer in Faridabad

Need a Commercial RO Plant in Gurgaon?

Contact us for:

  • Site Assessment
  • Water Quality Evaluation
  • RO Plant Design and Capacity Selection
  • Commercial RO Plant Manufacturing
  • Installation and Commissioning
  • RO Membrane Replacement
  • Plant Maintenance and AMC Services
  • Existing RO Plant Upgradation
  • Technical Support and Troubleshooting

If you are searching for a reliable Commercial RO Plant Manufacturer in Gurgaon, contact our water-treatment specialists to discuss your requirement and receive a customized solution.

Get in touch today for a commercial RO plant consultation, site visit, and customized quotation.

Contact Netsol Water at:

Phone: +91-9650608473

Email: [enquiry@netsolwater.com](mailto\:enquiry@netsolwater.com)


What-are-the-Applications-of-Commercial-Water-Softeners-3.webp

August 17, 2026by Netsol Water

Successfully Installed 1000 LPH Commercial RO Plant at Skylark, Gurgaon

Commercial offices, infrastructure companies, manufacturing facilities, institutions and hotels need reliable access to appropriately treated water. The incoming water may have excessive dissolved salts, hardness, suspended particles or other undesirable constituents; a properly designed commercial RO system can help maintain the necessary treated-water quality. We installed and commissioned a 1000 LPH Commercial RO Plant at Skylark, Gurgaon for its production of about 1000 litres of RO treated water per hour with the specified operating conditions. The project embodies our work as a reputed Commercial RO Plant Manufacturer in Gurgaon.

Project Overview

The main goal of this project was to set up a commercial water treatment system which would produce about 1000 LPH of RO treated water at Skylark‘s Gurgaon site.

The water-treatment systems used in commercial facilities are different to those in small domestic RO units. The equipment should be able to process greater flow rates, operate longer hours and process different feed-water characteristics, and be easy to operate and maintain.

The treatment system was designed for a 1000 LPH commercial RO plant with appropriate pre-treatment stages for this project. The goal was to not only install RO membranes, but to design an entire treatment sequence that would safeguard the membranes and ensure consistent output.

The overall work involved in the installation comprised assessment of the area, equipment planning, plant fabrication and assembly, plant transportation, positioning of the plant equipment, plant plumbing connections, electrical connections, plant pretreatment setup, plant RO membrane installation, testing, plant flushing, plant trial operation and final plant commissioning.

The final product was a water-treatment system that satisfied the commercial need of Skylark with a convenient access path for future inspection and maintenance of the major components of the system.

Client Details

The project was for Skylark, Gurgaon as a client. It has EPC, mining, toll collection and highway maintenance as its major business segments.

The company’s operations feature large-scale infrastructure activities, and a significant employee base. Such an organisation needs reliable utility services capable of supporting the normal running of business.

One of these utilities is water-treatment infrastructure. An appropriate size commercial RO plant can process water at a central location, and the purified water can be stored for use as required at the facility, rather than using small purification units.

Thus the 1000LPH Commercial RO Plant was selected which proved to be a good solution for the site with a relatively small footprint for the system.

Project Location

The RO plant installed at Skylark, Gurgaon, Haryana. Their address in Gurgaon is: 267, Udyog Vihar, Phase IV, Gurgaon – 122015, Haryana, India.

One of the prominent commercial and industrial hubs of Gurgaon, Udyog Vihar is home to offices, manufacturing units, warehouses and corporate establishments in the various stages.

Water supply to commercial establishments in Gurgaon may be from various sources and the water quality may vary depending on the source and local conditions. Therefore, it is best to choose the water-treatment equipment based on the water’s feed-water quality, not just on the basis of its LPH rating.

Therefore, as a Commercial RO Plant Manufacturer in Gurgaon, our emphasis is on the capacity of the RO Plant and the number of treatment stages that will be required for a particular application as well as the quality of the water source.

Plant Capacity

The commercial RO system installed has a product water capacity of:

Parameter Value
Product Water Capacity 1000 Litres Per Hour (LPH)


This implies it is capable of delivering about 1,000 litres per hour of RO water under the plant’s operating and feed-water conditions.

Capacity must be determined based on a number of considerations such as:

Capacity Consideration
Daily treated-water requirement
Peak water demand
Number of operating hours
Available raw-water storage
Treated-water storage capacity
Feed-water quality
Membrane performance
Required product-water characteristics


A theoretical yield can be calculated: For a 1000 LPH plant, if it is able to work for 8 hours, then the theoretical output is about 8,000 litres. The theoretical production at the same time of effective operation is about 10,000 litres.

The actual production may change depending on the feed-water temperature, pressure, condition of the membrane, concentration of dissolved-solids, fouling, maintenance and other operating conditions.

This means that Skylark is able to deliver commercial scale water production with a 1000 LPH capacity, but not with a much larger treatment plant.

Treatment Technology

The key purification technology applied in the project is Reverse Osmosis (RO) together with the appropriate pre-treatment.

Reverse osmosis is a pressure driven membrane separation process. The water is pushed across a semi-permeable membrane, creating product water or permeate and reject water or concentrate, which is a concentrated stream.

The pretreatment decreases the loading rate on the membranes, fine filtration gives further protection against particulates, the high-pressure pump creates the pressure for membrane separation, and the RO membranes decrease the concentration of dissolved material in the product-water stream.

The plant can be systematically maintained and a practical solution for commercial water treatment is possible.

Influent Characteristics

An RO plant‘s performance is highly dependent upon the properties of the influent, or raw water entering the plant.

For commercial RO systems, some key feed-water parameters that are normally considered in designing and operating systems are:

Influent Parameter
Total Dissolved Solids (TDS)
Total hardness
Calcium and magnesium
Turbidity
Suspended matter
pH
Chloride
Alkalinity
Iron, where present
Hard Minerals (Silica, etc.)
Organic matter
Microbiological Condition


Treatment Process

The 1000 LPH Commercial RO Plant consists of a series of treatment units that work together in a coordinated manner.

1. Raw-Water Feeding

Raw water is initially delivered to the pretreatment part by the feed line. Flow of feed is essential as subsequent equipment relies on a steady supply of feed water.

2. Pressure/Media Filtration

The primary filtration section filters out suspended impurities and turbidity.

Particulate loading is reduced at this stage which leads to less loading of fine filters or RO membranes.

3. Activated Carbon Treatment

Activated carbon treatment is available to remove chlorine, odour and some organic material in feed water if needed.

Granular activated carbon is widely utilised in water treatment applications for the adsorption of taste and odour-causing compounds and a number of organic contaminants.

4. Antiscalant Dosing

If scaling has the potential to occur, controlled antiscalant dosing can decrease the growth of mineral deposits on membrane surfaces.

As scaling builds up it can decrease membrane output, increase differential pressure, and over time increase maintenance needs.

5. Micron/Cartridge Filtration

Water flows through fine cartridge filtration before going to the high pressure RO section.

This provides another protection to keep small suspended particles away from the membrane elements.

6. High-Pressure Pumping

This high-pressure pump raises the water pressure to the amount necessary for a good reverse osmosis.

The RO process is dependent on pressure and requires it to push water through the semi-permeable membrane.

7. RO Membrane Separation

Water is split into two streams in the membrane housings.

These are referred to as RO permeate, which flows through the membrane at much lower levels of many dissolved substances.

The second is the concentrate or reject stream that contains more of the substances that are rejected by the membrane.

The EPA also explains RO as generating a permeate/product water stream and a reject/concentrate stream.

8. Treated-Water Collection

The RO permeate is finally channeled to the intended treated water storage facility for distribution and use.

Major Equipment

Skylark Gurgaon‘s 1000 LPH Commercial RO Plant features all necessary equipment needed for a commercial water treatment system.

The main functional elements are:

Equipment
Raw-water feed arrangement
Feed-water pump
Pressure/media filtration system
Activated carbon filtration is used
Antiscalant dosing system
Micron cartridge filter
High-pressure pump
Commercial RO membrane elements.
Membrane pressure housings
Pressure gauges
Product-water flow monitoring
Reject-water flow monitoring
TDS/water-quality monitoring arrangement
Control panel
Valves and inter-connections pipelines
Treated-water outlet arrangement
Reject-water discharge arrangement


Equipment was set up both to be functional and accessible.

Maintenance or inspection of parts such as filter elements, dosing equipment, membrane housings, pumps and instruments requires regularity, particularly in a commercial RO plant, where accessibility is of paramount importance.

A quality commercial RO system should therefore be capable of yielding treated water, but also be designed to serve a long time.

Installation Process

The installation process was systematically conducted so that the RO plant is able to function after its commissioning.

A review of the available installation area and the selection of suitable locations for the RO skid and pretreatment equipment was the first step.

Wherever possible, working space was kept clear around the treatment units to enable routine changes of the filters, pressure checks and maintenance to be carried out conveniently.

Post equipment positioning, the raw water line was hooked up to the feed section and interconnections between the pretreatment components and the RO system were made.

The product-water piping and reject-water piping were not connected to each other so as to avoid mixing of the two streams.

Electrical connections to the feed pump and the high-pressure pump were then made, along with the feed pump, dosing system and control panel.

The installation team preperformed the following checks before starting the plant:

Pre-Startup Check
Pipe connections
Valve positions
Electrical connections
Pump direction
Filter installation
Membrane housing connections
Pressure lines
Conveying product and reject outlets
Potential leakage points


The process of installation was systematic which facilitated controlled startup and commissioning of the system.

Plant Commissioning

Commissioning of plants is the point where the installed equipment is tested as a whole water-treatment system.

Firstly, the 1000 LPH RO plant was flushed to prepare the filtration section and membrane section for normal operation.

Feed pump was then operated and then low pressure section was started in a controlled way.

The technical team was monitoring the operating condition such as feed-flow, pressure, product-water generation, reject-water discharge etc. during the commissioning.

Leaks were tested and the pressure and operation of the pumps were monitored for any abnormality.

The plant was slowly ramped up to operating conditions to avoid unnecessary hydraulic stressing of the plant.

The treated water production rate was verified against the desired plant capacity of 1000 LPH

There was also basic operational guidance provided in the commissioning process, such as:

Operational Guidance Topic
Plant startup
Plant shutdown
Pressure observation
Product-water monitoring
Cartridge-filter replacement
Chemical dosing
Membrane maintenance
The detection of abnormal flow and/or pressure.
Preventive maintenance requirements


Following successful testing and adjustment, the plant was made ready for routine operation.

Treated Water Reuse

The treated water from the plant can be stored in a separate treated water tank until such treated water is required for Skylark‘s own water usage.

Depending on the quality needed for each application, treated water can be used for:

Treated Water Use
After required final treatment and verification, drinking-water supply.
A full pantry and kitchen will be supplied.
A well-equipped kitchen and pantry will be provided.
Office utility requirements
Appropriate equipment or process applications
Other purposes with relatively lower TDS water


The actual end use should always determine the required final water-quality specification.

If treated water is to be used for human consumption, then hygienic storage and disinfection as required, and routine laboratory testing should be observed. IS 10500:2012 specifies requirements for drinking water in India, which can be used to evaluate the water quality parameters relevant to it.

The reject water from RO system should be disposed properly. The EPA states that the concentrate stream will include salts and other materials that are trapped by the membrane, and therefore, should be treated appropriately before being discharged or managed.

Only the reject water’s quality and the needs of the intended non-potable use should be taken into account when considering possible reuse.

Results and Performance

The successful installation and commissioning of the 1000 LPH Commercial RO Plant at Skylark Gurgaon has enabled the facility to have a dedicated on-site water-treatment system which can provide about 1,000 litres of RO water per hour under its specified operating conditions.

The project was successful in achieving the project objective of having a stable commercial scale production of treated water using a structured pretreatment and membrane-separation process.

The main results are:

Result Description
Well defined treated water production The plant offers treated water as a separate source of water rather than relying only on smaller point-of-use water purifiers.
Commercial scale capacity A rated capacity of 1000 LPH is considered a reasonable scale of production/capacity to install.
Removal of dissolved mineral content RO Membrane technology is used specifically for the removal of a variety of inorganic constituents and dissolved solids.
Pretreatment for membrane protection Proper filtration prior to the RO stage can minimise fouling and plugging, which are known operational issues of membrane treatment.
Easy system monitoring Pressure monitoring points, flow monitoring points and water-quality monitoring points allow system operators to monitor plant operation during regular operation.
Sustainable equipment layout System installed to allow convenient access to consumables and major equipment needing routine maintenance.


This overall installation thus provides both 1000LPH purification capacity and a complete commercial treatment solution including pretreatment, membrane separation, monitoring and the collection of treated water.

Customer Feedback / Testimonial

Installing and commissioning processes were executed professionally, keeping in mind operational ease and system reliability.

After commissioning, basic maintenance and operation of the plant was demonstrated to the concerned personnel.

As a result of not having received an independently verified customer quotation for this case study a direct statement must not be attributed to Skylark without permission.

The installation and commissioning of the 1000 LPH Commercial RO Plant in our Gurgaon facility is done professionally and the plant is functioning well as per our water treatment requirement and the technical team gave us proper guidance about the operation and routine maintenance of this plant.

Looking for a trustworthy Commercial RO Plant Manufacturer in Gurgaon for your office, factory, hotel, school, hospital, warehouse, commercial complex or industrial plant?

Some of the points to consider in a well-designed system:

Design Consideration
Raw-water quality
Daily water requirement
Peak demand
Required treated-water quality
Available operating hours
A space that allows for the installation of equipment.
An area that can accommodate equipment.
Pretreatment requirements
Water storage
Maintenance requirements
Intended treated-water application


We supply complete solution from the designing to manufacturing, installation and commissioning of RO Plant for Commercial applications in Gurgaon for various capacities.

Commercial RO plant can be designed in various capacities like:

Available Capacities
500 LPH
1000 LPH
2000 LPH
3000 LPH
5000 LPH
10,000 LPH and customised capacities


Our services include water-treatment requirement assessment, system design, equipment selection, RO plant manufacturing, installation, commissioning, operator guidance, membrane replacement, filter replacement, troubleshooting and preventive maintenance support.

Our track record of delivering water-treatment projects from conception to commissioning, such as the 1000 LPH Commercial RO Plant at Skylark Gurgaon, showcases our capabilities in delivering commercial water-treatment projects.

If you require a dependable Commercial RO Plant Manufacturer in Gurgaon, contact our technical team.

Read some interesting information for the Effluent Treatment Plant Manufacturer in Faridabad

Conclusion

The 1000 LPH (Commercial RO Plant) installed at Skylark Gurgaon is testament to the significance of selecting the right plant capacity, pretreatment, membrane technology and professional commissioning under one umbrella solution.

Skylark is an infrastructure and engineering company that has offices in EPC (Engineering, Procurement, and Construction) and other sectors such as mines, tolls, and highways.

When a commercial facility is being used, the reliability of the water treatment will not only be determined by the rated capacity of the RO plant but also by factors such as incoming water condition, pretreatment performance, proper operating pressure, membrane condition and periodic maintenance.

The 1000 LPH system meets these needs with a series of systematic treatment processes that involve raw-water feeding, pretreatment, fine filtration, high-pressure pumping, and RO membrane separation and output of product water.

While RO is an established membrane separation process for decreasing dissolved solids and a host of other contaminants, system pretreatment and concentrate management are important factors in proper system operation.

As a Commercial RO Plant Manufacturer in Gurgaon, the project has also provided another hands-on example to understand our capability to deliver commercially appropriate water-treatment systems based on capacity, water quality, and operational requirements.

For businesses planning a new RO installation or upgrading an existing treatment facility, a properly engineered commercial RO plant can provide a dependable, scalable and manageable source of treated water for long-term use.

Contact Netsol Water at:

Contact Details
Phone +91-9650608473
Email enquiry@netsolwater.com


What-are-the-Applications-of-Commercial-Water-Softeners-2.webp

August 13, 2026by Netsol Water

Successfully Installed 2000 LPH Commercial RO Plant at Boutique International, Gurgaon

Consistently treated water is important for commercial and industrial operations that rely on water consistently and continuously. The composition of raw water, including dissolved salts, hardness, suspended matter and other water properties, can vary and impact the usefulness of the raw water for drinking, utilities, processes. The combination of appropriate pretreatment with membrane purification would present an effective solution provided by a suitably designed commercial RO plant. The RO plant of 2000 LPH Commercial RO Plant was successfully installed and commissioned at Boutique International, Gurgaon and they were provided with a reliable source of treated water of about 2000 litres per hour based on the operating conditions provided.

Boutique International is a vertically integrated garment Export Company based in Gurgaon. It has knitting, embroidery, printing and other apparel manufacturing activities and is manufactured in its facility in Gurgaon.

The project reflects our expertise as a Commercial RO Plant Manufacturer in Gurgaon and most importantly, designing treatment systems as per the plant requirements, feed water quality available at the site, output capacity required and operational needs of the client.

Project Overview

The aim of the project was to supply a viable commercial scale water treatment plant for Boutique International that will produce 2,000 litres per hour of treated water.

The quantity of water required is not the only factor to consider before installing a commercial RO plant, the characteristics of the feed water must also be taken into account. RO membranes are primarily meant to separate the dissolved contaminants from water, and pretreatment is used to abate suspended particles, scaling, etc., that can impact the membrane.

Thus, it was decided that the solution will be an integrated treatment system instead of a standalone RO membrane unit. The removal of material from the raw water, generating the pressure, separation in a membrane, monitoring and treating the water out of the membrane were all taken into account, in order to ensure the plant’s operation under commercial conditions.

The project involved site assessment, capacity planning, equipment selection, system fabrication, transportation to the facility, installation, electrical and plumbing connections, flushing, trial operation, parameter adjustment and final commissioning.

The system once installed, gives Boutique International a separate RO water-treatment system of 2000 LPH for assured everyday operation.

Client Details

Boutique International is a garment manufacturing and export company from Gurgaon, Haryana, which was the client for this project.

Boutique International calls itself the star export house for apparel brands in the United States and Europe recognised by the government. The company claims its manufacturing process is vertically integrated, that is all the process from yarn to finished goods are done at the company’s facility. It has the facilities of circular knitting, flat knitting, embroidery and printing.

Infrastructure reliability is crucial in an organisation that operates at this level. All water-treatment facilities need to be able to deliver the treated water needed in the required quantity, and not make routine operation and maintenance unnecessarily complex.

The need was thus for a commercial system, not a small domestic purification system. The chosen capacity of 2000 LPH was deemed to be an appropriate balance of the water demand, operational capability and future utility.

Project Location

The commercial RO plant was installed in Boutique International, Plot No. 553, Pace City 2, Gurgaon, Haryana – 122016.

The town Gurgaon or Gurugram has emerged as a very important business and industrial hub in Delhi NCR region. The nature of water may vary greatly depending on whether it comes from a municipal water supply, a ground water well or a tanker.

So, it is not right to choose commercial RO plants only on the basis of the rated production capacity. The characteristics of the feed-water, treatment time, and pretreatment time, storage facilities, and the water quality to be expected after treatment, must also be taken into account.

As a Commercial RO Plant Manufacturer in Gurgaon, we therefore do not follow a one design fits all principle instead we ensure that the treatment configuration is personalized to fit the actual site needs.

Plant Capacity

The rated treated water production of the installed plant is: 2000L/h (Litres per Hour)

Parameter Value
Rated Treated Water Production 2000 L/h (Litres per Hour)


The system can generate around 2000 litres of RO treated water in an hour when operated at its full capacity. The actual daily production will vary depending on the operating time, feed-water condition, membrane performance, maintenance condition, and water need of the facility.

The theoretical production capacity of a 2000 LPH plant is, for example, about 16 000 litres during a period of 8 effective production hours. But the plant does not have to run around the clock—operation can be synchronized with treated-water storage and actual consumption.

The capacity selected is enough for commercial scale output, while treated water production and storage will follow the facility’s production schedule.

Treatment Technology

The RO process with the proper pre-treatment technology represents the main treatment process adopted in the plant.

Reverse osmosis is a method that uses pressure to push feed water through a special membrane to extract some of the water. This results in two streams of water, the purified water or permeate, and a more concentrated stream of water called the concentrate or reject water, which contains the dissolved substances that were not purified. RO is a membrane-separation technology capable of separating a wide spectrum of dissolved contaminants and salts.

But RO membranes should not be fed inadequately treated feed water. Scaling compounds, suspended matter, and chlorine and organics may have an impact on membrane life and performance.

Influent Characteristics

Incoming water quality is one of the most crucial factors to consider while designing any commercial RO plant.

Dissolved salt, minerals which form hardness, suspended solids, turbidity, chlorine and organic matter can be found in varying amounts in commercial feed water.

The treatment system was designed to address the key parameters, which typically affect commercial RO operation, such as:

Total dissolved solids, hardness, suspended particles, turbidity, scaling potential and contaminants that could impact the performance of the membrane.

Pretreatment is particularly important because it is not only to enhance the quality of the feed water, but to avoid fouling or scaling of RO membranes before they are used. DuPont says proper pretreatment ensures good RO performance and that the pretreatment required is a function of the chemistry of the raw water and the purpose of the treated water.

If the water is to be used for drinking, it is prudent to test its final quality with the right tests. The drinking-water specification of Bureau of Indian Standards (BIS) IS 10500:2012 suggests that the acceptable range for TDS is 500 mg/L and permissible range is 2,000 mg/L without any source. This same standard establishes acceptable hardness levels between 6.5 and 8.5, as well as limits for chloride, fluoride, nitrate and many other parameters.

BIS IS 10500:2012 Parameter Value
TDS – Acceptable Range 500 mg/L
TDS – Permissible Range (No source) 2,000 mg/L
Acceptable Level 6.5 to 8.5


Treatment Process

The 2000 LPH Commercial RO Plant is designed to pass through a series of treatment stages that help prevent damage to the membranes and assure a consistent product-water quality.

The raw water is pumped into pretreatment section first. The suspended matter is filtered out initially and the load is reduced to the later filter elements.

The water is then filtered through media filters. This stage is useful in controlling turbidity, suspended impurities, colour, odour and substances which may affect the operation of the RO membrane depending on the nature of the raw water.

When incorporated, activated carbon treatment acts as an important barrier to protect the membranes from the presence of chlorine and some of the organic compounds before they reach the membranes. This is especially important since improper feed-water conditions can adversely affect the performance of the membrane.

Fine cartridge filtration is another physical barrier to small suspended particles that is offered before membrane treatment.

A high-pressure pump is used to pump the pretreated water to the RO section. Reverse osmosis requires pressure due to the natural tendency of dissolved salts to move across a semi-permeable membrane.

The feed flows inside the RO membrane housing, splitting into a product water and a concentrate stream. Water passing through the membrane becomes the product water and continues to treated water storage, while a higher concentration reject water stream removes a significant amount of the dissolved substances separated.

During operation, flow and pressure parameters are monitored along with water quality parameters to detect any abnormal conditions and correct them.

Major Equipment

The main components needed for the pretreatment, membrane purification, monitoring and controlled operation were set up in the commercial RO system.

The major functional equipment consisted of:

Equipment
Arrangements for feeding raw water and water feeding pump.
Pressure/media filtration system
Activated Carbon Treatment, when needed based on feed-water conditions
Antiscalant dosing arrangement
Micron/cartridge filtration
High-pressure RO pump
Monitoring of product-water and reject-water flow.
Temperature and operating controls
Electrical control panel
Interconnection of piping, fittings and valves.
RO-treated-water outlet/storage connection


The equipment size was scaled to the product water requirement of 2000 LPH and operating condition.

The design also took ease of operation and maintenance into account since the installation of successful commercial water treatment relies not only on a good installation, but also regular monitoring, changing filters, maintaining membranes and timely servicing.

Installation Process

Installation started by surveying the plant space and existing utility services.

RO skid and pretreatment equipment were located for good accessibility for future maintenance and filter change out. The positioning of equipment is especially critical in commercial installations as the layout could become unnecessarily complicated to service the equipment routinely.

The inlet plumbing for raw water was connected to the pretreatment system, and connections between the treatment stages were made. Careful checks were made on the high pressure line, membrane housings, product-water outlet and reject water discharge line.

Pumping and dosing equipment and the control panel were electrically connected. The system was then checked for correct positioning of the valves, piping alignment and leaks.

With mechanical and electrical connections checked, individual system sections were ready for flushing and start-up.

Installation method – The approach was designed to reduce disruption to the client’s existing operations and provide easy access to the water-treatment equipment for future maintenance.

Plant Commissioning

Commissioning is one of the most important phases of a commercial RO project as good installation does not guarantee good operation.

The system was initially flushed to clear any loose material that may have been encountered during installation, and to ready the filters and membrane system for use.

The pumps were then gradually started and increased pressure applied in a controlled manner. The feed-water flow, product-water flow and reject-water flow were monitored as the system approached normal operating conditions.

The team inspected the system for leaks, abnormal pump performance, pressure and flow blockages during the commissioning. RO operating parameters were optimized for stable operation, while avoiding undue stress to the membranes.

The product-water output has been validated with the desired capacity of the plant, namely 2000 LPH subject to the condition of operating conditions and the quality of feed-water.

Routine startup and shut down, pressure monitoring, cartridge-filter replacement, chemical dosing, membrane cleaning indicators and preventive maintenance were also discussed with the operators.

Treated Water Reuse

The water that is treated through RO system can be stored in a separate tank, and can be pumped to specific locations where the facility needs low TDS water.

RO treated water can be used to prepare drinking water, to meet pantry needs, for utility uses and for appropriate process water needs based on the client’s internal water-management plan, where controlled dissolved-solids levels are desired.

For any end use, the distribution should be the same as the required water quality specification. If the water is used for drinking, the proper post-treatment, hygienic storage and regular microbiological and chemical testing are essential.

Concentrate management is also responsible for RO concentrate. Facilities may consider whether they can make a suitable non-potable use of the reject-water stream depending on its quality and the local needs. Testing and the needs of the intended use should be considered when making a reuse decision.

Results and Performance

The installation and commissioning of 2000LPH Commercial RO Plant at Boutique International, Gurgaon was a great success, it gave the facility its own high capacity treatment system to produce purified water there.

The main aim of the project, which was to set up a reliable RO water production system with a rated capacity of around 2000 litres per hour was achieved.

After commissioning, the stable operation of the system with controlled feed pressure, product-water generation, and reject flow were identified. The RO membrane stage achieved high removal of dissolved mineral matter from the feed water, and pretreatment prevented particulate and scaling loading of the membrane system.

The primary operational advantages of the installation are the assured commercial scale water production, reduced reliance on small-scale purification units, ability to control the availability of treated-water, improved management of the dissolved solids and hardness, and the plant configuration which allows for easy monitoring of system performance and for routine service.

RO membrane technology is a proven technology for commercial and industrial water treatment. Commercial RO membranes are utilized in a wide variety of applications, from restaurants and hotels to medical and scientific facilities.

The finished project provided Boutique International with a new facility water-treatment asset on top of its current facility infrastructure.

Customer Feedback / Testimonial

Installation was finished with special consideration for the performance of the plants, ease of access and ease of operation. The system was tested during commissioning and the operating procedures were discussed to the facility staff.

The 2000 LPH Commercial RO Plant has been installed at our facility in Gurgaon and we are pleased with the professional installation and commissioning of the RO Plant. The RO Plant is working as per our water-treatment requirement and the Technical team provided us the required support during installation, testing and handover.

In execution of this project success highlights the needs of using proper plant capacity together with proper pretreatment, reliable equipment, proper installation and technical support.

Call to Action

When it comes to selecting the best commercial RO Plant Manufacturer in Gurgaon, the decision is crucial if you have a factory, office, hotel, hospital, school, institution, warehouse or commercial facility which needs a reliable water-treatment plant.

A commercial RO system should be configured based on your specific water analysis, your daily water demand, the number of hours the system will be used, available space and the specific quality of water you want to produce—rather than just picking a capacity from a standard capacity chart.

We design, manufacture, install and commission the commercial RO plants for various water needs and operating conditions. The treatment configuration can be designed depending on the application and feed-water characteristics, if you need a 500 LPH, 1000 LPH, 2000 LPH, 3000 LPH, 5000 LPH or a customised commercial RO plant.

Available Capacities
500 LPH
1000 LPH
2000 LPH
3000 LPH
5000 LPH
Customised commercial RO plant


Services offered range from requirement assessment to designing the water-treatment system, selecting the equipment, manufacturing the RO plants, commissioning and training the operators, troubleshooting and providing equipment maintenance support and replacement of consumables and membranes.

The installation of a 2000 LPH Commercial RO plant at Boutique International, Gurgaon, showcases our capability to take on commercial water-treatment projects from system design to final commissioning.

Looking for a reliable Commercial RO Plant Manufacturer in Gurgaon? Contact us today and speak about your water requirement.

Provide us with your raw-water test report and daily water demand and our technical team will be able to suggest the capacity and treatment configuration of the RO plant required for your facility.

Read some interesting information for the Commercial RO Plant Manufacturer in Faridabad

Conclusion

The Boutique International project did not just use the RO membrane but included all the components of a complete treatment process, such as pretreatment, fine filtration, pressure generation, membrane separation, monitoring, commissioning and operational guidance. This is significant because the performance and life of the membrane is highly dependent on the quality of the water treated and the quality of pretreatment.

The system installed has a capacity of 2000 litres per hour and enables the Boutique International‘s Gurgaon facility to have a significant treatment water production capacity with the help of installed system. Reliable long term operation is also achieved through correct installation, system commissioning and equipment arrangement which is easy to access.

If any organisation is planning to install a similar RO Plant in Gurgaon, it is advisable to choose a Commercial RO Plant Manufacturer in Gurgaon to ensure that plant capacity, water chemistry, pretreatment and operational requirements are all taken care.

A business where treated water availability is a constant requirement can turn to a professionally engineered commercial RO plant for a reliable solution that is scalable and can provide them with the water they need.

Contact Netsol Water at:

Contact Details
Phone +91-9650608473
Email enquiry@netsolwater.com


What-are-the-Applications-of-Commercial-Water-Softeners-1.webp

August 12, 2026by Netsol Water

Successfully Installed 1000 LPH RO Plant at Capacite, Gurgaon

Purified water is important to commercial buildings, offices, construction sites, industrial sites, institutions and large workplaces. Raw water may contain dissolved salts, hardness, suspended particles, unpleasant taste or smell and other contaminants that are not desirable for direct use. A properly designed RO plant provides an effective solution by combining pre-treatment, membrane separation, process control, and water-quality monitoring.

Netsol Water has installed a 1000 LPH RO Plant at Capacite, Gurgaon, which is a commercial and industrial water purification plant that can produce high purity water. The installation illustrates the ability of the right size RO plant to satisfy the daily purified water need of a commercial water facility in a compact and manageable treatment setup.

This project serves as an excellent example of how plant capacity, treatment stages, equipment selection, installation, and commissioning can be linked to create an effective water-treatment system.

Project Overview

The project was the installation of Capacite 1000 litres per hour (LPH) RO plant in Gurgaon, Haryana. The primary goal was to obtain a dependable system for producing purified water on site for the facility rather than relying on the untreated incoming water or the supply of purified water from outside.

The product water capacity for a 1000 LPH plant is about 1,000 litres per hour per operating hour. The actual amount of production possible depends on the number of hours the plant is operating, the quality of the raw water, the feed pressure, the condition of the membranes, their maintenance, and the plant’s demand.

Netsol Water‘s commercial RO solutions rely on several treatment stages and not just the RO membrane. It has been documented that its commercial RO process encompasses the removal of suspended solids, treatment with activated-carbon, fine cartridge filtration, high pressure pumping, membrane separation, management of reject water, dosing, instrumentation and provisions for membrane cleaning.

The Capacite project is an important installation for Netsol Water as it further strengthens its reputation as a leading Commercial RO Plant Manufacturer in Gurgaon and the Delhi NCR region.

Client Details

The client for the project was the Capacit’e Infraprojects which is a company that is engaged in construction activities. It defines its sectoral presence as total contracting, general contracting and design-and-build services for such projects as high-rise buildings, super-high-rise buildings, commercial and office buildings, institutional buildings, hospitals, hotels, data centres, industrial buildings, mass housing, and other large projects.

Water availability becomes significant for the construction and commercial development, as well as infrastructure sectors, not just in providing drinking water, but also some functions within project offices and facilities.

A commercial RO system must then be tough enough to use regularly, and be easy to operate and maintain.

Project Location

The RO plant was setup in Capacite, Gurgaon. Gurgaon is among the important commercial and corporate cities of Delhi-NCR, which has a large number of offices, housing societies, hotels, institutions, construction sites, industrial units, etc. These facilities may need special water treatment facilities when the quality of the water is not satisfactory for the intended purpose.

Netsol Water in particular in Gurgaon offers commercial RO solutions and emphasizes the need for choosing a plant based on the number of users, water source parameters, water required capacity, installation site and maintenance needs.

Plant Capacity

The RO plant installed has the capacity of:

Parameter Value
Plant Capacity 1000 LPH
Equivalent Product-Water Output 1 m³/h


This is a capability that makes the system appealing to facilities that need a significant amount of purified water over the course of a workday, but the amount is not too much to handle.

The rated capacity, for instance, refers to the theoretical capacity that the plant can achieve, for example, at 8 hours operating time it can deliver around 8000 litres, at 10 hours it can deliver around 10000 litres subject to actual operating conditions and availability of feed-water.

The sizing of plants is an important engineering design decision. Both an undersized and an oversized RO plant can have drawbacks in terms of meeting peak consumption and/or operating the plant efficiently. The 1000 LPH capacity offers a realistic compromise between capability, size, usage and commercial water demand.

Treatment Technology

RO is the main treatment technology being utilized in the project.

RO is a membrane separation technique where the pretreated water is subjected to pressures and allowed to flow through semi-permeable RO membranes. The water molecules traverse the membrane as purified permeate while a large percentage of the dissolved salts and other constituents that are not allowed to pass through are left on the concentrate side of the membrane and exit through the reject line.

But this successful RO performance relies on proper pre-treatment. If the untreated water is fed directly to RO membrane, it may lead to fouling, scaling, pressure demand, frequent cleaning and deterioration of the membrane.

The commercial RO treatment unit by Netsol Water, therefore, includes several treatment mechanisms, namely the sand filter, the activated carbon filter, the micron filter, the high pressure pump, the membrane, the dosing system, the instrumentation and the cleaning system.

This multi-stage approach is designed to help protect and stabilize the system performance of the membrane.

Influent Characteristics

One of the key components of commercial RO design is influent assessment. The following are some of the parameters that are usually assessed prior to the finalization of an RO system:

Influent Parameter
Total Dissolved Solids (TDS)
Electrical conductivity
pH
Total hardness
Calcium and magnesium
Chloride
Sulphate
Alkalinity
Turbidity
Suspended matter
Iron, where relevant
Organic matter


Depending on the water source, microbiological contamination occurs.

Water-quality parameters like pH, EC, TDS, total hardness, calcium, magnesium, alkalinity, chloride, sulphate, nitrate, fluoride, sodium and potassium are also listed as important water-quality parameters in Haryana’s water quality testing infrastructure.

This treatment system was designed to solve the larger problem of the conversion of the incoming water into a reliable high purity product-water supply, for the Capacite project, rather than simply basic filtration.

Treatment Process

The treatment sequence is in accordance with the multi-stage treatment principle proven in the commercial RO systems of Netsol Water.

A system for removing dissolved solids from raw water that includes feed pump, pressure sand filter, activated carbon filter, micron filter, scale control, high pressure pump, RO membranes, storage and use.

Stage 1: Raw Water Feeding

Water is pumped into the plant by means of a feed pump at the appropriate flow and pressure into the pre-treatment system.

Stage 2: Pressure Sand Filtration

Water is first filtered in the sand filter stage. This will help to remove any suspended solids or larger particulate matter that might enter the cartridge filters and/or RO membranes.

Stage 3: Activated Carbon Filtration

Activated-carbon treatment is the next step. Activated carbon is part of its commercial sequence for dechlorination by Netsol Water. Another property that can be modified by carbon treatment is the water properties, by removing some of the organic compounds that cause undesirable taste and odour.

Stage 4: Micron Cartridge Filtration

Fine filter before high pressure section, with a micron filter. It is a secondary barrier to smaller suspended particles.

Stage 5: Dosing and scale protection

The use of the proper chemicals allows control of scaling at the surface of the membranes. Often, the membrane is scaled and this can lead to lower permeate flow and higher operating pressure, which require protection for the long-term stable operation.

Stage 6: High-Pressure Pumping

The pre-treated water is pressurised by the high-pressure pump. The purified water must be pushed through the RO membrane against the osmotic pressure which requires adequate pressure.

Stage 7: Reverse Osmosis Membrane Separation

The water is split into two streams within the membrane system:

Stream Description
Product water Water that has been treated to be used for various purposes.
Rejected/Concentrated Water with a greater concentration of rejected dissolved materials.


The permeate is directed to a storage tank or used as is, with the concentrate being directed to the reject or recycle system, depending on the plant design. Netsol Water refers to the same general process when referring to its commercial RO systems.

Major Equipment

The key equipment of a commercial RO system of this kind is:

Equipment
Raw-water/feed pump
Pressure sand filter
Activated carbon filter
Micron cartridge filter housing
Chemical/anti-scalant dosing arrangement
High-pressure RO pump
RO membrane housings
Reverse osmosis membranes
Flow meters
Pressure gauges
Conductivity/TDS monitoring instruments
Level-control switches
Control panel
Product-water line
Reject-water line
Installing piping and valves between different units.
Connecting pipes and valves between units.
Structural/skid arrangement


Netsol Water specifically records pressure gauges, flow meters, conductivity sensors and level switches for monitoring the performance of commercial RO systems and provides a description of a CIP system for maintaining the membranes.

These components combine to give not just filtration, but an environmentally regulated water-treatment process.

Installation Process

Installing an RO plant is no simple task; it must be done successfully. Mechanical, Electrical, Hydraulic, and Control components should function in a coordinated manner.

Netsol Water has confirmed success with 1000 LPH installation on the Capacite project.

A commercial structured RO installation would involve determining the space for the plant, positioning the filtration vessels and the RO skid, installing pipelines for raw water and product water, routing the reject line, connecting the pumps and the control panel, instrumenting and installing dosing lines, inspecting valves and pressure points, and ensuring product-water storage.

After mechanical erection pipelines and electrical connections are checked prior to controlled plant start-up.

This is especially crucial for organizations choosing a Commercial RO Plant Manufacturer in Gurgaon, as product supply without proper installation and commissioning could lead to varying plant performance.

Plant Commissioning

Commissioning is a process that transforms an installed RO plant to an operating treatment plant.

The commissioning process includes feed-water availability, correct pump rotation and pressure, flushing of the treatment system, checking filters, setting chemical dosing, checking for leakages, checking flow through the RO membranes, observing permeate and reject streams, checking instrumentation and automatic controls.

Pressure, flow, conductivity and water-quality behaviour are monitored during initial operation. Stable plant conditions can then be obtained by making adjustments.

Netsol Water has successfully completed many commercial RO installations, and all of these are instrumented to track both water quality and operating conditions, such as pressure gauges, flow meters, conductivity sensors and level switches.

The installation at Capacite is the successful completion of going from the equipment deployment stage to an operational purification system of 1000 LPH.

Treated Water Reuse and Utilisation

The design of the RO plant was aimed to produce high purity water for commercial and industrial use, and Netsol Water‘s project announcement was dedicated to the industries, offices, and commercial complexes.

Purified RO water can have applications where controlled water quality is required at a facility like Capacite provided the final water specification for the product is acceptable and the internal water-distribution system is acceptable.

Producing purified water on site, instead of having to bring the purified water into the site, may also help to minimise reliance on external supply of purified water, and enable the site to have more control over the water supply for the day.

Quality of the RO reject stream should always be managed based on the site requirements and quality of the RO reject stream. Where technically feasible, reject water can also be assessed for non-potable purposes, rather than be needlessly wasted.

Results and Performance

The successful installation of a rated 1000 LPH commercial and industrial RO plant at Capacite, Gurgaon, was the main outcome of the project.

The key results of the major project are:

Result
The installation of an on-site water purification system is made possible.
Dedicated water purification system on-site is enabled.
Purified-water production capacity of 1000 LPH (litre per hour) rated water.
1000 LPH (litre per hour) rated water for purification.
Treatment in multiple stages instead of one stage
The protection of RO membrane pre-treatment.
The separation of concentrated reject water and purified permeate.
Operational monitoring is provided.
A small system for commercial applications
Minimized reliance on untreated water supply for purified water uses
A treatment plan that is systematic and can be maintained and serviced over time


Customer Feedback and Project Acceptance

The importance of this ongoing relationship is that acceptance of a project in the commercial water-treatment industry involves not just providing equipment, but also engineering services, installation, service responsiveness, and confidence in ongoing support.

The Capacite is thus an important reference project for companies looking at the Commercial RO Plant Manufacturer in Gurgaon, Netsol Water.

How Netsol Water is Considered as a Leading Commercial RO Plant Manufacturer in Gurgaon?

The first step in plant selection is not necessarily to look at price or nominal capacity, but to consider what the requirement for the water is.

Netsol Water is producing commercial RO plants in various capacities and states and claims to offer customisable systems as per the customer’s requirement. It has documented treatment process that includes pre-filtration, activated-carbon treatment, cartridge filtration, high-pressure RO membranes, dosing, instrumentation and membrane-cleaning provisions.

Netsol Water also covers Gurgaon in the list where it supplies water-treatment plants and also provides commercial RO plants for various applications such as industries, commercial water plants, institutions, housing societies, hostels, restaurants, hospitals etc.

The successful installation of a 1000 LPH Commercial RO Plant in Capacite is a testament to Netsol Water‘s ability to transform a commercial water requirement into a treatment solution that is installed on-site.

Read some interesting information for the Sewage Treatment Plant Manufacturer in Faridabad

Call to Action!

When your office, commercial complex, hotel, hospital, educational institution, housing society, construction project or industrial facility needs a reliable RO water-treatment system, Netsol Water has the answer to find a plant of your choice that meets your raw water quality, required purified water capacity, operating hours, available installation space, and intended water application.

Selecting the right system configuration can provide you with better water quality and save downstream applications while also ensuring a reliable supply of purified water, whether you need a 500 LPH, 1000 LPH or a higher capacity commercial RO plant.

Are you searching for a reputed Commercial RO Plant Manufacturer in Gurgaon?

For consultation, water analysis, selection, design, manufacture, installation, commissioning and post installation support for water systems contact Netsol Water.

Contact Details
Call +91 9650608473
Email enquiry@netsolwater.com


What-are-the-Applications-of-Commercial-Water-Softeners.webp

August 11, 2026by Netsol Water

Successfully Installed 3,000 LPH RO Plant at ACC Cement RMC Plant, Gurgaon

A good water quality is essential in a ready-mix concrete (RMC) plant since the water becomes an integral part of the production environment and can affect the consistency, process control, equipment maintenance, and final product quality of the concrete. Netsol Water‘s 3000 LPH RO plant was installed at ACC Cement Ready Mix Concrete plant in Gurgaon to improve its supply of process water. The installation has been well documented by the project team of Netsol Water as a 3000 LPH RO plant to produce high-quality water for the RMC process.

The project shows Netsol Water the real-world benefits of using the right RO capacity, treatment and automation along with site commissioning for an industrial customer. It also demonstrates the importance of choosing an experienced commercial RO plant manufacturer in Gurgaon when the treatment plant is to be used along with the manufacturing activity.

Project Overview

The project was to supply and install a 3000 litres per hour (LPH) RO plant at an ACC Cement RMC plant in Gurgaon, Haryana and test and commission it. The information provided on the public project material is specific to:

Parameter Details
Customer ACC Cement Customer
Application Ready Mix Concrete
Plant Capacity 3000 LPH
RO plant supplier/Installer Netsol Water


The essential goal of the core project was to develop a reliable supply of treated water for the RMC process on site. The RO plant offers a controlled treatment barrier as opposed to just treated source water that may contain varying amounts of dissolved minerals.

The reverse osmosis process operates by pressurizing water to force it through a membrane that allows only water to pass, leaving a purified stream of water and a stream of reject or concentrate. The U.S. Environmental Protection Agency states that RO will remove many dissolved solids and inorganic contaminants from water.

From there the capacity of the 3000 LPH was chosen because it was a practical level for a plant that has variable process-water needs throughout the working day, but robust enough to allow for industrial-scale production. The unit will produce up to 3,000 litres of treated water per hour at nominal capacity.

Client Details

Field Details
Client ACC Cement / ACC Limited
Industry Cement, building materials, and ready-mix concrete
Process water Water used in the production process at the RMC plant


ACC Limited is one of the reputed manufacturers of cement, building materials, and ready-mix concrete in India and is currently part of the Adani Portfolio. According to ACC’s official website, the company has a huge national operating presence with over 117 ready-mix concrete plants.

Controlled batching and repeatability is essential to RMC production. Water is one of the fundamental requirements to make concrete, so a more reliable treated water supply can help with process control.

Project Location

The plant was installed in the premises of ACC Cement Ready Mix Concrete (RMC) plant in Gurugram (Gurgaon), Haryana. Gurugram is an important industrial, commercial, residential, and institutional city of Delhi NCR, having industrial activities, construction activities, institutional activities, hotel and hospitality activities and commercial activities which demand reliable water treatment system. Netsol Water is also a company that supplies commercial RO solutions to Gurgaon only and offers project services like design, installation, testing and support.

The project is also a good local benchmark for companies looking for a reliable Commercial RO Plant Manufacturer in Gurgaon for medium and large scale industrial applications.

Plant Capacity

The installed system is capable to produce 3000 LPH of treated RO water with the given design conditions. According to a published RO product information, Netsol Water‘s 3000 LPH RO unit is a fully automatic reverse osmosis configuration, appropriate for industrial water treatment.

A 3000 LPH system offers valuable flexibility of operation. It can be used for up to 24,000 litres of treated water per hour when running at full capacity. The actual daily production will vary based on the quality of the feed water, plant demand, recovery, storage space, cleaning cycles and operating pressure.

This capability is suitable for an industrial facility that has a much higher demand for treated water than a small commercial facility.

Treatment Technology

RO is the primary treatment technology used.

RO Systems: Pretreated feed water under pressure and forced through a semi-permeable membrane. The water molecules pass preferentially through the membrane and the reject stream carries off a portion of the dissolved salts and other rejected constituents, with a more concentrated reject stream.

Making water clear is not the sole significance of RO for an RMC plant. Its aim is to lower ionic loading of the water and maintain uniformity of the water provided to quality sensitive plant uses. EPA has designated RO as a technology that can remove a wide variety of dissolved solids and inorganics.

Influent Characteristics

Industrial RO plants may be used for source water that contains suspended matter, hardness-forming minerals, dissolved salts, alkalinity, and other components that can impact RO system performance. These factors dictate the pretreatment needed, operating pressure, antiscalant programme, cleaning frequency and recovery level.

For this ACC Cement project, the public installation material does not show laboratory values for inlet TDS, hardness, turbidity, pH, silica, iron or alkalinity. Hence, this case study does not assign the numerical values of the influents.

The treatment configuration should rather be interpreted as a selection, which is made with the aim of making the feed water available in the required state and to minimize the content of dissolved matter in the feed water before it is used in the RMC process. It is technically correct as the RO performance is very sensitive to the chemical nature of the feed water and adequate pretreatment will ensure the membranes are not fouled or scaled.

The technical datasheet for the project should have the actual influent water analysis from the project or commissioning record from Netsol Water added.

Treatment Process

The sequence of the 3000 LPH plant is similar to that of a commercial and industrial RO treatment plant:

Raw-water feed → Pretreatment → Cartridge/micron filtration → Chemical conditioning (as needed) → High-pressure pumping → RO membrane separation → Collection of treated water → Supply to the RMC process.

The raw water first flows to the pretreatment area. Media filtration is used to remove suspended contaminants and to preserve the downstream components. Sand and carbon filtration are pretreatment components of the system along with high-pressure pumping.

Next, fine filtration offers an extra layer of protection of the membrane. Positioning of the antiscalant for dosing and other conditioning may be required to prevent mineral deposits depending on the feed analysis. The high pressure pump is, in turn, used to deliver the pressure needed for the membrane separation process.

In the RO membrane vessels, the feed is divided into two streams: the treated permeate and reject concentrate. The water from the treatment plant is stored for use in the process and the reject water is sent to the site’s approved water-management system.

Operating conditions are optimized during commissioning to ensure a stable flow, pressure and product-water quality.

Major Equipment

The key equipments used for the 3000 LPH RO system are:

S. No. Equipment
1 Transfer pump and raw-water feed system
2 Pressure sand/media filtration
3 Activated carbon filtration
4 Micron/cartridge filter housing
5 Chemical dosing system, including antiscalant
6 High-pressure RO pump
7 RO membrane housings and membrane elements
8 Pressure gauges and flow indication
9 Treated-water and reject-water piping
10 Electrical Control Panel/Automation
11 Valves, fittings and instrumentation
12 Treated-water storage/supply interface


Netsol Water‘s RO treatment yields 3000 LPH, that the treatment is fully automated, and that the RO treatment is of industrial scale, and its more extensive product are sand/carbon pretreatment and high-pressure pumps.

Installation Process

However, at a working RMC factory, co-ordination needs to be carried out such that water-treatment operations don’t needlessly interfere with production. The job of Netsol Water involved installation of 3000 LPH RO plant on site, which has been captured for the ACC’s Gurugram location.

A standard install process for a plant of this type will consist of foundation verification, positioning of treatment skid and filter vessels, raw water and treated water connections, reject drainage, electrical connections, pump rotation, pretreatment flushing, filter media loading or verification, cartridge and membrane install and finally valves and instrumentation checking.

Special care is needed in access for future maintenance. Filters, membrane housings, pumps and dosing systems must be serviceable following the commissioning. Reliable long-term operation is also achieved by proper pipe support, drainage, electrical safety and operator access.

After mechanical and electrical installation the system is taken to the testing and commissioning phase.

Plant Commissioning

Converting an installed RO system into a stable operating utility is called commissioning. First, mechanical and electrical checks, leak testing, line flushing, pump testing, pretreatment testing, and checking instruments and controls for proper response are performed.

The RO is then operated under controlled conditions. Operators gradually bring up the necessary feed pressure and monitor the flow of permeate, reject flow, pressure, and quality of treated water. The goal is not just to achieve 3000 LPH for a short period, but to create repeatable operation in the plant’s design envelope.

The last item to consider is operator handover. Regular checks are required on inlet/outlet quality, pressure differential, filter condition, dosing chemical level, permeate flow, reject flow, pump behaviour and indications of membrane fouling.

Treated Water Reuse

The main application of the treated water was in the RMC process. The above mentioned public project post on the Netsol Water website explicitly mentions the use of water of high quality for the Ready Mix Concrete process.

Process water in an RMC facility can be processed to be used for quality sensitive applications as per the internal SOPs of the plant and requirement for concrete production.

The main operational benefit is that the site now has a treatment step on site that is able to produce a controlled stream of RO permeate instead of sending untreated source water to all uses.

This also allows for more control to be exercised by the plant personnel over the water applied to applications where consistency is of great importance.

Results and Performance

The key achievement so far is the successful installation of a 3000 LPH RO system at the ACC Cement RMC plant in Gurugram and its operation for supplying good quality water to RMC process.

In operational terms, there are four distinct advantages to the installation. It establishes a separate treated-water supply within the facility. Second, RO removes dissolved contaminants and salts which permeate through the normal particulate filtration. Third, the 3000 LPH rating ensures production at an industrial scale, with appropriate process-water demand. Fourth, automation helps to maintain consistent operation, with reduced need for ongoing manual adjustments.

The project represents a suitable sized commercial or industrial RO plant to serve a manufacturing plant where water quantity and quality is significant.

Customer Feedback / Testimonial

The 3000 LPH RO plant was installed as part of our RMC facility and is in reliable operation, “We appreciate the help Netsol Water provided during installation and start-up.”

Call to Action (CTA)

For quality and reliable water purification, Netsol Water can design a system based on your actual feed-water quality, demand, and hourly consumption, whether you have an RMC plant, factory, hospital, institution, commercial complex, or industrial unit.

Netsol Water is a Commercial RO Plant Manufacturer in Gurgaon and provides Commercial RO water solutions along with Project support ranging from selection to design, installation, testing and commissioning as well as after sales support. It has a Gurgaon-based commercial RO page which says that businesses in this region can avail customised RO plants along with lifecycle support.

Need RO Plant in Gurugram for commercial or industrial use that delivers 3000 LPH?

Talk to Netsol Water about your:

S. No. Item to Discuss
1 Raw-water test report
2 Required treated-water quality
3 The water requirements for an hour and a day
4 The amount of water needed per hour and per day
5 Operating hours
6 Treated-water storage requirement
7 Desired automation level
8 Available installation space
9 The process or product has been applied to industry or commerce


For commercial enquiries about RO, contact the Netsol Water +91-9650608473.

Read some interesting information for the Industrial RO Plant Manufacturer in Noida

Successful installation of the ACC Cement RMC system illustrates the ability to use a relatively simple RO system at an industrial plant to deliver a consistent supply of water for process use, which is quality-focused. This project offers a real-world demonstration of a 3000 LPH Commercial RO Plant solution tailored for industrial applications.

When a combination of water analysis, pretreatment, membrane technology, automation, and professional installation and commissioning is used, the commercial RO treatment can be a reliable component of an industrial facility’s water-management infrastructure. This is a practical example of what is being done by Netsol Water at ACC Cement RMC plant in Gurugram.


Commercial-RO-Plant-Installation-Steps.webp

July 22, 2026by Netsol Water

Commercial RO Plant Installation Steps

Many industries and even commercial places require clean water. A commercial RO plant purifies impurities and provides safe water for drinking. This technology is crucial to the production of food for many industries in India, including manufacturing units, hospitals, and hotels. Other areas in India also suffer from water quality issues related to the presence of minerals and the season. Therefore, water treatment systems are crucial to ensure seamless operations.

We are one such leading company that offers complete solutions for water purification systems. To set up an RO system, it should be done with proper planning and correct execution. All stages impact the overall system performance.

Site Assessment and Requirement Analysis

In order to create a successful installation, it is important to have a proper requirement analysis and site assessment. This is a critical step because the system may not represent the actual water demand or working conditions without it. This stage guarantees proper placement of the plant and proper function. The first step in commercial RO plant installation is to perform a detailed study of the water quality and usage requirements. Let’s take a look at some of the key points in this stage.

1. Water Quality Analysis

Water quality analysis is used to gain an understanding of the level of impurities in the source water. The engineers take samples and test for salts, hardness, and other undesirable material. This information is useful for selecting the appropriate level of filtration. If the water being fed to the system is highly contaminated, a more powerful RO system will be needed. This ensures that the plant design is in line with actual conditions and that there are no future performance problems.

2. Space and Utility Evaluation

Space evaluation is also crucial for seamless installation. Engineers check the available area for placing equipment, tanks, and pipelines. They also inspect the electricity supply and drainage. Good spacing eases maintenance and safe operation. If the utilities are arranged properly, the system will operate continuously without interruptions and help produce water continuously.

Design and Engineering Planning for a System

The system is designed and engineered to determine how the plant will operate following installation. During this phase, collected data is transformed into a usable system plan. This is an important part of the process, since a well-designed commercial RO plant installation will help reduce operational problems and ensure optimal performance.

Let’s take a closer look at some of the key elements of this phase.

1. Capacity and Flow Design

The amount of water produced by the plant in a day is determined by capacity planning. The engineer determines the amount of water demanded based on the needs of the industry. They determine flow rates to ensure that the system can accommodate maximum use without a drop in pressure. This enables the output to remain consistent throughout working hours. Energy savings and balanced performance are other advantages of proper capacity design.

2. Technical Layout Planning

Technical layout planning involves the positioning and connections for each unit. Filters, pumps, membranes, and storage tanks are designed by the engineers. They also design routes for pipe installations to minimize pressure loss. A clean design helps minimize installation mistakes and simplifies future maintenance. This ensures the system is organized and efficient.

Equipment Procurement and Installation Process

The procurement and installation process is an important phase where the design materializes. Quality equipment guarantees stable production and long-term performance. Commercial RO plant installation relies on the right selection and correct installation of all the components. Let’s take a look at some of the key points of this stage.

1. Selection of RO Components

The membranes, pumps, filters, and control systems are among the RO components selected. The parts need to be chosen according to the design of the system and the water needs. High-quality components help improve efficiency and reduce the chances of breakdown. Engineers make sure that all parts will fit together. This step directly impacts water purity and system durability.

2. Physical Installation and Assembly

Physical installation refers to the process of installing equipment in the designed layout. Technicians connect pipes, wires, and control panels. All connections should be firm and secure to prevent leakage or pressure drop. Smooth flow of water is achieved by ensuring proper alignment of machines. A high level of skill is required for this stage, as even minor mistakes may impact the performance of the system.

Testing, Commissioning, and Maintenance Setup

Testing, commissioning, and maintenance setup allow the system to be verified as functioning properly prior to operation. In this stage, it is confirmed that all components are working as intended. Proper testing and final adjustments are an essential part of the steps involved in commercial RO plant installation.

Let’s take a look at some of the key elements of this stage.

1. System Testing and Performance Check

In system testing, water flow, pressure, and water purity are tested. The plant is operated by engineers for a few hours to check performance. They detect any leaks or imbalances in pressure. Adjustments are made to increase efficiency. This step helps ensure a continuous, safe, and clean water supply from the system.

2. Maintenance Planning and Support Setup

After installation, maintenance planning is used to ensure the plant maintains good condition. Filters and membranes are cleaned on a regular basis. Engineers also provide training for operators to monitor the system day to day. Good maintenance minimises breakdown and maximises system life. A healthy support network will help the system run smoothly and solve problems quickly.

Read some interesting information for the Sewage Treatment Plant Manufacturer

Conclusion

The installation of a commercial RO plant is a crucial step in creating a dependable water treatment unit that can be used in commercial buildings and industrial facilities. From the site study to the final test, performance and safe water output stay smooth and reliable. With proper planning and execution, long-term efficiency and minimization of operational problems can be achieved.

For businesses aiming for a consistent water supply, it’s crucial to emphasize correct installation practices and expert advice. Netsol Water offers complete support for designing and installing RO systems for advanced usage in different industries. Contact us today to request a consultation and get a water solution and expert advice on commercial RO plant installation steps, to ensure you have a system that works for you.

Contact Netsol Water at:

Phone: +91-9650608473

Email: enquiry@netsolwater.com


Can-Commercial-RO-Plant-Treat-Seawater.webp

July 18, 2026by Netsol Water

Can Commercial RO Plant Treat Seawater?

In coastal areas, water is a key ingredient of various industries and everyday life. Low availability of fresh water is a serious issue in coastal cities. When seawater is available, it cannot be used as is, because of the impurities and salt that it contains. For industries in coastal regions such as Gujarat, Tamil Nadu, and other coastal areas of India, the search for dependable water treatment solutions becomes important, aiming to transform seawater into potable water. This generates a high demand for knowledge on the ability of advanced treatment systems to treat such high-salinity water.

A large number of industries are looking for the answer to the question, “Can a commercial RO plant be used to treat seawater in a practical and economical manner?” The need for clean water is still increasing with the development of industrial activities in coastal areas. Under these circumstances, companies such as Netsol Water are top suppliers of water treatment solutions, which are helpful for industrial water applications. The use of a commercial RO system significantly contributes to salt and impurity removal; however, a better understanding of technology and system design is needed for seawater treatment.

Seawater Treatment in Commercial RO Systems

It is crucial to understand the interaction between seawater and reverse osmosis systems before assessing performance. Seawater is saltier and has more minerals dissolved in it, making it unsuitable for direct use. The commercial RO system works with high pressure and special membranes to isolate clean water from dissolved solids. But seawater treatment is not so easy due to its high salinity.

1. High-Pressure Requirement for Seawater Filtration

Seawater requires much more pressure than normal groundwater or surface water. This is because there is high resistance to membrane filtration due to the salt concentration. The commercial RO system used for seawater needs to have high enough pressure to force water through special membranes. This pressure is necessary to effectively separate the salt in the system. A continuous flow with stable filtration is maintained by means of high-pressure pumps. This increases the energy requirement of the seawater treatment process, but it is possible with proper system design. Pressure control in a continuous process is crucial to process efficiency.

2. Special Membranes for Salt Removal

Another important factor is the use of seawater-grade RO membranes. These membranes are specially manufactured for greater salt and pressure resistance. They are used to desalinate seawater to produce potable water. Such high salt content could damage standard membranes in a short amount of time. These seawater membranes are designed to have a longer lifetime in extreme conditions and to maintain filtration performance. This is particularly important for industries that rely on coastal water supplies. Choosing the right membranes is crucial for the effective treatment of seawater in a real industrial setting.

Role of Pretreatment in Seawater RO Systems

Pretreatment is a key factor in improving the quality of seawater for reverse osmosis filtration. If not pretreated appropriately, the RO system can suffer from frequent damage and inefficiency. Suspended particles, organic matter, and microorganisms in the seawater have to be removed before reaching the RO membrane. Let’s take a look at some of the important pretreatment processes that can make the system more effective and help a commercial RO plant treat seawater.

1. Filtration and Sediment Removal

The first step in pretreatment is to eliminate sand, dust, and suspended particles in seawater. This is achieved by using filtration systems which ensure that RO membranes do not clog. Unless these particles are removed, they can clog the water flow and make the system less efficient. Good sediment removal provides smooth operation and minimises maintenance requirements. It also helps improve the lifespan of the membrane system by reducing physical damage. This is critical to ensure constant water quality production in commercial systems.

2. Chemical Treatment for Organic Control

Seawater may contain organic matter and biological growth which may impact the membranes’ performance. These impurities are controlled by chemical treatment prior to the water entering the RO unit. This helps inhibit biological fouling and scaling inside the system. It also helps enhance water quality and keep the process in stable operation for long periods of time. The chemical dosing should be optimized to prevent damage to membranes and to be effective in purification. This is an important step to make seawater suitable for the commercial RO process.

Efficiency and Limitations of Commercial RO for Seawater

It is essential to understand the efficiency of the system when assessing seawater treatment systems. A commercial RO system can be used to treat seawater, but there are some disadvantages. These restrictions are primarily connected with energy consumption and maintenance requirements. Let’s take a look at some of the key considerations that make a commercial RO plant suitable, and difficult, for the desalination of seawater for industrial use.

Maintenance and System Durability

The components of seawater are extremely corrosive and can impact system life in the long term. The system must be maintained regularly in order to keep it running smoothly. Depending on usage, membranes must be cleaned and replaced periodically. Maintenance activities help ensure long-term performance and minimize system breakdowns. A clean system can run efficiently for many years even in harsh seawater environments. This shows how crucial service support is for commercial installations.

Industrial RO Systems Using Seawater

Industries in coastal areas have widely used seawater RO systems. These systems assist industries in coping with water scarcity and aid in their operational requirements. Let’s take a look at some of the important applications where treating seawater with a commercial RO plant is an effective solution to industrial requirements.

1. Energy Generation and Production Facilities

Cooling and production processes in power plants and large manufacturing units require a continuous supply of water. Seawater RO systems contribute to this need by converting seawater into potable water. This saves on freshwater consumption and promotes sustainability. These industries are the ones most affected by stable water availability, which allows production to be carried out more efficiently.

2. Coastal Hotels and Resorts

Coastal hotels and resorts rely on seawater treatment systems as well. They need clean water to serve their guests and for their daily activities. RO systems can be used to make seawater potable for general use. This means good hospitality services even in regions with limited freshwater. It also lowers the expenses of transporting water.

Read some interesting information for the Commercial RO Plant Manufacturer

Conclusion

A commercial RO plant can treat seawater effectively if it is designed with the correct technology and the right pretreatment system. It can turn high-salinity water into potable water for industry and commerce. It also needs high pressure and regular maintenance over time to work efficiently. Knowing these factors can help industries make informed decisions prior to installation.

Expert support makes final decision-making easier. So if you are looking to know more about whether a commercial RO plant can treat seawater, or need guidance to select the right RO plant, Netsol Water is the trusted partner you can turn to. Call our staff for professional advice and quality industrial water treatment systems.

Contact Netsol Water at:

Phone: +91-9650608473

Email: enquiry@netsolwater.com