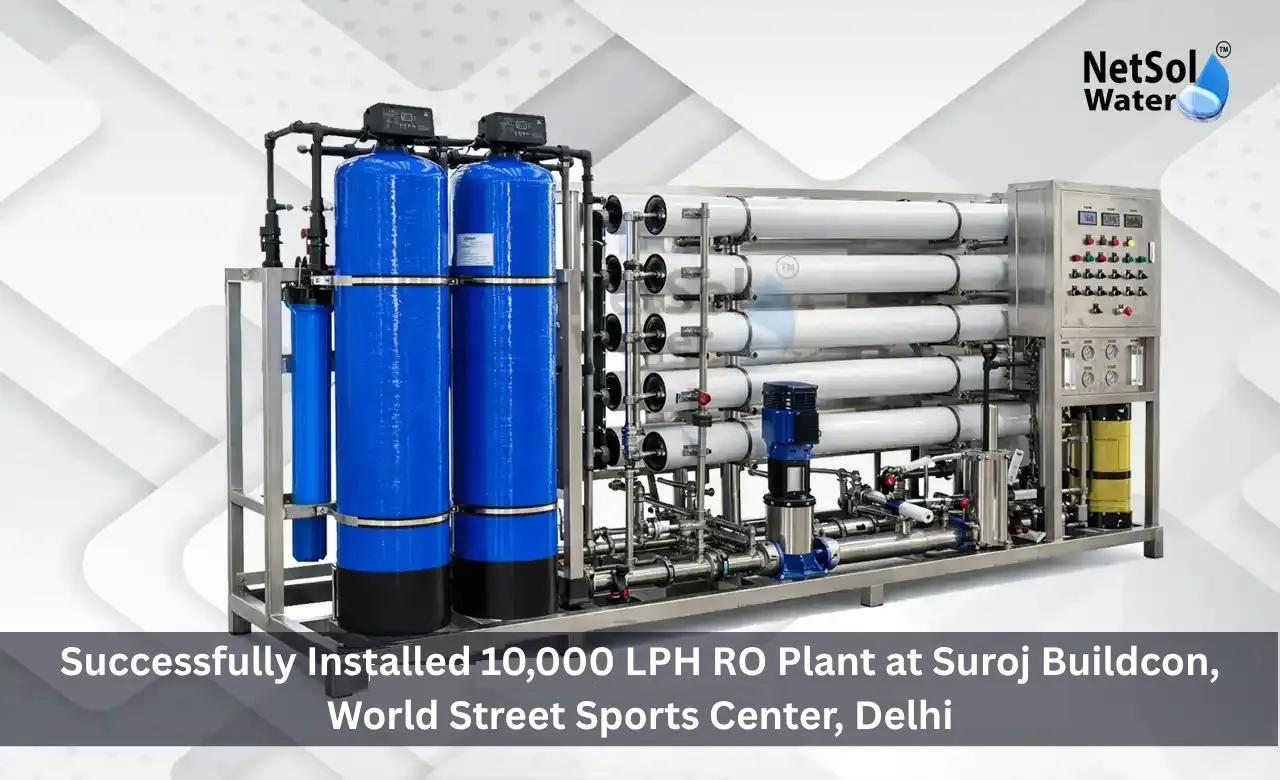
Water is one of the essential needs to be met for all businesses. Hotels, restaurants, hospitals, schools, offices, factories, and numerous other commercial properties require fresh water on a daily basis. Safe water enables the working process and also will help the well-being of employees, customers, and visitors. A quality water treatment plant will remove impurities and enhance the taste and quality of water. That’s why it is important for every organization to make a correct choice when buying a commercial water purifier.
A commercial RO plant manufacturer guides businesses to choose plants suitable for their water quality and usage requirements. We are the best commercial RO plant manufacturer with unique and high-quality water purification solutions for various industries. The water requirements vary from one business to another. Some demand purified water for drinking purposes, and some demand purified water for production processes.
Why Choosing the Right Commercial Water Purifier Matters
Clean water is important for the proper functioning of all commercial enterprises. Water quality impacts the health of employees, customer satisfaction, equipment life, and product quality. A poor water purification system can lead to numerous issues, including frequent maintenance, high operating costs, and poor water quality. Therefore, the selection process is very significant. Let’s take a look at some important factors that explain why it is important to choose the right commercial water purifiers.
1. Water Quality Requirements
The quality of the water received at the business is the first thing every business needs to know. Different sources of water have different contaminants. The water can have an excessive amount of dissolved salts and/or high amounts of iron, bacteria, or particulate matter. It’s a good idea to test the water before buying a purifier so you can determine exactly what treatment is needed. A commercial RO system can eliminate dissolved salts, heavy metals, and many other harmful contaminants. In this process, clean water with commercial requirements is obtained. The system operates more efficiently and more effectively when it is in balance with the water quality. It also helps minimize the cost of repairs that are not necessary and helps improve the efficiency.
2. Daily Water Demand
Every business uses a different quantity of water each day. A restaurant might need many hundreds of litres, while a manufacturing unit can need several thousand liters. Selecting a purifier of the right capacity helps to avoid a shortage of water in the peak hour. If the system is undersized, it does not satisfy the demand; if it is oversized, it will raise the investment and operating cost. If the RO plant is designed correctly, there won’t be any waste of energy or water by having a continuous water supply. This equilibrium enhances the business operations and helps in maintaining smooth operations in the daily activities.
Features That Make a Commercial Water Purifier the Best Choice
A commercial water purifier’s size is not the only feature that matters for its quality. Many functions have been incorporated in modern treatment plants that enhance the performance and decrease maintenance. Having knowledge of these features will aid the decision-making of the businesses before investing. Let’s take a look at some of the important features that every commercial water purifier should provide.
1. Advanced Reverse Osmosis Technology
RO is one of the most successful water purification techniques in commercial use. Water is pushed across a unique membrane that filters out the dissolved salts, chemicals, heavy metals, and many impurities. This yields clean and safe water to be used for drinking, cooking, manufacturing, and other commercial purposes. The water that is produced by the use of advanced RO technology is also better-tasting and causes less scaling in RO equipment. Improved water quality extends machine life and protects machines. It also helps to lower maintenance costs and promotes overall effective business performance in the year.
2. Strong Construction and Easy Maintenance
Commercial water purification systems run for extended periods of time every day. Thus, durable construction is an important feature. Quality stainless steel frames, corrosion-resistant parts, and reliable pumps increase system life. Easy maintenance is also a crucial feature, as the machine needs to be cleaned regularly for it to function properly. Easy filter replacement and easy-to-access components minimize downtime and service expenses. The well-designed purifier helps to save time and helps the businesses to operate without any kind of disruptions frequently. The durability and ease of maintenance provide commercial users with value.
How to Choose the Best Commercial RO Plant Manufacturer
The quality of the purifier depends not only on the equipment but also on the company that designs and installs it. An experienced manufacturer provides proper guidance before and after installation. This support helps businesses achieve better performance from their investment. Let us have a look at some important qualities that should be considered while selecting a manufacturer.
1. Experience and Technical Knowledge
A company with years of experience understands different water treatment challenges. It studies water quality, daily consumption, and available space before recommending a suitable solution. Experienced engineers design systems that match the customer’s exact requirements. They also ensure proper installation and testing before the plant begins operation. Technical knowledge helps solve problems quickly and improves system performance over time. Businesses receive dependable solutions that continue to deliver safe water every day.
2. Service Support and Customer Assistance
Good service support is one of the biggest advantages of choosing a trusted manufacturer. Commercial RO plants require regular maintenance, inspections, and timely replacement of filters and membranes. A company that offers quick technical support prevents long shutdowns and protects business operations. Customer assistance also includes operator training and guidance for proper system use. These services increase equipment life and improve purification efficiency. A dependable manufacturer remains available whenever customers need help, which builds long-term confidence and satisfaction.
Selecting the best commercial water purifier requires careful planning and a clear understanding of water quality, daily demand, and long-term operating needs. A properly designed RO system provides safe water, improves equipment life, and supports uninterrupted business operations. Working with an experienced commercial RO plant manufacturer ensures that every part of the purification process meets commercial requirements.
Netsol Water is the leading commercial RO plant manufacturer that delivers reliable water treatment solutions for businesses across different industries. If you are planning to install a commercial water treatment plant or upgrade an existing one, you can contact the experienced team at Netsol Water for expert guidance and a customized solution that matches your business needs.
One of the most essential demands of all homes and businesses is clean water. Water is consumed daily by people for drinking, cooking, cleaning, and a variety of industrial processes. Poor water quality can impact health, equipment, and work activities. That’s why many people go for an RO system, as it lowers out the impurities in water, thus enhancing its quality. A decent RO system delivers safe water and additionally secures machines that use water on a regular basis.
An experienced RO plant manufacturer will be able to design an RO Plant that will suit various water conditions and customer needs. We are a premier RO plant manufacturer providing trusted solutions to industries, commercial, and domestic water bodies. It is important to have a better understanding of the advantages that an RO system has, and how it works, before choosing any water treatment plant.
Enhanced Water Quality Enhances Daily Living
Water quality is the basis for good health and efficient industrial processes. Water can be clear and still contain dissolved salts that contain harmful chemicals, bacteria, and contaminants. These unwanted substances may alter the taste and odour of water and can potentially have impacts on health in the long term. An RO plant can eliminate many such impurities and give clearer water that can be used for various purposes. Let’s take a look at some important ways that better water quality enhances life.
1. Removes Harmful Impurities
One of the greatest benefits of the RO plant is that it can be used to remove unwanted contaminants from water. The special membrane within the system removes dissolved salts, heavy metals, and most harmful particles. This procedure renders water much safer for drinking and cooking. Fresh water is available each day, so families will not have to worry about common impurities. If the firm is manufacturing products that require clean water, the consistency in water quality also improves the quality of the product.
2. Enhances the Taste and Smell
Excess minerals and/or organic matter in the water often give it an unpleasant taste or smell when it is chlorinated. However, many people don’t want to consume such water because it does not taste fresh. An RO system can filter out these unwanted substances and enhance the quality of water. The smell of fresh-tasting water will make people more inclined to drink water and help them stay hydrated. It also enhances the taste of tea, coffee, juices, and cooked food, as ingredients are loaded to cleaner water.
Safeguards Equipment and Minimizes Maintenance Costs
Water is required daily in many machines in homes, commercial buildings, and industries. Minerals are a common issue in poor-quality water that can accumulate in pipes, boilers, cooling towers, and production equipment. These deposits cause inefficiency and maintenance issues. An RO system can address this issue by providing better water, which may be water with fewer dissolved minerals. Let’s take a look at a few essential reasons why an RO system helps to safeguard equipment and minimize maintenance costs.
1. Prevents Scale Formation
Hard water is water that has minerals, such as calcium and magnesium, that form scale in the equipment. This deposit over time prevents water from flowing and decreases heating efficiency. Machines then use more energy and have to be fixed more often. An RO plant filters out most of these minerals prior to reaching the RO equipment. This results in a cleaner, more efficient system for a longer period.
2. Increases Equipment Life
The equipment used in industries and houses is a significant investment. Every owner desires such systems to run for many years without any unforeseen failures. Clean water minimises wear in the pump’s pipeline and other components. Fewer mineral deposits also minimize moving parts’ stress. This enables equipment to run efficiently and reduces the replacement cost. Operating businesses can be done without constant stoppages, resulting in increased overall productivity.
Saves Money and Contributes towards Sustainability
People believe that an RO system is just about clean drinking water, but it can also help save cash in the long run. Improved water quality leads to fewer unnecessary costs and the responsible use of natural resources. As water treatment efficiency increases, people also lower their waste and boost environmental protection. So, let’s take a look at some of the significant environmental and financial advantages of having an RO plant.
1. Lowers Operating Costs
Clean water equipment typically requires less energy input because it does not have a significant scale build-up within the equipment. This also decreases maintenance costs, and thus repair costs. Companies will save on replacement costs for any damaged parts and prevent lost production time due to equipment failure. This also helps homes, as appliances like water heaters and washing machines can be used effectively for a longer period. These savings can usually offset the upfront costs of investing in the RO plant.
2. Reduces Plastic Waste
A large number of families buy bottled water as a result of not being content with the quality of the tap water. This only adds to the waste of plastic and the monthly cost. A RO water filter system is a process that generates potable water immediately at the location. Families can top off reusable water bottles rather than purchasing water in bottles over and over again. It is an easy modification that will help to cut down on the waste of plastic, enhance the cleanliness of the environment, and cut costs.
Suitable for Homes, Commercial Buildings, and Industries
Each user has their own desired water quality. Safe drinking water can be needed by a family, and purified water can be needed by an industry. An RO plant is very useful for various applications due to its flexibility. Various options of modern systems exist with the capacity and design as per the needs. Let’s take a quick look at some common applications in which RO plants work very well.
1. Domestic Applications
RO systems are installed in homes to ensure the drinking water is of better quality and to keep their families safe. The system filters out the unwanted impurities and ensures the availability of fresh water for the preparation of beverages, for cooking, and for daily use. Children, particularly, and older family members benefit the most from clean water, as it promotes a healthy lifestyle. Home systems are also simple to operate and can only be maintained routinely for consistent performance.
2. Commercial and Industrial Applications
Restaurants, hotels, hospitals, schools, laboratories, and manufacturing industries all require dependable water quality. Many production processes cannot deliver consistent results without purified water. An experienced industrial RO plant manufacturer designs plants according to water quality and daily demand. This ensures smooth operation and better efficiency across different industries. Businesses also improve customer satisfaction because they use cleaner water in their services and products.
Clean water supports better health, protects valuable equipment, and improves daily life. An RO system offers a practical solution for removing unwanted impurities while reducing maintenance costs and improving efficiency. It also helps save money over time and supports environmental protection by reducing plastic waste. Choosing the right system is important because every water source has different treatment needs.
Working with a trusted RO plant manufacturer ensures that the system performs efficiently and delivers long-lasting results. Netsol Water is the leading RO plant manufacturer that provides reliable water treatment solutions for homes, commercial buildings, and industries. If you are planning to install an RO plant or upgrade your existing water treatment setup, you can contact the experienced team at Netsol Water for professional guidance and the right solution for your requirements.
Clean water is one of the basic needs of every home and every industry. As the demand for safe water continues to grow, many sectors now use advanced purification methods to improve water quality. RO is one of the most trusted technologies because it removes dissolved salts, harmful chemicals, and many other impurities from water. This process makes water suitable for drinking, industrial use, and many other purposes. A trusted RO plant manufacturer helps businesses and institutions install plants that match their water quality needs and production requirements. We are the leading commercialRO plant manufacturer that provides advanced solutions for different industries with a strong focus on quality and performance. Understanding the applications of RO helps people choose the right treatment system for their needs.
Applications of RO in Domestic and Commercial Water Supply
The use of RO technology has become very important in homes and commercial places because clean water is necessary for daily life. Water from different sources often contains dissolved salts, bacteria, chemicals, and other unwanted substances. RO plants improve water quality and make it safer for drinking, cooking, and other daily activities. As the need for clean water increases, more people are choosing RO systems for regular use. Let us have a look at some important applications of RO in domestic and commercial water supply.
1. Residential Water Purification
RO plants are being installed in various cities and towns to enhance the quality of drinking water in homes. High levels of dissolved salts that adversely influence taste and safety are present in many areas. An RO plant purifies these impurities and gives the whole family pure drinking water. Additionally, it decreases the chance of health issues that can come from polluted water. Many people prefer to install RO plants at home, as they help them to save the expense of buying bottled water and also provide long-term benefits.
2. Hotels, Restaurants, and Office Buildings
Clean water is needed daily, day in and day out, in hotels, restaurants, and office buildings. Drinking, cooking, and cleaning water is supplied to customers. RO plants contribute to the maintenance of water quality and also increase customer satisfaction. They also safeguard the equipment in the kitchen from scaling due to hard water. A professional RO Plant Manufacturer creates particular designs that suit the daily water requirement of business buildings and aids them to function without ever being interrupted.
Applications of RO in Industrial Manufacturing
High-quality water is required by industries, as many manufacturing processes require clean and stable water conditions. Low-quality water can cause equipment damage, affect product quality, and increase maintenance expense. RO technology answers these problems with purified water at industrial water quality. There are different types of RO plants that are used in different industries based on the requirement of production. Let us look at some significant industrial applications of RO technology.
1. Food and Beverage Industry
Pure water is required by the food and beverage industry to make safe and consistent-quality products. Washing, mixing, and cleaning equipment are processed with water. RO plants can be used to selectively remove minerals and contaminants that could impact the taste or quality of the food product. This is especially helpful for manufacturers to adhere to food safety regulations and maintain product standards. Clean water also helps to make production processes more efficient and can decrease the risk of contamination.
2. Pharmaceutical and Chemical Industry
Highly purified water is used in the manufacture of medicines and healthcare products by pharmaceutical companies. Product quality and safety can be impacted even with a minor contamination. RO water systems produce water of high purity quality, which is essential for manufacturing. RO-treated water is also used in various manufacturing units in the chemical industry, as it ensures consistency and a reduction in impurities. A good water treatment system helps achieve better-quality products and smooth operations.
RO Uses in Healthcare and Educational Institutions
Healthcare and educational facilities have a high volume of visitors on a daily basis. Clean water is required for medical uses, sanitation, and drinking in these locations. RO technology assists in keeping water safe and assists in daily operations. Good treatment of water also assists in improving hygiene and public health. Let us have a look at some important applications in these sectors.
1. Healthcare facilities and hospitals
Purified water is needed for patient laboratories, dialysis units, and medical equipment in hospitals. Access to clean water helps to prevent infections and facilitate proper medical care. These also prevent mineral deposits and scaling on costly health care equipment. This prolongs the life of equipment and minimizes maintenance expenses. Water treatment plays a crucial role in the functionality of hospitals; they rely on it to provide excellent healthcare.
2. Schools, Colleges, and Research Laboratories
Schools require clean water for different purposes such as the hostel, students, teachers, laboratories, and other uses. RO systems deliver safe drinking water and improve the health of all on campus. Water is also needed for purification of water systems used in research laboratories for experiments and testing procedures. Good water quality ensures accurate scientific work and reduces chances for contamination to occur. Reliable and efficient water treatment systems provide the schools with water for their daily needs.
Applications of RO in Agriculture and Environmental Protection
RO technology is also useful in the field of agriculture and environmental management. Water quality has a direct influence on crop production, irrigation systems, and the environment. Purified water improves agricultural practices and minimizes the environmental footprint. Let’s take a look at some of the important applications in these areas.
1. Agriculture and Irrigation
Saline or poor-quality water is an issue for many farming areas. Before irrigation, Irrigation Water Quality (IWQ) is improved by RO systems, which remove excessive salts. High-quality irrigation water helps to improve crop growth and productivity. Farmers can also minimize the damage to soil by over-accumulating minerals. Better water quality equals better crops and sustainability.
2. Wastewater Reuse and Environmental Conservation
Nowadays, industries and municipalities target recycling water in order to decrease the amount of freshwater used. The RO technology processes the wastewater and allows it to be used for irrigation, cleaning, and industrial processes. This will help alleviate stress on water resources and help preserve the environment. Water recycling also reduces operating costs and assists industries in complying with environmental restrictions. Netsol Water provides novel RO solutions to aid in responsible water management and sustainable development.
RO technology has become an important part of modern water treatment because it provides safe and purified water for homes, businesses, industries, hospitals, farms, and many other sectors. Every application shows how clean water improves health, production quality, and operational efficiency. Choosing an experienced RO plant manufacturer ensures that every system performs according to the required standards and delivers long-lasting results.
Netsol Water is the leading RO plant manufacturer that offers dependable RO solutions for different water treatment needs. If you want to install an RO plant or need expert guidance for your project, you can contact Netsol Water for professional consultation and the right solution for your water purification requirements.
Clean water supports every business that depends on production quality and smooth daily operations. Industries such as food processing, pharmaceuticals, hotels, hospitals, and manufacturing units need a dependable water treatment system to maintain product quality and protect equipment. A commercial RO plant removes dissolved salts, harmful minerals, and other unwanted particles from water. This process helps businesses receive safe water for different industrial and commercial uses.
India is known for its fast industrial growth and increasing demand for water treatment systems. As more businesses expand, they need reliable water purification solutions that can handle different water sources. Installing a commercial RO plant in the right way helps the system perform well for many years. It also lowers maintenance needs and improves water quality. We are the leading commercial RO plant manufacturer that designs and installs quality systems for different industries. Understanding the installation process helps every business make better decisions and achieve the best results from its investment.
Site Preparation Before Installation
Every successful installation begins with proper planning. A well-prepared site helps the commercial RO plant perform without interruption. It also prevents future operating problems. Let us have a look at some important aspects of site preparation.
1. Selecting the Right Installation Location
The first step is choosing a suitable place for the plant. The location should provide enough space for the RO system and allow operators to move around easily during inspection and maintenance. The floor should remain strong and level so that it supports the full weight of the equipment. The area should stay clean and protected from direct sunlight, heavy rain, and excessive dust. Good ventilation also helps maintain the proper working condition of electrical parts and pumps.
2. Arranging Utility Connections
The next requirement is preparing all utility connections before installation starts. The plant needs a stable electricity supply along with proper water inlet and outlet connections. A suitable drainage line should also be available because the RO process releases reject water during operation. When these facilities remain ready in advance, the installation team can complete the work smoothly without unnecessary delays.
Installing the Main Components of the RO Plant
Correct installation of every component allows the plant to deliver high-quality water. Each part works together to complete the purification process. Proper positioning and secure connections improve system efficiency and increase equipment life. Let us have a look at some important stages of installing the main components.
1. Installing the Pretreatment System
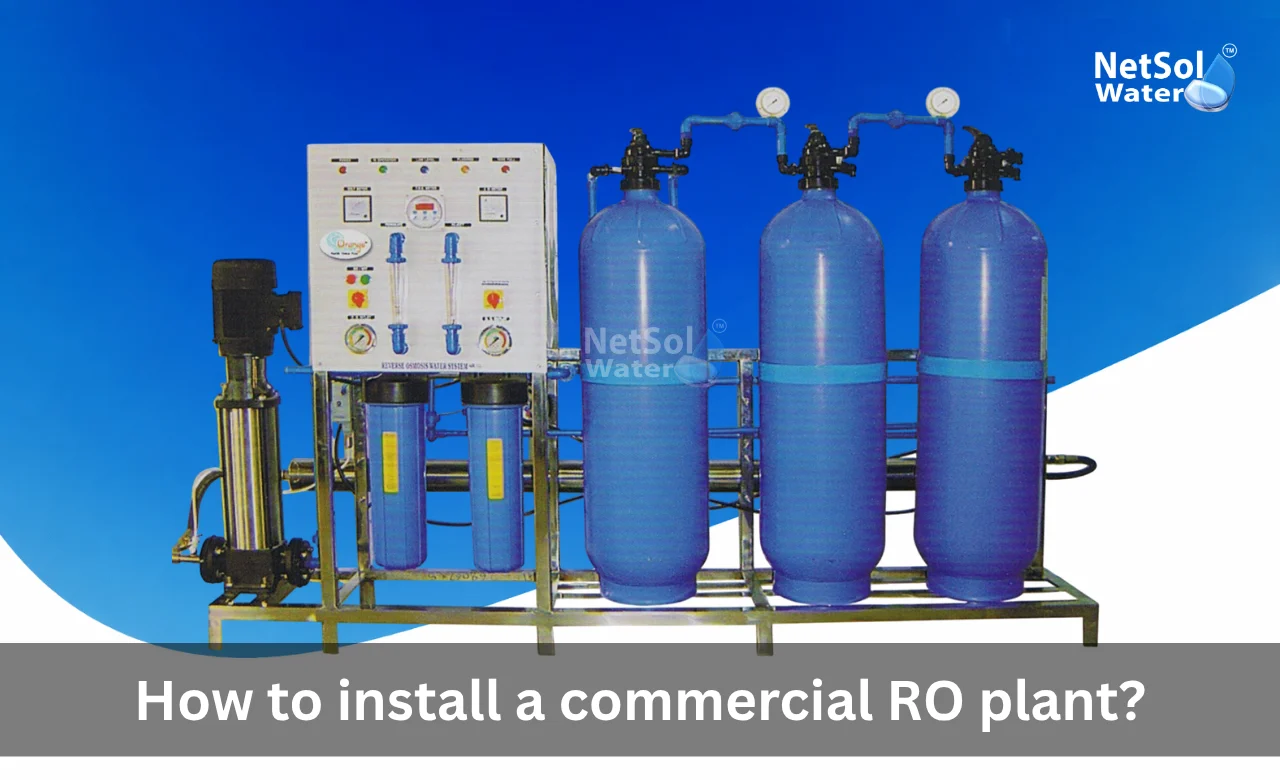
Pretreatment protects the RO membranes from damage. This stage removes suspended particles, chlorine, hardness, and other impurities before water enters the membranes. Sand filters, activated carbon filters, and water softeners should be installed according to the system design. Every unit must connect properly to maintain steady water flow. Good pretreatment improves membrane life and keeps the purification process stable for a longer period.
2. Installing RO Membranes and Pressure Vessels
RO membranes form the heart of the complete system. The installation team places the membranes carefully inside pressure vessels according to the manufacturer’s instructions. Proper sealing prevents leakage and supports smooth water movement through the membranes. Pressure vessels should remain firmly fixed to avoid vibration during operation. Correct installation ensures that the system removes dissolved impurities with high efficiency.
3. Connecting Pumps and Piping
High-pressure pumps move water through the complete purification process. These pumps should be installed securely to maintain stable pressure during operation. The piping network should connect all units without leakage. Every joint must remain tight because even a small leak can affect system performance. Proper pipe alignment also helps maintain smooth water flow throughout the plant.
Electrical Connection and System Testing
Electrical installation and performance testing confirm that the commercial RO plant operates safely and efficiently. This stage ensures that every part works according to the design before regular operation begins. Let us have a look at some important activities performed during this phase.
1. Completing Electrical Installation
Qualified professionals should complete all electrical work. The control panel should connect correctly with pumps, sensors, and other electrical equipment. Proper earthing protects both the equipment and plant operators from electrical hazards. All wiring should follow recommended safety standards. A stable electrical supply helps maintain smooth plant performance and prevents unexpected shutdowns.
2. Testing System Performance
After completing installation, the entire system should undergo detailed testing. The installation team checks water pressure, flow rate, and water quality at different stages. They inspect every connection for possible leakage and verify that all valves function correctly. The team also measures the quality of purified water to confirm that the plant meets the required standards. Careful testing helps identify small issues before the plant begins regular production.
Commissioning and Operator Training
The final stage prepares the plant for long-term operation. Proper commissioning ensures that every system performs according to design. At the same time, operator training allows staff members to manage daily operations with confidence. Let us have a look at some important activities completed during commissioning.
1. Starting the Plant for Regular Operation
Commissioning begins with gradual startup of the complete system. The installation team monitors pressure, water recovery, and membrane performance during the first operating cycles. They make necessary adjustments whenever required. This careful approach allows the plant to reach stable operating conditions while protecting sensitive components from sudden pressure changes.
2. Training Plant Operators
Operator training remains equally important after installation. Staff members learn how to start and stop the system safely. They also understand routine inspections, filter replacement, membrane cleaning, and basic troubleshooting methods. Proper training allows operators to identify small problems early before they become major repairs. Regular maintenance performed by trained operators keeps the system running efficiently and extends the life of every component.
Proper installation creates the foundation for dependable water treatment and long service life. Every stage, from site preparation to commissioning, plays an important role in achieving stable performance and consistent water quality. Careful planning, professional installation, and regular maintenance help businesses receive the full benefit of their investment.
Choosing an experienced commercial RO plant manufacturer also ensures expert guidance throughout the installation process and beyond. Netsol Water is a trusted commercial RO plant manufacturer that delivers complete solutions for different industries with quality products and professional support. If you are planning to install a commercial RO system or need expert advice, contact Netsol Water today to request a consultation and find the right solution for your water treatment needs.
India has become one of the fastest-growing markets for water treatment because industries and cities need clean water every day. The country is famous for its large manufacturing sector and its strong demand for advanced water treatment plants. As industries expand and the population grows, clean water has become more important than ever before. This growing need has also increased the demand for high-quality RO membranes that can remove dissolved salts, impurities, and harmful substances from water.
Choosing the right membrane manufacturer helps industries improve water quality and keep treatment plants working for a long time. A trusted manufacturer also provides technical support and products that meet different treatment needs. Among the companies working in this field, we have built a strong name as a leading RO membrane manufacturer in India. The company offers dependable membrane solutions for industrial, commercial, and municipal applications. Understanding what makes a manufacturer dependable helps businesses make the right investment for long-term water treatment success.
Importance of Choosing the Right RO Membrane Manufacturer
Selecting the right manufacturer is the first step toward building an efficient water treatment system. Every RO membrane performs an important job because it removes unwanted particles and produces clean water. A good manufacturer not only supplies quality products but also supports customers throughout the life of the system. Let us have a look at some important factors that help identify a dependable manufacturer.
1. Quality Standards and Manufacturing Process
A trusted manufacturer follows strict quality standards during production. Every membrane goes through several testing stages before reaching customers. This process ensures that each membrane performs well under different operating conditions. High-quality raw materials also improve membrane strength and increase its working life. A company that focuses on quality delivers products that maintain stable performance for a longer period. This gives industries confidence in their investment and helps them achieve consistent water purification results.
2. Technical Support and Product Range
Manufacturers should also provide strong technical guidance after the sale. Different industries need different membrane sizes and performance levels. A dependable company understands these requirements and recommends suitable products. Good technical support helps customers install membranes correctly and maintain them in the right way. This support also prevents unnecessary operational problems. A wide product range allows industries to select membranes that match their treatment capacity and water quality requirements without difficulty.
Why Netsol Water Is the Leading RO Membrane Manufacturer in India
Many companies manufacture RO membranes in India, but only a few have earned customer trust through consistent quality and service. Experience, innovation, and customer satisfaction make a significant difference when selecting a manufacturer. Let us have a look at some reasons why Netsol Water has become a preferred choice for many industries.
1. Advanced Manufacturing and Quality Assurance
Netsol Water follows advanced manufacturing methods to produce high-performance RO membranes. The company uses modern production techniques and carefully selected materials to ensure dependable results. Every membrane passes through detailed quality inspections before delivery. These inspections help maintain product consistency and improve customer confidence. The company continues to improve its manufacturing process so customers receive products that perform efficiently under different operating conditions. This commitment to quality has helped the company build a strong reputation across India.
2. Wide Industry Applications and Customer Support
Netsol Water serves many industries, including food processing, pharmaceuticals, textiles, hospitals, hotels, and commercial buildings. Each industry has different water treatment needs, and the company provides suitable membrane solutions for every application. The experienced technical team helps customers choose the right membrane according to feed water quality and production requirements. The company also offers guidance during installation, maintenance, and replacement. This complete support allows customers to operate their systems smoothly and improve overall plant performance. Because of this customer-focused approach, Netsol Water is widely recognised as a leading RO membrane manufacturer in India.
Applications of RO Membranes across Different Industries
RO membranes are used in many industries because clean water supports both production and environmental protection. Every industry has different treatment goals, but all of them require efficient water purification. Let us have a look at some major industries where RO membranes play an important role.
1. Industrial Water Treatment
Water is used up extensively in manufacturing industries on a daily basis. Salts and impurities in the water can cause equipment problems and reduce the quality of the product. These undesirable components are rejected by RO membranes and result in clean process water. RO units are employed in industries like power plants, chemical plants, and textile factories to enhance efficiency and to prevent damage to costly machinery. Correct water treatment also ensures that industries are compliant with environmental legislation and will enhance the performance of their operations in the long term.
2. Commercial and Municipal Applications
RO membranes are also used in commercial buildings such as hotels, hospitals, schools, and municipal water treatment plants for clean water production. Clean water is vital for people’s health and well-being. RO systems are used by municipal authorities to treat water prior to its distribution. RO plants are also installed in commercial facilities to ensure that the employees, customers, and guests have safe water. Membranes are reliable, and they allow for continuous operation with uniform water quality throughout treatment.
How to Select the Best RO Membrane Manufacturer in India
Each project will be different, and the choice of manufacturer needs to be carefully considered. When selecting a product, buyers will want to look at the quality of the product, as well as their service experience and long-term support. Let us check some of the important points that assist in the selection process.
1. Experience and Product Performance
A knowledgeable manufacturer knows the various water treatment problems and creates solutions to address them appropriately. Having years of experience, the companies still strive to enhance their membrane technology to meet customer demands and industry advancements. When the product has proven performance, buyers know that it is reliable and can be confident when it is installed. Performance records should always be taken into consideration by customers when buying RO membranes.
2. Service Network and Long-Term Value
A robust service network helps to deliver high customer satisfaction, as technical support is available when required. Quick response helps minimise interruptions and keeps treatment plants running. The overall value is another factor to take into account, not just the price tag. Maintenance and replacement costs are reduced in the long term with a high-quality membrane, due to its longer life and better performance. It’s better to deal with a reliable RO membrane manufacturer in India than to opt for products due to their low prices.
Choosing the correct membrane manufacturer is an important part of ensuring that you have clean water and an efficient plant operation. Long-term success comes from product quality, manufacturing standards, technical support, as well as industry experience. These should be carefully considered before a business invests in a system, as they will lead to higher efficiency in operation and a longer lifespan of the treatment plant.
Netsol Water has established a good reputation by offering quality products, reliable service, and customer-centric solutions. Netsol Water, as a trusted RO membrane manufacturer in India, can help you get expert advice and an appropriate RO membrane solution to address your water treatment requirements. The professional team will ensure that you select the most suitable product and offer you support with your project from beginning to end.
Reverse Osmosis or RO technology has become one of the most trusted methods for water purification. It removes dissolved salts along with harmful chemicals and many unwanted particles from water. The quality of an RO plant depends greatly on the membrane because it performs the main filtration process. A good membrane gives clean water for a long time and also improves the overall performance of the system.
Many industries and commercial facilities use RO plants every day to meet their water needs. Since different applications require different water quality, there is no single membrane that suits every situation. The right choice depends on the source of water and the desired output. A trusted RO membrane manufacturer helps users select the correct membrane according to their needs. We are the leading RO membrane manufacturer that provides dependable membrane solutions for industrial and commercial applications with a strong focus on quality and long service life.
Different Types of RO Membranes
Choosing the correct membrane starts with knowing the available options. Every membrane has a different design and serves a specific purpose. A proper understanding helps users select a membrane that delivers better performance and longer service life. Let us have a look at some common types of RO membranes and understand how each one works.
1. Thin Film Composite Membrane
Thin Film Composite or TFC membranes are the most widely used membranes in modern RO plants. They offer excellent salt rejection and produce high-quality purified water. These membranes perform well in industrial plants, commercial buildings, and water treatment facilities. They also provide a higher water flow while maintaining good filtration efficiency.
TFC membranes require proper pre-treatment because chlorine can damage their surface. When users protect them with suitable filters, they deliver excellent performance for many years. Their high efficiency and consistent results make them the preferred choice for many industries.
2. Cellulose Triacetate Membrane
Cellulose Triacetate or CTA membranes work well in water that contains small amounts of chlorine. They naturally resist chlorine damage better than TFC membranes. However, they generally provide lower salt rejection and lower water production.
These membranes suit applications where chlorine removal before the RO system is difficult. They also perform well in systems that receive regular maintenance. Although they are less common today, some industries still use them because of their specific advantages.
3. Low Pressure RO Membranes
Low-pressure membranes operate efficiently while using less energy. They require lower operating pressure and help lower electricity costs. Many commercial facilities choose these membranes because they provide a balance between water quality and operating expenses.
They work best with water that has lower dissolved solids. When used under suitable conditions, they produce consistent results while keeping energy consumption under control.
Factors That Help You Choose the Best RO Membrane
Selecting an RO membrane involves more than comparing different products. Every water source has unique properties, and every application has different demands. Understanding these factors helps users make a better investment. Let us have a look at some important points that affect membrane selection.
1. Water Quality
The quality of feed water plays a major role in membrane selection. Water with high dissolved salts requires membranes that provide higher rejection rates. Water containing suspended particles or organic matter also needs proper pre-treatment before entering the RO system.
Testing the water before choosing a membrane helps avoid operational problems. It also increases membrane life and improves purification efficiency.
2. Flow Requirement
Different industries require different amounts of purified water every day. Small commercial buildings may need limited production, while manufacturing plants often require continuous high-volume output.
Selecting a membrane that matches the required flow prevents unnecessary pressure on the system. It also maintains steady water production without affecting quality.
3. Operating Conditions
Pressure, temperature, and system design also influence membrane performance. Some membranes perform better under high pressure, while others work efficiently at lower pressure.
Proper matching of operating conditions with membrane specifications improves system stability. It also lowers maintenance needs and extends membrane life.
Why Membrane Quality Matters for Long-Term Performance
Many users focus only on the purchase price while selecting a membrane. However, long-term performance depends much more on quality than on initial cost. A good membrane provides better efficiency and lower operating expenses throughout its life. Let us have a look at some reasons why membrane quality should always receive proper attention.
1. Better Water Purification
High-quality membranes remove dissolved salts, bacteria, and unwanted chemicals more effectively. This produces cleaner water that meets industrial and commercial requirements. Better purification also protects equipment used in later production processes.
Consistent water quality supports smooth operations and lowers the chances of product quality issues. This becomes especially important in food processing, pharmaceutical production, and manufacturing industries.
2. Longer Service Life
Well-manufactured membranes maintain their performance for a longer period when users operate them correctly. They resist fouling more effectively and tolerate regular cleaning procedures.
Longer membrane life lowers replacement frequency. This helps businesses save maintenance costs while improving plant productivity.
3. Lower Operating Costs
Efficient membranes require less energy to produce the same amount of purified water. Better filtration also lowers cleaning frequency and reduces system downtime.
Although premium membranes may cost more during purchase, they often save much more money during daily operation. This makes them a practical choice for long-term use.
Why Choose Netsol Water for RO Membranes
The success of an RO system depends not only on the membrane but also on the company that supplies it. A dependable manufacturer provides quality products along with technical support and guidance. Let us have a look at some reasons why many industries choose Netsol Water.
1. High Quality Manufacturing
Netsol Water follows strict quality standards while manufacturing RO membranes. Every membrane undergoes careful testing before reaching customers. This helps ensure reliable performance under different operating conditions.
The company develops membranes that suit industrial, commercial, and institutional applications. Customers receive products that deliver stable water quality and dependable operation.
2. Technical Guidance
Every application has different water conditions and production needs. Netsol Water studies these requirements before recommending the right membrane.
Proper guidance helps customers avoid incorrect selection. It also improves system efficiency and increases membrane life.
3. Complete Customer Support
Support continues even after installation. Netsol Water assists customers with maintenance advice, cleaning recommendations, and operational guidance whenever required.
This complete support helps customers maintain excellent system performance throughout the membrane life cycle.
Choosing the best RO membrane depends on water quality, operating conditions, production requirements, and long-term performance goals. A well-selected membrane delivers clean water, improves efficiency, and lowers operating costs over time. Product quality and expert guidance always make a significant difference in achieving dependable results.
If you are looking for a trusted RO Membrane Manufacturer that offers quality products and professional support, then Netsol Water is the right choice. As a leading RO Membrane Manufacturer, the company provides reliable membrane solutions for industrial and commercial applications. Contact Netsol Water today to discuss your water treatment needs or request a consultation to find the most suitable membrane for your system.
India has a fast-growing industrial sector that depends on clean water for daily production. Industries such as food processing, pharmaceuticals, chemicals, textiles, power plants, and manufacturing need pure water to maintain product quality and machine performance. This has increased the demand for high-quality RO membranes across the country. A good RO membrane helps remove unwanted salts, minerals, and impurities from water. It also improves the efficiency of the complete RO system and supports long-term operation.
Netsol Water has earned a strong name in this field because it provides dependable RO membranes and complete water treatment systems for different industries. As a leading Industrial RO Plant Manufacturer, the company delivers solutions that match the needs of many industrial applications.
Why RO Membrane Quality Matters
Every industrial RO system performs according to the quality of its membrane. A well-designed membrane improves water quality and keeps the complete treatment process stable for a long time. It also helps industries lower operating costs and maintain consistent production. Let us have a look at some important points that explain why RO membrane quality should always receive proper attention.
1. Better Water Purification
A high-quality RO membrane removes dissolved salts, bacteria, organic matter, and other unwanted particles from water. This process produces clean water that industries can use safely for production, cooling, and cleaning purposes. Good purification also protects equipment from scaling and unwanted deposits. As a result, industries enjoy smooth operations and better product quality.
2. Longer Membrane Life
A durable membrane continues to perform well for many years when industries follow proper maintenance practices. Strong membrane material resists wear and supports stable filtration even under demanding operating conditions. This helps companies avoid frequent replacements and lowers maintenance expenses over time.
3. Improved System Performance
The membrane controls the overall efficiency of the RO plant. When it works properly, the plant consumes less energy and delivers steady water output. Industries also experience fewer breakdowns, which saves both time and operating costs. This is why experienced companies always choose membranes from trusted manufacturers who understand industrial water treatment.
Which Company RO Membrane Is Best in India?
Many companies supply RO membranes in India, but only a few provide complete support from product selection to installation and maintenance. Choosing the right manufacturer is important because industries need more than just a membrane. They also require technical guidance, quality assurance, and dependable customer service. Let us have a look at some reasons why Netsol Water stands out in the Indian market.
1. High Quality Manufacturing Standards
Netsol Water follows strict quality standards while designing and supplying RO membranes for industrial applications. Every membrane undergoes careful testing before reaching customers. This process ensures stable performance, high rejection rates, and dependable water purification for different industries.
2. Complete Industrial Solutions
The company does not only supply membranes. It also designs complete industrial RO systems that suit different water conditions and production requirements. This approach allows industries to receive one complete solution instead of purchasing separate components from different suppliers.
3. Strong Technical Support
Technical support plays a major role in the success of every RO plant. Netsol Water provides expert guidance during system selection, installation, maintenance, and troubleshooting. Customers receive practical solutions whenever they face operational challenges. This support helps industries maintain continuous production without unnecessary delays.
Because of these strengths, many industries consider Netsol Water the answer to the question “Which company RO membrane is best in India?” The company continues to build trust through quality products, dependable service, and practical water treatment solutions.
Why Netsol Water Leads as an Industrial RO Plant Manufacturer
Selecting the right manufacturer is as important as choosing the right membrane. Industries expect long-term performance, reliable service, and customized solutions that match their production goals. Let us have a look at some qualities that make Netsol Water a trusted name across India.
1. Customized Plant Design
Every industry faces different water quality challenges. Netsol Water studies water characteristics before designing each RO plant. This careful planning allows the company to deliver systems that perform efficiently under different operating conditions. Customers receive plants that match their actual production requirements instead of standard designs.
2. Advanced Engineering
The company combines quality membranes with efficient pumps, pressure vessels, and control systems. This balanced engineering improves overall plant performance and supports smooth daily operation. Industries benefit from stable water production while lowering energy use and maintenance needs.
3. Focus on Customer Satisfaction
Customer relationships continue even after installation. Netsol Water provides maintenance support, membrane replacement guidance, and technical assistance whenever required. This commitment helps industries maintain consistent plant performance throughout the system’s life.
These strengths have helped the company become a respected Industrial RO Plant Manufacturer that serves industries across India with dependable water treatment solutions.
Factors to Consider Before Choosing an RO Membrane Company
Every business should evaluate several factors before investing in an RO membrane supplier. A careful decision protects the investment and ensures better long-term performance. Let us have a look at some important points that every industry should examine before making a final choice.
1. Product Quality
The first step is checking membrane quality and manufacturing standards. High-quality membranes deliver better filtration, stable performance, and longer operating life. They also help maintain water quality throughout industrial operations.
2. Industry Experience
Experienced manufacturers understand different industrial processes and water conditions. Their knowledge allows them to recommend suitable membranes and complete treatment systems for each application. This experience often prevents costly design mistakes.
3. Service and Maintenance
Good after-sales service supports uninterrupted plant operation. Industries should choose companies that provide installation support, maintenance guidance, and quick technical assistance whenever needed. Strong customer service builds confidence and improves long-term plant performance.
4. Complete Water Treatment Expertise
Companies that design complete RO plants understand how every component works together. Their expertise helps customers receive balanced systems that deliver better efficiency and dependable results. This is one reason why many industries choose Netsol Water as their preferred Industrial RO Plant Manufacturer for complete water treatment solutions.
Choosing the best RO membrane company in India requires careful attention to product quality, technical knowledge, customer support, and complete water treatment experience. A dependable membrane improves water purity, extends equipment life, and supports smooth industrial operations. At the same time, a trusted manufacturer helps industries receive the right solution for their specific requirements.
Netsol Water has built a strong reputation by delivering quality RO membranes, complete industrial water treatment systems, and dependable technical support. As a leading Industrial RO Plant Manufacturer, the company continues to help industries achieve efficient water purification with confidence. If your business is planning a new RO system or wants to upgrade an existing plant, you can contact Netsol Water for expert guidance and a customized consultation that matches your industrial water treatment needs.
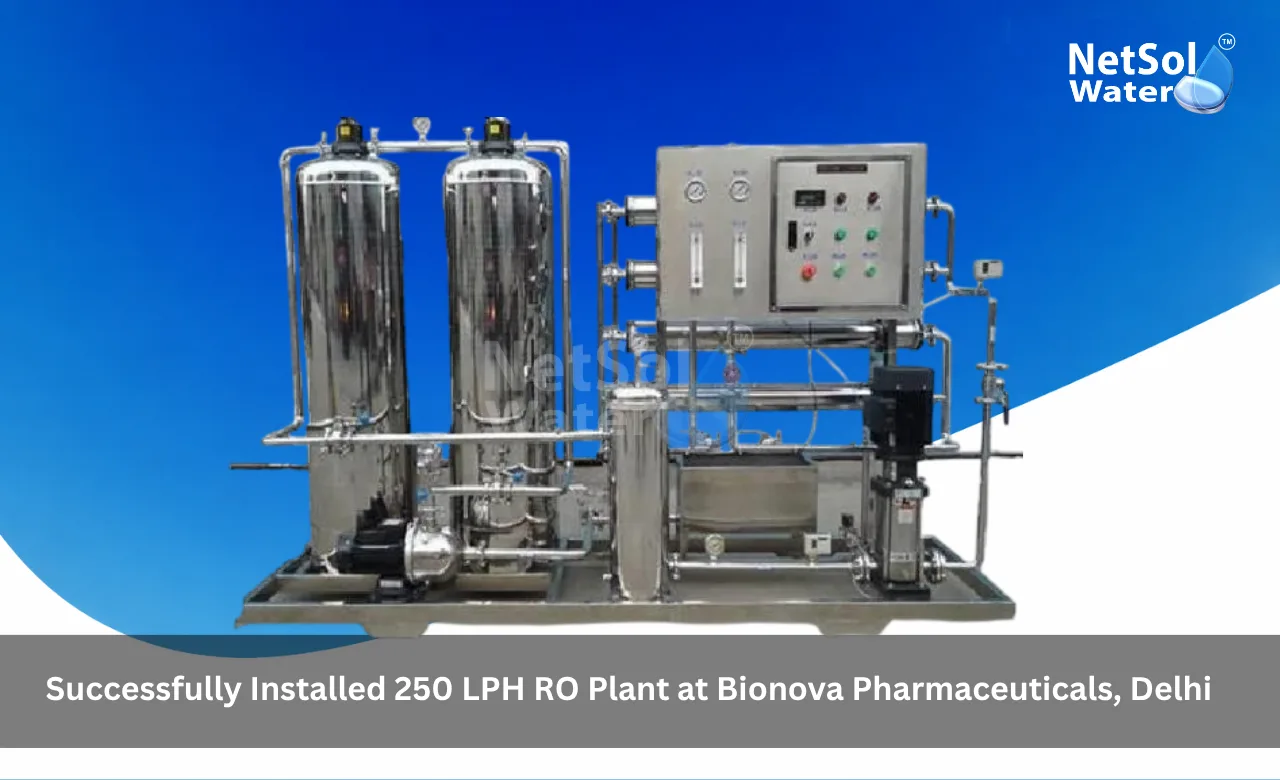
Successfully Installed 250 LPH RO Plant at Bionova Pharmaceuticals, Delhi
Reliable water quality plays an important role in facilities where water forms part of regular operations. This becomes especially important for pharmaceutical facilities because the water used within the premises needs to meet the purpose for which it is intended. When incoming water requires treatment, a suitable treatment plant can help the facility produce water with improved quality and support more controlled water use.
Bionova Pharmaceuticals in Delhi required a suitable water treatment solution for its facility. To address this requirement, Netsol Water successfully installed a 250 LPH RO plant at the site. The project focused on providing a practical RO-based treatment plant that could support the client’s intended water requirement.
The installation also reflects the role of us as a Commercial RO Plant Manufacturer in Delhi. By providing an RO plant that matches the stated capacity requirement, the project created a dedicated treatment arrangement for the client’s premises. The installed system gives the facility an organized method for treating incoming water instead of depending on untreated water for applications where better water quality is required.
Project Overview
A water treatment project needs to begin with a clear understanding of the client’s requirement. The treatment system should match the intended water demand and provide a process that is suitable for the quality of the incoming water. The 250 LPH RO plant installed at Bionova Pharmaceuticals was undertaken with this objective in mind. The project involved supplying and installing an RO-based water treatment solution with a stated production capacity of 250 litres per hour.
The main requirement was to establish an RO treatment facility within the client’s premises. RO provides a widely used method for reducing dissolved substances present in water through membrane-based separation. For a facility that needs treated water for defined operational purposes, an RO plant can provide a dedicated treatment stage between the incoming water source and the point where treated water is used.
The project scope therefore centred on the installation of the 250 LPH RO plant at Bionova Pharmaceuticals in Delhi. The work required the treatment system to be placed at the site and connected so that the plant could operate as intended. The objective was not simply to place the equipment at the facility. It was also to establish a functional treatment arrangement that could produce RO-treated water at the specified plant capacity.
This approach created a direct connection between the client’s requirement and the selected treatment technology. The capacity defined the expected treatment rate while the RO process provided the purification mechanism. The next important consideration was the nature of the client and the reason a dedicated water treatment system was required.
Client Details
Bionova Pharmaceuticals is the client for this project, and the available project information identifies it as a pharmaceutical organisation. Pharmaceutical facilities operate in an environment where process requirements can place greater attention on water quality. Water may be needed for different operational purposes within a facility and the suitability of that water depends on the application.
Bionova Pharmaceuticals required an RO plant and that a 250 LPH system was installed to address the stated treatment requirement. A dedicated treatment plant also provides a more structured method of handling water at the facility. Rather than treating water through an undefined arrangement, the client receives a defined treatment system with a stated output capacity. This gives the project a clear operational purpose and makes it easier to relate the plant size to the intended water requirement.
The requirement becomes particularly relevant in a pharmaceutical setting because water quality can influence how water is selected for different uses. With the client requirement established, the project location also becomes an important part of understanding the installation.
Detail
Information
Client
Bionova Pharmaceuticals
Facility Type
Pharmaceutical organisation
Location
Delhi
Solution Provided
250 LPH RO Plant
Installed By
Netsol Water
Project Location
The plant was installed at Bionova Pharmaceuticals in Delhi. Project location matters because the treatment plant must be installed within the operating environment of the client. The site must provide an appropriate arrangement for placing the treatment plant and allowing the treated water to move toward its intended point of use.
Bionova Pharmaceuticals is the location where the treatment solution had to be integrated into the client’s facility. The installation needed to suit the available site conditions and support normal operation after commissioning.
The location also highlights the relevance of local water treatment service capability. For organisations seeking a Commercial RO Plant Manufacturer in Delhi, access to a supplier that can handle the installation at the client’s premises can simplify the transition from equipment supply to plant operation. In this project, the treatment system was installed directly at the client’s Delhi facility.
Plant Capacity
Plant capacity determines how much treated water a system can produce over a given operating period. Selecting an appropriate capacity helps align the treatment system with the client’s expected requirement. A plant that does not match the intended demand may create operational limitations, while an appropriately selected capacity provides a clearer basis for planning water production.
For Bionova Pharmaceuticals, the installed RO plant has a capacity of 250 LPH, which means 250 litres per hour. The stated 250 LPH capacity gives the client a defined production rate for the installed RO system. At the specified operating rate, the plant is designed around a treatment output of 250 litres per hour. The actual daily quantity produced would depend on the plant’s operating hours and operating conditions.
Capacity also provides an important reference during operation and maintenance. The client and service team can use the rated 250 LPH figure as a basic reference when assessing plant operation. Any assessment of actual production would still require operating data collected from the plant.
The capacity requirement led directly to the selection of an RO treatment system designed around the specified output.
Parameter
Specification
Installed Capacity
250 LPH (Litres Per Hour)
Treatment Technology
Reverse Osmosis (RO)
Project Site
Bionova Pharmaceuticals, Delhi
Plant Type
Industrial / Pharmaceutical RO Plant
Design Basis
Defined production rate matched to client’s requirement
Treatment Technology
The treatment technology selected for the project is Reverse Osmosis. RO is a membrane-based water treatment process that separates water from many dissolved substances. It works by applying pressure to feed water so that water passes through a semi-permeable membrane while a significant portion of dissolved impurities is retained in the reject stream.
For the Bionova Pharmaceuticals installation, the 250 LPH RO plant uses this principle to produce treated water from the incoming feed water. The process provides a defined purification stage and allows the plant to handle water treatment through a controlled membrane system.
1. How Reverse Osmosis Works
An RO system uses pressure to move water through a membrane. The membrane allows water molecules to pass through more easily than many dissolved materials. As a result, the treated side receives permeate water while the concentrated stream carries away a portion of the substances separated from the feed.
The quality of the final treated water depends on factors such as the quality of the feed water, membrane condition, operating conditions and overall system design. For this reason, an RO plant must be operated within the conditions for which it was designed.
2. Relevance to the Project
The use of RO gave Bionova Pharmaceuticals a dedicated treatment process with a defined output capacity of 250 LPH. It also created a clear separation between incoming water and treated water. This arrangement can support better management of water quality for the applications that require RO-treated water.
Understanding the incoming water is equally important because RO treatment performance depends strongly on feed water conditions.
Influent Characteristics
Before any water treatment system is selected and operated, the characteristics of the incoming water need to be understood. Parameters such as total dissolved solids, hardness, turbidity, iron and microbial content can affect the treatment approach, membrane condition and overall plant performance.
Importance of Influent Assessment
Knowing the incoming water characteristics allows the treatment system to be matched more accurately to the water being handled. It can also help the operating team understand changes in plant performance over time. When raw water quality changes, the treatment response may also change.
The next stage is the treatment journey itself, where the incoming water moves through the RO system toward treated water production.
Treatment Process
A treatment system performs effectively when water moves through each stage in the intended sequence. Every stage has a purpose and the overall process depends on the proper interaction of those stages. In the Bionova Pharmaceuticals project, the central treatment technology is Reverse Osmosis and the installed plant has a rated capacity of 250 LPH.
1. Raw Water Entry
The treatment process begins when incoming water is directed to the RO plant. At this stage, the plant receives the feed water that requires treatment. The condition of this feed water affects the performance of the downstream membrane system.
2. Feed Water Preparation
RO membranes perform best when the incoming water reaches the membrane system under suitable operating conditions. Depending on the source water characteristics, an RO system may require suitable preparation before water reaches the membrane.
3. Reverse Osmosis Stage
Once the feed water reaches the RO membrane section, pressure drives the separation process. Water passes through the semi-permeable membrane and forms the treated permeate stream. Dissolved substances that do not pass through the membrane remain concentrated in the reject stream.
The RO stage therefore creates two streams from the feed water. One stream becomes treated water while the other carries the concentrated portion of the rejected material.
4. Treated Water Collection
The permeate generated through the RO process is collected as treated water. From there, it can be directed toward the intended point of use or storage arrangement provided at the facility. The important project outcome is that the RO plant was installed to produce treated water at the stated 250 LPH capacity.
This treatment sequence connects directly with the plant equipment. The equipment enables the feed water to move through the treatment process and supports the production of treated water.
Stage
Function
Raw Water Entry
Incoming feed water is directed to the RO plant
Feed Water Preparation
Prepares water so it reaches the membrane under suitable conditions
Reverse Osmosis Stage
Pressure drives separation into treated permeate and concentrated reject streams
Treated Water Collection
Permeate is collected and directed to the intended point of use or storage
Major Equipment
Correct equipment selection supports the stable operation of a water treatment plant. Each component in an RO system has a defined role, from moving water through the system to carrying out the membrane separation process. The equipment arrangement must also work together as one treatment unit. For the Bionova Pharmaceuticals project, the installation of a 250 LPH RO plant was done.
1. RO Plant Assembly
The principal equipment installed at the site is the 250 LPHReverse Osmosis plant itself. The plant provides the treatment framework through which the feed water passes and the RO membrane process takes place.
The system brings the treatment components together in a coordinated arrangement. Its primary purpose is to receive the incoming water and produce RO-treated water at the specified plant capacity.
2. Membrane Treatment Section
The membrane section represents the core of the RO process. Here, pressure enables water to pass through the semi-permeable membrane while a portion of dissolved material remains in the concentrated stream.
The equipment supports the process, but successful installation also depends on proper site execution. That brings the project to the installation stage.
Equipment
Role in the System
RO Plant Assembly (250 LPH)
Principal treatment framework through which feed water passes
Membrane Treatment Section
Core of the RO process; performs the separation under pressure
Installation Process
Installation requires more than placing a treatment unit at the client’s premises. The plant must be positioned correctly and connected so that the treatment system can function as intended. Careful execution at the site also helps prepare the system for testing and commissioning.
For the Bionova Pharmaceuticals project, the installation work focused on establishing the 250 LPH RO plant at the client’s Delhi facility. The process began with preparing the site for placement of the treatment system.
Once the site was ready, the RO plant was positioned in its designated area. Proper placement is important because the treatment system needs a suitable connection arrangement for feed water, treated water and reject water. The plant also requires an operating arrangement that allows access for routine observation and maintenance.
The next stage involved making the required system connections. These connections establish the path through which water enters the plant, moves through the RO treatment stage and leaves as treated water and reject water.
After the physical connections were established, the installed system could be prepared for functional testing. This stage links the installation activity with commissioning because a newly installed treatment plant must be checked before it enters regular service.
Plant Commissioning
Commissioning is necessary because installation alone does not confirm that a water treatment plant is ready for operation. The commissioning stage provides an opportunity to check the system after installation and verify that the treatment plant responds correctly when operated.
For the 250 LPH RO plant at Bionova Pharmaceuticals, commissioning followed the installation of the treatment system. The team checked the plant as part of the start-up process and prepared it for operational use.
A commissioning exercise for an RO plant generally involves checking the system connections, starting the treatment process, observing plant operation and confirming that water moves through the intended treatment path. The plant can then be assessed against the required operating conditions.
250 LPH RO plant was successfully installed and commissioned for the client’s facility. This completed the transition from equipment installation to an operational water treatment system.
Treated Water Reuse
Treating water creates value when the resulting water is used appropriately within the facility. The purpose of an RO plant is not limited to the treatment stage itself. The treated water must also be directed toward applications for which its quality is suitable.
At Bionova Pharmaceuticals, the installed system provides RO-treated water at a stated capacity of 250 LPH. The client can use the treated water for the purposes defined by its internal operational requirements and water quality criteria. The appropriate application should depend on the quality of the treated water and the requirements of the specific process in which it is used.
A controlled treated water stream can also make water handling more structured at the facility. Instead of treating water only at the point of use, the RO plant creates a central treatment stage that produces water through a defined process.
This provides a logical connection between treatment and operation. The plant treats the incoming water while the facility determines how the resulting water should be used based on its own requirements.
Results and Performance
Project results provide the clearest indication of whether a treatment system has addressed the requirement for which it was installed. In this project, the successful installation of a 250 LPH RO plant at Bionova Pharmaceuticals in Delhi has been done.
The completed installation provided the client with an RO-based treatment system with a defined production capacity. The plant establishes a dedicated method for treating incoming water and producing RO-treated water within the facility.
1. Successful Installation
The project was successfully completed with the installation of the specified 250 LPH RO plant. This means the client’s requirement for the installation of an RO treatment system was addressed through the completed project.
2. Defined Treatment Capacity
The installed system has a rated capacity of 250 LPH. This gives the client a clear reference for the plant’s intended treatment output. It also provides a basis for planning water production around the facility’s operating schedule.
3. Operational Water Treatment
The RO plant creates a dedicated water treatment process at the client’s premises. The system allows the facility to process incoming water through Reverse Osmosis and obtain treated water for appropriate uses.
From a project delivery perspective, the successful installation demonstrates the practical ability to provide an RO treatment solution for a defined industrial requirement. It also reflects the role of a Commercial RO Plant Manufacturer in Delhi in delivering and installing treatment systems at client facilities.
Confirmed Outcome
Status
Installation of 250 LPH RO Plant
Completed
System Connections & Testing
Completed
Plant Commissioning
Completed
Laboratory/TDS Data
Not provided — not included in this case study
Customer Feedback/Testimonial
Customer feedback is valuable because it provides a direct view of how the completed installation was received by the client. It can also help show whether the delivered system addressed the original requirement from the user’s perspective.
We are pleased with the successful installation of the 250 LPH RO plant at our facility in Delhi. The Netsol Water team understood our requirement and provided a suitable water treatment solution for our facility. The installation was carried out professionally and the system was commissioned successfully. We appreciate the team’s support throughout the installation process and are satisfied with the overall project execution. The RO plant has provided us with a dedicated solution for producing treated water as required at our facility.
A well-planned water treatment system can provide a facility with a defined method for managing the quality of its incoming water. The installation of the 250 LPH RO plant at Bionova Pharmaceuticals in Delhi addressed the client’s stated requirement for an RO-based treatment solution. The completed plant provides a treatment capacity of 250 LPH and establishes a dedicated RO process at the facility.
The project also demonstrates how treatment technology can be matched with a defined operational requirement. Reverse Osmosis provides the central purification process while the installed plant brings the treatment arrangement into the client’s premises. The successful installation itself represents a completed water treatment solution based on the specified capacity.
Netsol Water serves as a Commercial RO Plant Manufacturer in Delhi and provides water treatment solutions for organisations with different treatment requirements. Businesses that need a suitable RO system can discuss their water quality, capacity requirement and site conditions with the technical team before selecting a plant.
For more information about RO water treatment solutions or to discuss a similar requirement, contact Netsol Water for a consultation and project discussion personalized to your facility.
Successfully Installed 24,000 LPH RO Plant at MES BUILDERS ASSOCIATION OF INDIA
Reliable water treatment plays an important role wherever a facility requires a steady supply of treated water for its operations. Water quality can vary depending on the source and local conditions. A suitable treatment system therefore needs to match the required capacity and the intended use of treated water. The installation completed for MES BUILDERS ASSOCIATION OF INDIA demonstrates how a planned RO solution can address a defined water treatment requirement with an installed capacity of 24000 litres per hour.
Netsol Water completed the installation of a 24000 LPH RO plant for MES BUILDERS ASSOCIATION OF INDIA. The project focused on providing a treatment system with sufficient processing capacity for the client’s requirement.
The project also reflects the practical role of Netsol Water as a Commercial RO Plant Manufacturer in Delhi. By matching the treatment system with the specified capacity, the installation created a dedicated water treatment arrangement for the client’s facility.
Project Overview
A commercial water treatment project requires more than simply installing a treatment unit. The selected plant must match the required treatment capacity and support the intended use of the treated water. The 24000 LPH installation for MES BUILDERS ASSOCIATION OF INDIA was planned around this basic requirement. The project provided the client with a dedicated RO treatment system capable of processing water at a rated capacity of 24000 litres per hour.
The main objective was to install a suitable RO plant that could address the client’s water treatment requirement through a defined and organised treatment system. Reverse Osmosis remains widely used where dissolved substances in water need to be reduced through membrane-based treatment. For a commercial installation, the system must also be arranged in a way that allows the treatment process to operate in a controlled and practical manner.
Netsol Water handled the project as a complete installation assignment rather than treating the RO plant as an isolated piece of equipment. The work centred on establishing the plant at the client facility and preparing the system for operation. This included the installation of the specified 24000 LPH RO plant and the necessary site-level execution associated with commissioning the treatment system.
The project scope is important because treatment capacity directly affects how a plant supports an organisation’s water requirement. An undersized system may not provide sufficient treatment output while an unnecessarily large system may create avoidable capital and operating considerations. The 24000 LPH capacity therefore formed the central design reference for the project and guided the installation work.
With the project objective established, the next consideration is the client for whom the treatment plant was installed and the requirement that led to the project.
Client Details
MES BUILDERS ASSOCIATION OF INDIA is the client identified for this RO plant installation. The need for a commercial RO plant indicates a requirement for treated water with a defined processing capacity. Water treatment becomes particularly relevant when an organisation must manage the quality of its available water before using it for its intended purpose. The role of the RO plant in this project was to provide a dedicated treatment stage rather than depending on untreated source water alone.
For the client, the selection of a 24000 LPH plant established a clear treatment capacity. This gave the project a measurable operational reference and provided a system around which water treatment activities could be organised. The installation also helped convert the requirement for treated water into a dedicated treatment infrastructure at the facility.
Since the project was carried out at a client facility, location forms another important part of understanding the installation.
Detail
Information
Client
MES Builders Association of India
Requirement
High-capacity dedicated RO treatment stage
Solution Provided
24,000 LPH RO Plant
Installed By
Netsol Water
Project Location
Project location influences the practical planning of any water treatment installation because the available site determines how equipment can be placed and connected. Access to the treatment area, available installation space and the arrangement of the facility can affect execution work. These considerations become especially relevant when a commercial RO plant is installed at an existing site.
For the MES BUILDERS ASSOCIATION OF INDIA project, the exact project address is Sahyog Building, 807,808 58, Nehru Place, New Delhi, Delhi 110019. The location matters from an installation perspective because the plant had to be positioned within the client’s facility in a way that supported its intended operation. The installation team needed to execute the work according to the physical conditions of the site. Proper placement helps create a practical connection between the water source, treatment system and treated water arrangement.
The project location also connects directly with the next consideration, which is the treatment capacity selected for the facility. Once the installation site is established, the capacity of the treatment plant becomes the main reference for the system’s intended performance.
Detail
Information
Project Address
Sahyog Building, 807,808 58, Nehru Place, New Delhi, Delhi 110019
City
New Delhi
Plant Capacity
Plant capacity determines how much water a treatment system can process over a given operating period. Choosing the correct capacity is therefore an essential part of planning a commercial RO installation. The capacity needs to correspond with the intended treatment requirement so that the plant can provide an appropriate volume of treated water during operation.
For this project, Netsol Water installed a 24000 LPH RO plant for MES BUILDERS ASSOCIATION OF INDIA. The notation LPH means litres per hour and identifies the rated water treatment capacity of the installed RO system. At the specified capacity, the plant is designed around the client’s requirement for a high-volume commercial water treatment arrangement.
The selected 24000 LPH capacity gives the client a clearly defined treatment rate. It also provides a practical reference for operating the plant and planning treated water availability. Capacity is particularly important in larger installations because water requirements need to be considered in relation to the treatment rate rather than only the storage volume.
This capacity also establishes the technical context for the selected treatment technology. The system uses Reverse Osmosis as the principal treatment process, making the membrane stage central to the project’s water treatment function.
Parameter
Specification
Installed Capacity
24,000 LPH (Litres Per Hour)
Treatment Technology
Reverse Osmosis (RO)
Project Site
Nehru Place, New Delhi
Plant Type
High-Capacity Commercial RO Plant
Design Basis
Rated treatment capacity matched to client’s requirement
Treatment Technology
The treatment technology determines how the plant handles the incoming water and what kind of treatment performance it can provide. Reverse Osmosis was selected for this installation and forms the central treatment process within the 24,000 LPH plant.
1. Reverse Osmosis
Reverse Osmosis is a membrane-based water treatment process. In an RO system, water is supplied to a semi-permeable membrane under pressure. The membrane allows water molecules to pass through while restricting many dissolved salts and other unwanted substances. The treated stream that passes through the membrane is known as permeate or RO product water. The concentrated stream carries the rejected dissolved material away from the membrane side.
The process works by applying pressure to overcome the natural movement of water through the membrane. Under normal conditions, water tends to move from a region of lower dissolved concentration toward a region of higher dissolved concentration through a semi-permeable membrane. Reverse Osmosis applies pressure in the opposite direction so that water moves through the membrane while a significant portion of dissolved material remains behind.
For a commercial installation such as the one completed for MES BUILDERS ASSOCIATION OF INDIA, the RO membrane stage provides the main treatment barrier. It allows the plant to process a large water flow while applying a controlled membrane-based separation process.
2. Importance of Pretreatment
RO membranes require suitable feed water conditions because suspended material and certain contaminants can interfere with membrane operation. Pretreatment is normally selected according to the characteristics of the incoming water. It can help reduce substances that may otherwise affect membrane performance.
The specific pretreatment equipment and treatment stages used in this project have not been provided. The project information only confirms the installation of the 24,000 LPH RO plant.
3. Membrane Treatment and Water Separation
The main RO stage receives pressurised feed water and separates it into treated water and a concentrated reject stream. The treatment technology provides the basic framework for the project. Its purpose is to process the available feed water through a membrane-based system so that the client receives treated water from the RO stage at the specified plant capacity.
Understanding the incoming water is equally important because water characteristics influence treatment requirements and membrane operation. The next section therefore focuses on the influent information available for this project.
Influent Characteristics
Understanding the quality of incoming water is an essential step in water treatment planning. Raw water may contain dissolved salts, hardness, suspended matter, microorganisms or other substances that influence the selection and operation of a treatment system. Proper water analysis helps determine what treatment stages are needed and provides a basis for monitoring system performance.
Role of Water Quality Testing
Water quality testing helps identify the treatment challenges that the RO plant needs to manage. TDS can indicate the level of dissolved substances in water. Hardness can affect scaling potential. Turbidity reflects suspended particles that may interfere with downstream treatment. Iron can create fouling concerns under certain conditions. Microbial testing can provide information about biological quality.
These parameters normally help engineers determine the treatment arrangement and operating requirements. With the plant capacity and treatment technology established, it is possible to explain the treatment journey from incoming water to RO-treated water.
Parameter
Relevance to Treatment
TDS
Indicates the level of dissolved substances in water
Hardness
Can affect scaling potential
Turbidity
Reflects suspended particles that may interfere with downstream treatment
Iron
Can create fouling concerns under certain conditions
Microbial Content
Provides information about biological quality
Treatment Process
A proper treatment sequence allows each stage of a water treatment plant to support the next stage. In an RO-based system, raw water enters the treatment arrangement and is prepared for membrane treatment before it reaches the RO stage. The membrane system then separates the treated water from the concentrated stream.
1. Raw Water Entry
The treatment journey begins when incoming water is brought into the treatment system. At this stage, the water represents the source condition that requires treatment. The source water quality determines the treatment load and influences how the RO stage should be operated.
A commercial RO plant needs controlled feed flow because the membrane system depends on a steady and suitable supply of water. Proper handling of the incoming stream helps maintain consistency as the plant moves into the treatment stage.
2. Feed Water Preparation
Before water reaches the RO membranes, the feed normally requires conditions suitable for membrane operation. The exact preparation stage depends on the quality of the incoming water and the plant design. The purpose is to make the feed appropriate for the membrane stage and reduce conditions that could negatively affect its operation.
Because the project records supplied here do not identify specific pretreatment units, this section does not name individual filters or dosing systems as project equipment.
3. Pressure and Membrane Treatment
The prepared feed enters the RO system where pressure drives water through the semi-permeable membranes. The membranes allow a portion of the water to pass through while restricting many dissolved substances.
This stage creates two water streams. The first is the treated permeate stream. The second is the concentrated reject stream containing a higher proportion of the rejected dissolved material.
4. Treated Water Collection
The RO permeate becomes the treated water output of the membrane system. The treated stream can then move into the client’s designated treated water arrangement according to the facility’s requirements. The collection and use of treated water depend on the site layout and intended application.
5. Reject Stream Handling
RO treatment also produces a reject stream because the membrane does not convert all feed water into permeate. The reject contains the material retained by the membrane and must be handled according to the site’s water management arrangement.
The process demonstrates how the different treatment stages fit together around the RO membrane. Equipment selection supports these stages and provides the physical framework required for plant operation.
Stage
Function
Raw Water Entry
Incoming water is brought into the treatment system; represents the source condition
Feed Water Preparation
Conditions the feed to suit membrane operation
Pressure and Membrane Treatment
Pressure drives water through the membrane, producing permeate and reject streams
Treated Water Collection
Permeate becomes the treated water output for the client’s designated arrangement
Reject Stream Handling
Concentrated reject stream is handled per the site’s water management arrangement
Major Equipment
Equipment selection plays an important role in ensuring that a commercial treatment plant can perform its intended function. Each component must support the water flow, pressure requirements and treatment sequence of the system. In an RO plant, the membrane system forms the core treatment stage while associated equipment helps move and control the water.
1. RO Membrane System
The RO membrane system is the central treatment component. It receives pressurised feed water and performs the membrane separation that produces treated permeate and concentrated reject.
The membrane stage defines the core function of the installed RO plant. Its operation needs suitable feed conditions and controlled pressure so that water can pass through the membrane as intended.
2. Flow and Pressure Arrangement
An RO plant also requires a controlled method for moving water through the treatment system. Water must reach the membrane stage at the pressure required for Reverse Osmosis operation.
3. Control and Monitoring
Commercial RO systems also require operating controls and monitoring arrangements so that water flow and treatment conditions can be observed during operation.
Once the plant components are brought to the site, careful installation becomes necessary to turn the treatment design into an operating system.
Equipment
Role in the System
RO Membrane System
Central treatment component; produces treated permeate and concentrated reject
Flow and Pressure Arrangement
Moves water through the system and delivers pressure required for RO operation
Control and Monitoring
Allows water flow and treatment conditions to be observed during operation
Installation Process
Plant installation requires proper planning because treatment equipment must be positioned and connected in a logical sequence. The installation team needs to consider the site arrangement while ensuring that the treatment system can receive feed water and deliver treated water as intended.
For the MES BUILDERS ASSOCIATION OF INDIA project, Netsol Water carried out the installation of the specified 24,000 LPH RO plant at the client facility. The work began with preparing the installation area and organising the site for placement of the treatment system. Proper site readiness helps create the conditions required for equipment placement and system assembly.
Equipment placement then formed the next stage of execution. The treatment system needed to be positioned within the available facility area so that the water treatment arrangement could function as a connected system. Correct placement is important because the physical arrangement of equipment affects access, piping and operational convenience.
After positioning the plant, the installation work moved into the connection stage. Water lines and system connections needed to be arranged so that incoming water could reach the treatment system and treated water could move toward the designated outlet or storage arrangement.
The installation also required attention to the relationship between the different treatment stages. A commercial RO plant cannot operate effectively as disconnected individual units. Water must move through the treatment sequence in the correct direction and at suitable operating conditions.
Once the physical installation and connections were completed, the system moved into testing and commissioning. This final stage allowed the team to check the plant before regular operation.
Plant Commissioning
Commissioning provides the transition between installation and routine plant operation. A newly installed RO plant needs to be checked under operating conditions so that the installation team can confirm that the system functions as intended.
After completing the installation of the 24,000 LPH RO plant, the system was prepared for commissioning. The commissioning stage involved checking the installed treatment arrangement and ensuring that the system was ready for operation. A proper commissioning process generally includes verification of connections, water flow and operating conditions before regular use begins.
The treatment flow also needs to follow the intended path from feed water entry through the RO membrane stage and toward the treated water outlet. These checks help identify installation issues before the plant enters normal operation.
Commissioning formed part of the successful installation of the 24,000 LPH RO plant. The process provided the necessary step between completing physical installation work and placing the treatment system into use.
Once the treatment plant was ready to operate, the value of the system depended on how the treated water could support the client’s requirements.
Treated Water Reuse
Treated water becomes most useful when the facility can use it according to its intended application. A water treatment plant is therefore not only about producing treated water. It also needs to provide an output that fits into the client’s overall water management arrangement.
For MES BUILDERS ASSOCIATION OF INDIA, the installed RO plant provides treated water through the RO process at a rated capacity of 24,000 LPH.
The treated water output can support the client’s water management requirement according to the actual use planned at the facility. Efficient use of the output also helps ensure that the value of the installed treatment system extends beyond the plant itself and into daily facility operations.
The practical significance of the project becomes clearer when the available results and measurable outcomes are considered.
Results and Performance
Project results provide the clearest way to evaluate whether an installed treatment solution addressed the defined requirement. In this installation, the most clearly documented result is the successful completion of a 24,000 LPH RO plant installation for MES BUILDERS ASSOCIATION OF INDIA.
The first major outcome is the establishment of dedicated RO treatment capacity at the client’s facility. The installed plant provides a rated processing capacity of 24,000 litres per hour. This creates a defined treatment resource for the client’s water requirement.
The second outcome is the implementation of Reverse Osmosis as the principal treatment technology. The membrane-based process provides a structured method for separating treated water from a concentrated reject stream.
Another important result is the completion of the installation and commissioning sequence. Bringing the plant from site installation to a commissioned treatment system converts the project from an equipment supply requirement into an operational treatment arrangement.
The strongest measurable project result remains the confirmed 24,000 LPH treatment capacity and the successful installation of the RO plant for the client. These documented outcomes show that the project delivered the specified treatment infrastructure without introducing unsupported performance claims.
The client’s perspective provides another useful way to describe the completed project while staying within the available information.
Confirmed Outcome
Status
Installation of 24,000 LPH RO Plant
Completed
Implementation of Reverse Osmosis Treatment
Completed
Installation & Commissioning Sequence
Completed
Laboratory/TDS Data
Not provided — not included in this case study
Customer Feedback/Testimonial
Customer feedback helps show how a completed installation is viewed from the client’s side. It can also indicate whether the delivered system addressed the requirement for which it was installed.
“We required a high-capacity RO treatment system for our facility and the installation of the 24,000 LPH RO plant provided us with a defined water treatment capacity. The plant was installed for our requirement and gave us a dedicated Reverse Osmosis treatment system for managing the required water treatment process. The completed installation provides a clear treatment arrangement with a rated capacity of 24,000 litres per hour.”
A successful water treatment installation begins with a clear understanding of the required capacity and the purpose of treatment. The 24,000 LPH RO plant installed for MES BUILDERS ASSOCIATION OF INDIA shows how a defined commercial water treatment requirement can be addressed through a dedicated Reverse Osmosis system. The project delivered a treatment plant with the required 24,000 LPH capacity and established a structured treatment arrangement at the client’s facility.
Netsol Water works as a Commercial RO Plant Manufacturer in Delhi and provides water treatment solutions for commercial requirements based on the capacity and treatment needs of the site. Proper system selection helps organisations avoid mismatched treatment capacity and supports a more practical approach to water management.
For businesses and institutions evaluating a commercial RO installation, the right starting point is a clear assessment of water requirements, source water quality and expected treatment capacity. Netsol Water can assist in evaluating similar requirements and identifying an appropriate RO treatment solution.
For more information about commercial RO plants or to discuss a water treatment requirement, contact Netsol Water for a consultation and project discussion. A suitable treatment system can help create a structured and dependable approach to managing treated water at commercial facilities.
Successfully Installed 10,000 LPH RO Plant at Suroj Buildcon, World Street Sports Center, Delhi
Suroj Buildcon at World Street Sports Center in Delhi required a dependable water treatment solution to meet its operational water needs. For such a facility, the quality and availability of treated water can affect daily activities and the overall management of water resources. The project therefore called for a treatment system that could process the available water and provide a suitable source of treated water for intended use.
We completed the installation of a 10,000 LPHReverse Osmosis plant at the site. The project focused on providing a practical treatment system that could support the client’s water requirement through a structured purification process. Reverse Osmosis offers a suitable method for reducing dissolved impurities in feed water. It works by pushing water through a semi-permeable membrane under pressure while separating a large part of the dissolved salts and other unwanted substances.
The successful completion of the installation added a dedicated water treatment system to the facility. It also demonstrated the importance of selecting the right plant capacity and arranging the treatment stages in a suitable sequence.
Project Overview
A commercial water treatment project needs more than the installation of a single purification unit. It requires an understanding of the site requirement and a treatment arrangement that can support regular operation. The project at Suroj Buildcon, World Street Sports Center, Delhi was planned around this need. The main objective was to install a suitable RO system with sufficient treatment capacity for the intended application.
The scope of the project included the installation of a 10,000 LPH RO plant. The treatment system was selected to address the need for treated water through membrane-based purification. The project also involved arranging the plant components in a practical sequence so that incoming water could move through the required treatment stages before reaching the final treated water section.
The installation had to suit the project site and provide an organised treatment setup. Proper equipment placement and system connection were important because the treatment process depends on coordination between different components. A well-planned arrangement also supports easier operation and maintenance.
With these requirements in mind, the project moved from planning to installation at the client’s facility. The next section looks at the client and explains the project requirement in relation to the site.
Client Details
Suroj Buildcon was the client for this project. The installation took place at its World Street Sports Center facility in Delhi. The need for an RO plant indicates that the facility required a controlled source of treated water for its intended operations. In a commercial setting, water treatment helps provide better control over water quality when the incoming water contains dissolved substances that need to be reduced. The treatment system can also help create a more consistent source of processed water than relying only on untreated feed water.
For this project, the client selected a system with a 10,000 LPH treatment capacity. That choice established a clear treatment scale for the installation and allowed the plant to be designed around the required output.
The project was carried out at a specific commercial facility in Delhi. Its location was an important part of the installation because the treatment system had to fit the available site conditions and work within the operational setting of the facility.
Detail
Information
Client
Suroj Buildcon
Facility
World Street Sports Center
Location
Delhi
Solution Provided
10,000 LPH RO Plant
Installed By
Netsol Water
Project Location
The location of a water treatment plant influences how the equipment is arranged and how the system is connected. Commercial facilities often have existing infrastructure and space limitations that must be considered before equipment installation begins. The RO plant at Suroj Buildcon was installed at World Street Sports Center in Delhi.
Delhi is a large urban environment where commercial sites can have varied water sources and different treatment requirements. For a project like this, the treatment system must fit the actual site rather than follow a fixed arrangement. The plant therefore needed to be positioned in a manner that allowed the treatment stages and related connections to function properly.
The World Street Sports Center site provided the setting for the installation of the 10,000 LPH system. The project team had to consider the available installation area and the practical arrangement of the treatment equipment. This helped create a setup that could support the intended treatment process without unnecessary complications.
Once the location and site needs were considered, the next major factor was plant capacity. The treatment output had to match the purpose for which the system was installed.
Plant Capacity
Selecting the right plant capacity is important because an RO system must process enough water to serve the intended requirement. A plant with insufficient capacity may not meet demand when treated water is needed. A suitable capacity provides a defined treatment output and creates a clear operating basis for the facility.
For Suroj Buildcon, Netsol Water installed a 10,000 LPH RO plant. LPH stands for litres per hour. This means the plant has a designed treatment capacity of 10,000 litres of feed water per hour under the relevant operating conditions.
The installed capacity gives the project a substantial treatment scale for commercial use. It provides a clear flow rate for planning the treated water supply within the facility. At the same time, actual production can depend on operating conditions and feed water characteristics. Factors such as membrane performance, pressure, water temperature and feed quality can influence real output.
The 10,000 LPH capacity formed the basis of the treatment system. To achieve effective purification, the plant also needed the right treatment technology. Reverse Osmosis was selected as the main purification process for the project.
Parameter
Specification
Installed Capacity
10,000 LPH (Litres Per Hour)
Treatment Technology
Reverse Osmosis (RO)
Project Site
World Street Sports Center, Delhi
Plant Type
Commercial / Industrial RO Plant
Influencing Factors
Membrane performance, pressure, water temperature, feed quality
Treatment Technology
The treatment technology determines how the plant removes unwanted substances from water. For this project, Reverse Osmosis served as the primary purification method. RO is widely used in water treatment where the objective is to reduce dissolved salts and other impurities from feed water.
1. Reverse Osmosis Process
Reverse Osmosis works by applying pressure to water and directing it through a semi-permeable membrane. The membrane allows water molecules to pass through while restricting many dissolved salts and other dissolved contaminants. The process produces two streams. One is the treated water that passes through the membrane and the other is the reject or concentrate stream that carries a higher level of rejected dissolved substances.
The performance of an RO plant depends on preparing the feed water before it reaches the membranes. Suspended particles and other substances can affect membrane operation if the water enters the RO section without suitable pre-treatment. Pre-treatment therefore supports the main membrane stage by improving the quality of water entering the RO unit.
2. Role of Membrane Treatment
The RO membrane acts as the central separation stage in the plant. Water passes across the membrane under pressure. The membrane separation process reduces the concentration of dissolved substances in the permeate stream. This makes RO useful when a facility needs a more controlled treated water source.
The technology selected for the Suroj Buildcon project was therefore aligned with the need for membrane-based purification. However, the exact feed water chemistry remains important because RO design depends on incoming water quality. This brings the discussion to the influent characteristics considered for the project.
Influent Characteristics
Understanding the incoming water quality is an important part of designing and operating an RO plant. Feed water characteristics determine the treatment burden placed on the system and influence the level of pre-treatment required before membrane filtration. Parameters such as TDS, hardness, turbidity, iron, suspended matter and microbial content can affect treatment performance.
The importance of feed water quality remains clear. Dissolved salts can increase the load on the RO membrane. Hardness-forming substances can contribute to scaling under unsuitable operating conditions. Turbidity and suspended particles can affect upstream filtration. Iron and other unwanted substances may also need attention depending on the source water.
The treatment system must therefore address the feed water in stages. Pre-treatment prepares the incoming water, while the RO section carries out the primary dissolved impurity reduction. The following section explains how this treatment sequence works.
Treatment Process
A successful RO plant follows a treatment sequence in which each stage prepares the water for the next. This sequence helps protect the major treatment components and improves the overall functioning of the system. At the Suroj Buildcon site, the 10,000 LPH RO plant was arranged around the basic principle of controlled feed water movement followed by membrane purification.
1. Raw Water Entry and Pre-Treatment
The process begins when raw water enters the treatment system. Before the water reaches the RO membrane, it needs appropriate conditioning and filtration. Pre-treatment helps reduce the load caused by particles and other substances that may interfere with downstream equipment.
Depending on the actual feed water condition, pre-treatment can include filtration and other conditioning stages. The purpose is to provide water of a more suitable quality for the RO membrane.
2. Pressure and RO Feed
After the required pre-treatment, the water moves towards the RO section. The RO membrane needs pressure to perform the separation process. A high-pressure arrangement pushes water through the membrane while the membrane restricts many dissolved impurities.
This stage produces the treated permeate stream. It also generates reject water that contains a higher concentration of the substances removed by the membrane. Managing these two streams is an important part of RO operation.
3. Treated Water Collection
The permeate produced by the RO membrane moves into the treated water section for collection and use. The final water quality depends on feed water quality and plant operating conditions. The treatment sequence therefore creates a controlled path from raw water entry to purified water output.
Every stage supports the next. Good pre-treatment helps protect the membrane. Proper membrane operation supports the desired separation. Controlled collection ensures that the treated stream remains available for its intended application.
The treatment process can perform effectively only when the equipment supporting each stage is selected and installed correctly. This makes the major equipment an important part of the project.
Stage
Function
Raw Water Entry & Pre-Treatment
Conditions and filters incoming water to reduce the load reaching the RO membrane
Pressure and RO Feed
High-pressure arrangement pushes water through the membrane, producing permeate and reject streams
Treated Water Collection
Permeate moves into the treated water section for collection and use
Major Equipment
Equipment selection has a direct effect on the working of a water treatment plant. Each component performs a specific role and must work in coordination with the other stages. At the Suroj Buildcon project, the equipment arrangement supported the 10,000 LPH RO treatment process.
1. RO Membrane System
The RO membrane system forms the main purification section of the plant. Its function is to separate a large share of dissolved substances from the feed water by using pressure-driven membrane filtration. The permeate becomes the treated water stream while the concentrate leaves as reject water.
2. Feed and Pressure Arrangement
An RO plant needs controlled water flow and pressure so that the membrane can operate within its required conditions. The feed arrangement supplies water to the treatment line and the pressure system supports membrane filtration.
3. Pre-Treatment Equipment
Pre-treatment equipment prepares the feed water before it reaches the RO membrane. Its role is to reduce the effect of suspended matter and other feed water conditions that could interfere with membrane performance.
4. Piping and Interconnections
Piping forms the connection between the different treatment stages. Correct routing is important because the system depends on controlled movement of raw water, treated water and reject water. Proper connections also help reduce the risk of leakage or incorrect flow during operation.
Together, these components create the functional treatment system. Their correct installation was the next step in completing the project.
Equipment
Role in the System
RO Membrane System
Main purification section; separates dissolved substances from feed water
Feed and Pressure Arrangement
Supplies water to the treatment line and supports membrane filtration
Pre-Treatment Equipment
Reduces suspended matter and conditions that could interfere with membrane performance
Piping and Interconnections
Connects treatment stages and controls movement of raw, treated and reject water
Installation Process
Plant installation requires careful planning because water treatment equipment must work as one connected system. The installation process at the Suroj Buildcon site involved arranging the treatment system so that the major components could function in the required sequence.
The first stage involved preparing the site for equipment placement. The installation area needed to provide sufficient space for the plant and its connections. Equipment was then positioned according to the planned treatment flow. This arrangement helped maintain a logical path from raw water entry through the treatment section to treated water collection.
After placement, the different system components were connected to form the complete treatment line. The required piping connections were arranged between the relevant stages. Electrical and operational connections were also completed as part of the installation process.
Attention to connection and alignment was important because even a properly selected treatment unit can perform poorly when the installation does not support the required flow and operating conditions. The installation team therefore completed the system as an integrated setup rather than treating each component as a separate unit.
After the physical installation was completed, the system moved to the testing and commissioning stage. This step was necessary before regular operation could begin.
Plant Commissioning
Commissioning confirms that an installed water treatment plant is ready for operation. It allows the team to test the system and identify issues that may not be visible during physical installation. For the 10,000 LPH RO plant, commissioning formed the final technical stage before the system could be placed into regular service.
The commissioning process involved checking the installed treatment arrangement and verifying that the equipment and connections worked together correctly. The team assessed water movement through the treatment stages and checked the operating behaviour of the RO section. The system also needed to demonstrate that it could function according to the intended project capacity and treatment arrangement.
Commissioning is particularly important for RO plants because membrane treatment depends on controlled flow and pressure. The team must therefore ensure that the treatment sequence operates correctly before the plant is handed over for regular use.
Once the system passed the required checks, the plant could move into operation. This provided the client with a dedicated treatment system for the intended use of treated water.
Treated Water Reuse
Treating water is most useful when the facility can make effective use of the treated output. An RO plant does not simply improve water quality at the treatment point. It creates a processed water stream that can support the applications for which the system was installed.
At Suroj Buildcon‘s World Street Sports Center facility, the 10,000 LPH RO plant provides treated water for the client’s intended requirement. The practical value of the system comes from providing a dedicated source of treated water that the facility can manage according to its operational needs. The plant capacity and treatment process establish a structured way to produce treated water rather than leaving the facility dependent only on incoming raw water quality.
This treatment arrangement also connects directly with the project’s overall performance. A successful result depends on the plant providing the required treatment capacity while operating as an integrated system.
Results and Performance
Project results help show whether an installed treatment system has met its intended purpose. In this project, the main measurable fact provided is the successful installation of a 10,000 LPH RO plant at the client’s facility.
The completed installation gave Suroj Buildcon a dedicated commercial RO treatment system designed for a capacity of 10,000 litres per hour. This provides the facility with a defined treatment output and a structured process for producing treated water.
The project also established a complete treatment route from feed water entry to RO-based purification and treated water collection. The value of this arrangement lies in its ability to bring water treatment into a dedicated plant system that can be managed and operated for the facility’s requirements.
The successful completion of the installation is itself an important project outcome. It shows that the planned treatment capacity and RO technology were implemented at the specified site. The next measure of project value comes from the client’s response.
Confirmed Outcome
Status
Installation of 10,000 LPH RO Plant
Completed
Treatment System Connections (piping, electrical)
Completed
Plant Commissioning
Completed
Laboratory/TDS Data
Not provided — not included in this case study
Customer Feedback or Testimonial
Customer feedback provides useful insight into how a completed installation performs from the client’s perspective. It can confirm whether the project met the expected requirement and whether the client was satisfied with the installation and treatment solution.
We are pleased with the installation of the 10,000 LPH RO plant at our World Street Sports Center facility in Delhi. Netsol Water understood our requirement and provided a suitable water treatment solution for the site. The installation was completed professionally and the system was commissioned as planned.
The overall installation process was handled in an organised manner. The team supported us during equipment installation, system connections and commissioning. We appreciate the professional approach taken by Netsol Water and the attention given to completing the project according to our requirement.
The 10,000 LPH RO plant has provided us with a dedicated water treatment system for our facility. We are satisfied with the successful completion of the project and the support provided by the Netsol Water team.
The installation of the 10,000 LPH RO plant at Suroj Buildcon‘s World Street Sports Center in Delhi created a dedicated water treatment solution suited to the project’s stated requirement. The system uses Reverse Osmosis as its main purification technology and provides a defined treatment capacity of 10,000 litres per hour. From site preparation and equipment placement to system connections and commissioning, each stage contributed to the successful completion of the project.
The project also highlights the importance of choosing the right treatment capacity and arranging the treatment process in a clear sequence. Proper pre-treatment supports membrane operation while the RO stage helps reduce dissolved impurities from the feed water. The completed installation gives the client a structured source of treated water for its intended commercial requirement.
Netsol Water is the leading Commercial RO Plant Manufacturer in Delhi and provides water treatment solutions for commercial and industrial requirements. Businesses looking for a suitable RO plant can discuss their water source, treatment needs and required capacity with the Netsol Water team.
For information about RO plant solutions or to discuss a similar requirement, contact Netsol Water for a consultation.