RO Plant Gurgaon - Sewage Treatment Plant Manufacturers

What-are-the-Applications-of-Commercial-Water-Softeners-3.webp

August 17, 2026by Netsol Water

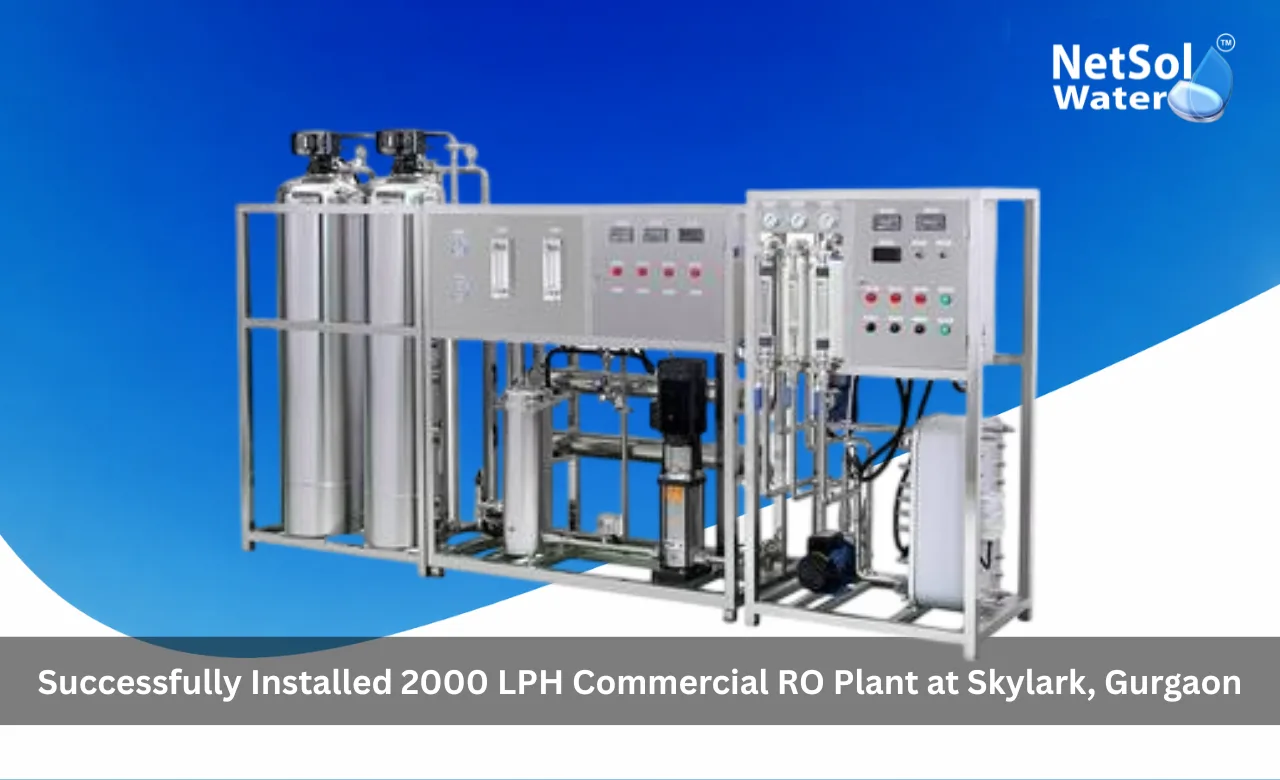
Successfully Installed 1000 LPH Commercial RO Plant at Skylark, Gurgaon

Commercial offices, infrastructure companies, manufacturing facilities, institutions and hotels need reliable access to appropriately treated water. The incoming water may have excessive dissolved salts, hardness, suspended particles or other undesirable constituents; a properly designed commercial RO system can help maintain the necessary treated-water quality. We installed and commissioned a 1000 LPH Commercial RO Plant at Skylark, Gurgaon for its production of about 1000 litres of RO treated water per hour with the specified operating conditions. The project embodies our work as a reputed Commercial RO Plant Manufacturer in Gurgaon.

Project Overview

The main goal of this project was to set up a commercial water treatment system which would produce about 1000 LPH of RO treated water at Skylark‘s Gurgaon site.

The water-treatment systems used in commercial facilities are different to those in small domestic RO units. The equipment should be able to process greater flow rates, operate longer hours and process different feed-water characteristics, and be easy to operate and maintain.

The treatment system was designed for a 1000 LPH commercial RO plant with appropriate pre-treatment stages for this project. The goal was to not only install RO membranes, but to design an entire treatment sequence that would safeguard the membranes and ensure consistent output.

The overall work involved in the installation comprised assessment of the area, equipment planning, plant fabrication and assembly, plant transportation, positioning of the plant equipment, plant plumbing connections, electrical connections, plant pretreatment setup, plant RO membrane installation, testing, plant flushing, plant trial operation and final plant commissioning.

The final product was a water-treatment system that satisfied the commercial need of Skylark with a convenient access path for future inspection and maintenance of the major components of the system.

Client Details

The project was for Skylark, Gurgaon as a client. It has EPC, mining, toll collection and highway maintenance as its major business segments.

The company’s operations feature large-scale infrastructure activities, and a significant employee base. Such an organisation needs reliable utility services capable of supporting the normal running of business.

One of these utilities is water-treatment infrastructure. An appropriate size commercial RO plant can process water at a central location, and the purified water can be stored for use as required at the facility, rather than using small purification units.

Thus the 1000LPH Commercial RO Plant was selected which proved to be a good solution for the site with a relatively small footprint for the system.

Project Location

The RO plant installed at Skylark, Gurgaon, Haryana. Their address in Gurgaon is: 267, Udyog Vihar, Phase IV, Gurgaon – 122015, Haryana, India.

One of the prominent commercial and industrial hubs of Gurgaon, Udyog Vihar is home to offices, manufacturing units, warehouses and corporate establishments in the various stages.

Water supply to commercial establishments in Gurgaon may be from various sources and the water quality may vary depending on the source and local conditions. Therefore, it is best to choose the water-treatment equipment based on the water’s feed-water quality, not just on the basis of its LPH rating.

Therefore, as a Commercial RO Plant Manufacturer in Gurgaon, our emphasis is on the capacity of the RO Plant and the number of treatment stages that will be required for a particular application as well as the quality of the water source.

Plant Capacity

The commercial RO system installed has a product water capacity of:

Parameter Value
Product Water Capacity 1000 Litres Per Hour (LPH)


This implies it is capable of delivering about 1,000 litres per hour of RO water under the plant’s operating and feed-water conditions.

Capacity must be determined based on a number of considerations such as:

Capacity Consideration
Daily treated-water requirement
Peak water demand
Number of operating hours
Available raw-water storage
Treated-water storage capacity
Feed-water quality
Membrane performance
Required product-water characteristics


A theoretical yield can be calculated: For a 1000 LPH plant, if it is able to work for 8 hours, then the theoretical output is about 8,000 litres. The theoretical production at the same time of effective operation is about 10,000 litres.

The actual production may change depending on the feed-water temperature, pressure, condition of the membrane, concentration of dissolved-solids, fouling, maintenance and other operating conditions.

This means that Skylark is able to deliver commercial scale water production with a 1000 LPH capacity, but not with a much larger treatment plant.

Treatment Technology

The key purification technology applied in the project is Reverse Osmosis (RO) together with the appropriate pre-treatment.

Reverse osmosis is a pressure driven membrane separation process. The water is pushed across a semi-permeable membrane, creating product water or permeate and reject water or concentrate, which is a concentrated stream.

The pretreatment decreases the loading rate on the membranes, fine filtration gives further protection against particulates, the high-pressure pump creates the pressure for membrane separation, and the RO membranes decrease the concentration of dissolved material in the product-water stream.

The plant can be systematically maintained and a practical solution for commercial water treatment is possible.

Influent Characteristics

An RO plant‘s performance is highly dependent upon the properties of the influent, or raw water entering the plant.

For commercial RO systems, some key feed-water parameters that are normally considered in designing and operating systems are:

Influent Parameter
Total Dissolved Solids (TDS)
Total hardness
Calcium and magnesium
Turbidity
Suspended matter
pH
Chloride
Alkalinity
Iron, where present
Hard Minerals (Silica, etc.)
Organic matter
Microbiological Condition


Treatment Process

The 1000 LPH Commercial RO Plant consists of a series of treatment units that work together in a coordinated manner.

1. Raw-Water Feeding

Raw water is initially delivered to the pretreatment part by the feed line. Flow of feed is essential as subsequent equipment relies on a steady supply of feed water.

2. Pressure/Media Filtration

The primary filtration section filters out suspended impurities and turbidity.

Particulate loading is reduced at this stage which leads to less loading of fine filters or RO membranes.

3. Activated Carbon Treatment

Activated carbon treatment is available to remove chlorine, odour and some organic material in feed water if needed.

Granular activated carbon is widely utilised in water treatment applications for the adsorption of taste and odour-causing compounds and a number of organic contaminants.

4. Antiscalant Dosing

If scaling has the potential to occur, controlled antiscalant dosing can decrease the growth of mineral deposits on membrane surfaces.

As scaling builds up it can decrease membrane output, increase differential pressure, and over time increase maintenance needs.

5. Micron/Cartridge Filtration

Water flows through fine cartridge filtration before going to the high pressure RO section.

This provides another protection to keep small suspended particles away from the membrane elements.

6. High-Pressure Pumping

This high-pressure pump raises the water pressure to the amount necessary for a good reverse osmosis.

The RO process is dependent on pressure and requires it to push water through the semi-permeable membrane.

7. RO Membrane Separation

Water is split into two streams in the membrane housings.

These are referred to as RO permeate, which flows through the membrane at much lower levels of many dissolved substances.

The second is the concentrate or reject stream that contains more of the substances that are rejected by the membrane.

The EPA also explains RO as generating a permeate/product water stream and a reject/concentrate stream.

8. Treated-Water Collection

The RO permeate is finally channeled to the intended treated water storage facility for distribution and use.

Major Equipment

Skylark Gurgaon‘s 1000 LPH Commercial RO Plant features all necessary equipment needed for a commercial water treatment system.

The main functional elements are:

Equipment
Raw-water feed arrangement
Feed-water pump
Pressure/media filtration system
Activated carbon filtration is used
Antiscalant dosing system
Micron cartridge filter
High-pressure pump
Commercial RO membrane elements.
Membrane pressure housings
Pressure gauges
Product-water flow monitoring
Reject-water flow monitoring
TDS/water-quality monitoring arrangement
Control panel
Valves and inter-connections pipelines
Treated-water outlet arrangement
Reject-water discharge arrangement


Equipment was set up both to be functional and accessible.

Maintenance or inspection of parts such as filter elements, dosing equipment, membrane housings, pumps and instruments requires regularity, particularly in a commercial RO plant, where accessibility is of paramount importance.

A quality commercial RO system should therefore be capable of yielding treated water, but also be designed to serve a long time.

Installation Process

The installation process was systematically conducted so that the RO plant is able to function after its commissioning.

A review of the available installation area and the selection of suitable locations for the RO skid and pretreatment equipment was the first step.

Wherever possible, working space was kept clear around the treatment units to enable routine changes of the filters, pressure checks and maintenance to be carried out conveniently.

Post equipment positioning, the raw water line was hooked up to the feed section and interconnections between the pretreatment components and the RO system were made.

The product-water piping and reject-water piping were not connected to each other so as to avoid mixing of the two streams.

Electrical connections to the feed pump and the high-pressure pump were then made, along with the feed pump, dosing system and control panel.

The installation team preperformed the following checks before starting the plant:

Pre-Startup Check
Pipe connections
Valve positions
Electrical connections
Pump direction
Filter installation
Membrane housing connections
Pressure lines
Conveying product and reject outlets
Potential leakage points


The process of installation was systematic which facilitated controlled startup and commissioning of the system.

Plant Commissioning

Commissioning of plants is the point where the installed equipment is tested as a whole water-treatment system.

Firstly, the 1000 LPH RO plant was flushed to prepare the filtration section and membrane section for normal operation.

Feed pump was then operated and then low pressure section was started in a controlled way.

The technical team was monitoring the operating condition such as feed-flow, pressure, product-water generation, reject-water discharge etc. during the commissioning.

Leaks were tested and the pressure and operation of the pumps were monitored for any abnormality.

The plant was slowly ramped up to operating conditions to avoid unnecessary hydraulic stressing of the plant.

The treated water production rate was verified against the desired plant capacity of 1000 LPH

There was also basic operational guidance provided in the commissioning process, such as:

Operational Guidance Topic
Plant startup
Plant shutdown
Pressure observation
Product-water monitoring
Cartridge-filter replacement
Chemical dosing
Membrane maintenance
The detection of abnormal flow and/or pressure.
Preventive maintenance requirements


Following successful testing and adjustment, the plant was made ready for routine operation.

Treated Water Reuse

The treated water from the plant can be stored in a separate treated water tank until such treated water is required for Skylark‘s own water usage.

Depending on the quality needed for each application, treated water can be used for:

Treated Water Use
After required final treatment and verification, drinking-water supply.
A full pantry and kitchen will be supplied.
A well-equipped kitchen and pantry will be provided.
Office utility requirements
Appropriate equipment or process applications
Other purposes with relatively lower TDS water


The actual end use should always determine the required final water-quality specification.

If treated water is to be used for human consumption, then hygienic storage and disinfection as required, and routine laboratory testing should be observed. IS 10500:2012 specifies requirements for drinking water in India, which can be used to evaluate the water quality parameters relevant to it.

The reject water from RO system should be disposed properly. The EPA states that the concentrate stream will include salts and other materials that are trapped by the membrane, and therefore, should be treated appropriately before being discharged or managed.

Only the reject water’s quality and the needs of the intended non-potable use should be taken into account when considering possible reuse.

Results and Performance

The successful installation and commissioning of the 1000 LPH Commercial RO Plant at Skylark Gurgaon has enabled the facility to have a dedicated on-site water-treatment system which can provide about 1,000 litres of RO water per hour under its specified operating conditions.

The project was successful in achieving the project objective of having a stable commercial scale production of treated water using a structured pretreatment and membrane-separation process.

The main results are:

Result Description
Well defined treated water production The plant offers treated water as a separate source of water rather than relying only on smaller point-of-use water purifiers.
Commercial scale capacity A rated capacity of 1000 LPH is considered a reasonable scale of production/capacity to install.
Removal of dissolved mineral content RO Membrane technology is used specifically for the removal of a variety of inorganic constituents and dissolved solids.
Pretreatment for membrane protection Proper filtration prior to the RO stage can minimise fouling and plugging, which are known operational issues of membrane treatment.
Easy system monitoring Pressure monitoring points, flow monitoring points and water-quality monitoring points allow system operators to monitor plant operation during regular operation.
Sustainable equipment layout System installed to allow convenient access to consumables and major equipment needing routine maintenance.


This overall installation thus provides both 1000LPH purification capacity and a complete commercial treatment solution including pretreatment, membrane separation, monitoring and the collection of treated water.

Customer Feedback / Testimonial

Installing and commissioning processes were executed professionally, keeping in mind operational ease and system reliability.

After commissioning, basic maintenance and operation of the plant was demonstrated to the concerned personnel.

As a result of not having received an independently verified customer quotation for this case study a direct statement must not be attributed to Skylark without permission.

The installation and commissioning of the 1000 LPH Commercial RO Plant in our Gurgaon facility is done professionally and the plant is functioning well as per our water treatment requirement and the technical team gave us proper guidance about the operation and routine maintenance of this plant.

Looking for a trustworthy Commercial RO Plant Manufacturer in Gurgaon for your office, factory, hotel, school, hospital, warehouse, commercial complex or industrial plant?

Some of the points to consider in a well-designed system:

Design Consideration
Raw-water quality
Daily water requirement
Peak demand
Required treated-water quality
Available operating hours
A space that allows for the installation of equipment.
An area that can accommodate equipment.
Pretreatment requirements
Water storage
Maintenance requirements
Intended treated-water application


We supply complete solution from the designing to manufacturing, installation and commissioning of RO Plant for Commercial applications in Gurgaon for various capacities.

Commercial RO plant can be designed in various capacities like:

Available Capacities
500 LPH
1000 LPH
2000 LPH
3000 LPH
5000 LPH
10,000 LPH and customised capacities


Our services include water-treatment requirement assessment, system design, equipment selection, RO plant manufacturing, installation, commissioning, operator guidance, membrane replacement, filter replacement, troubleshooting and preventive maintenance support.

Our track record of delivering water-treatment projects from conception to commissioning, such as the 1000 LPH Commercial RO Plant at Skylark Gurgaon, showcases our capabilities in delivering commercial water-treatment projects.

If you require a dependable Commercial RO Plant Manufacturer in Gurgaon, contact our technical team.

Read some interesting information for the Effluent Treatment Plant Manufacturer in Faridabad

Conclusion

The 1000 LPH (Commercial RO Plant) installed at Skylark Gurgaon is testament to the significance of selecting the right plant capacity, pretreatment, membrane technology and professional commissioning under one umbrella solution.

Skylark is an infrastructure and engineering company that has offices in EPC (Engineering, Procurement, and Construction) and other sectors such as mines, tolls, and highways.

When a commercial facility is being used, the reliability of the water treatment will not only be determined by the rated capacity of the RO plant but also by factors such as incoming water condition, pretreatment performance, proper operating pressure, membrane condition and periodic maintenance.

The 1000 LPH system meets these needs with a series of systematic treatment processes that involve raw-water feeding, pretreatment, fine filtration, high-pressure pumping, and RO membrane separation and output of product water.

While RO is an established membrane separation process for decreasing dissolved solids and a host of other contaminants, system pretreatment and concentrate management are important factors in proper system operation.

As a Commercial RO Plant Manufacturer in Gurgaon, the project has also provided another hands-on example to understand our capability to deliver commercially appropriate water-treatment systems based on capacity, water quality, and operational requirements.

For businesses planning a new RO installation or upgrading an existing treatment facility, a properly engineered commercial RO plant can provide a dependable, scalable and manageable source of treated water for long-term use.

Contact Netsol Water at:

Contact Details
Phone +91-9650608473
Email enquiry@netsolwater.com


What-are-the-Applications-of-Commercial-Water-Softeners-2.webp

August 13, 2026by Netsol Water

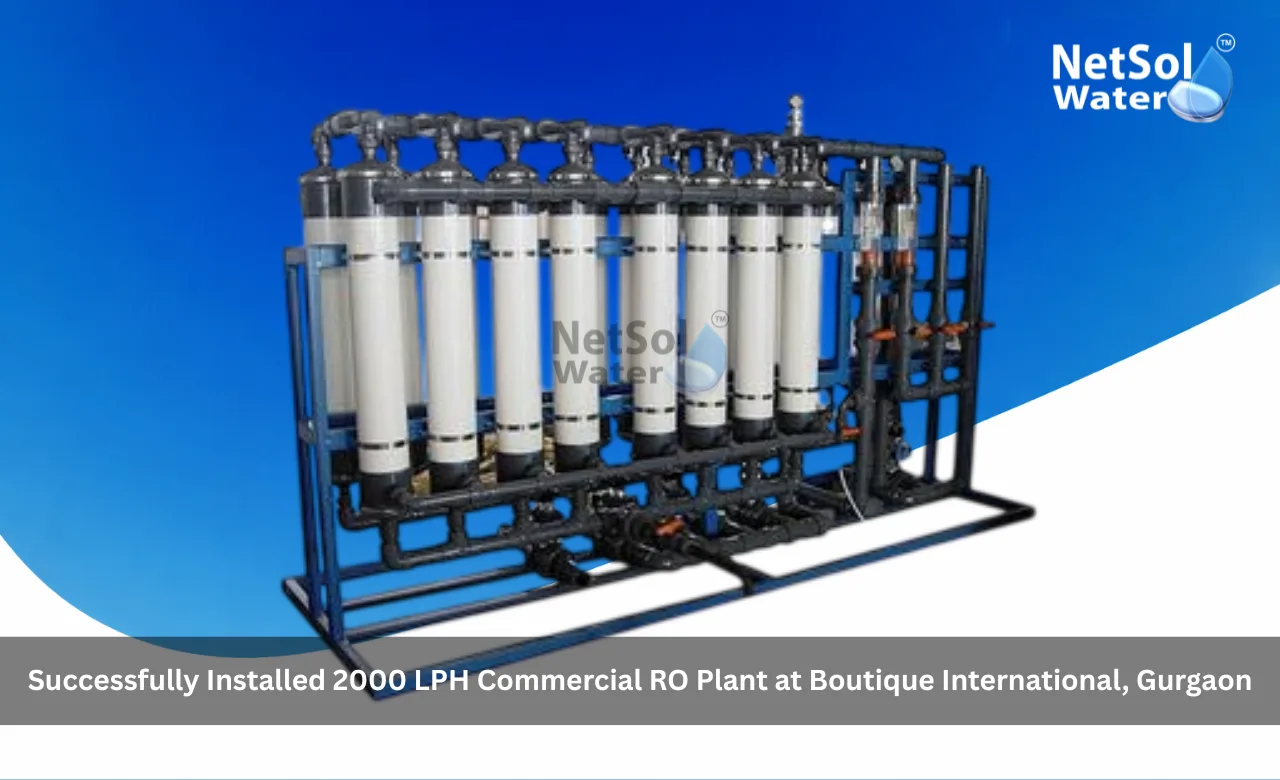
Successfully Installed 2000 LPH Commercial RO Plant at Boutique International, Gurgaon

Consistently treated water is important for commercial and industrial operations that rely on water consistently and continuously. The composition of raw water, including dissolved salts, hardness, suspended matter and other water properties, can vary and impact the usefulness of the raw water for drinking, utilities, processes. The combination of appropriate pretreatment with membrane purification would present an effective solution provided by a suitably designed commercial RO plant. The RO plant of 2000 LPH Commercial RO Plant was successfully installed and commissioned at Boutique International, Gurgaon and they were provided with a reliable source of treated water of about 2000 litres per hour based on the operating conditions provided.

Boutique International is a vertically integrated garment Export Company based in Gurgaon. It has knitting, embroidery, printing and other apparel manufacturing activities and is manufactured in its facility in Gurgaon.

The project reflects our expertise as a Commercial RO Plant Manufacturer in Gurgaon and most importantly, designing treatment systems as per the plant requirements, feed water quality available at the site, output capacity required and operational needs of the client.

Project Overview

The aim of the project was to supply a viable commercial scale water treatment plant for Boutique International that will produce 2,000 litres per hour of treated water.

The quantity of water required is not the only factor to consider before installing a commercial RO plant, the characteristics of the feed water must also be taken into account. RO membranes are primarily meant to separate the dissolved contaminants from water, and pretreatment is used to abate suspended particles, scaling, etc., that can impact the membrane.

Thus, it was decided that the solution will be an integrated treatment system instead of a standalone RO membrane unit. The removal of material from the raw water, generating the pressure, separation in a membrane, monitoring and treating the water out of the membrane were all taken into account, in order to ensure the plant’s operation under commercial conditions.

The project involved site assessment, capacity planning, equipment selection, system fabrication, transportation to the facility, installation, electrical and plumbing connections, flushing, trial operation, parameter adjustment and final commissioning.

The system once installed, gives Boutique International a separate RO water-treatment system of 2000 LPH for assured everyday operation.

Client Details

Boutique International is a garment manufacturing and export company from Gurgaon, Haryana, which was the client for this project.

Boutique International calls itself the star export house for apparel brands in the United States and Europe recognised by the government. The company claims its manufacturing process is vertically integrated, that is all the process from yarn to finished goods are done at the company’s facility. It has the facilities of circular knitting, flat knitting, embroidery and printing.

Infrastructure reliability is crucial in an organisation that operates at this level. All water-treatment facilities need to be able to deliver the treated water needed in the required quantity, and not make routine operation and maintenance unnecessarily complex.

The need was thus for a commercial system, not a small domestic purification system. The chosen capacity of 2000 LPH was deemed to be an appropriate balance of the water demand, operational capability and future utility.

Project Location

The commercial RO plant was installed in Boutique International, Plot No. 553, Pace City 2, Gurgaon, Haryana – 122016.

The town Gurgaon or Gurugram has emerged as a very important business and industrial hub in Delhi NCR region. The nature of water may vary greatly depending on whether it comes from a municipal water supply, a ground water well or a tanker.

So, it is not right to choose commercial RO plants only on the basis of the rated production capacity. The characteristics of the feed-water, treatment time, and pretreatment time, storage facilities, and the water quality to be expected after treatment, must also be taken into account.

As a Commercial RO Plant Manufacturer in Gurgaon, we therefore do not follow a one design fits all principle instead we ensure that the treatment configuration is personalized to fit the actual site needs.

Plant Capacity

The rated treated water production of the installed plant is: 2000L/h (Litres per Hour)

Parameter Value
Rated Treated Water Production 2000 L/h (Litres per Hour)


The system can generate around 2000 litres of RO treated water in an hour when operated at its full capacity. The actual daily production will vary depending on the operating time, feed-water condition, membrane performance, maintenance condition, and water need of the facility.

The theoretical production capacity of a 2000 LPH plant is, for example, about 16 000 litres during a period of 8 effective production hours. But the plant does not have to run around the clock—operation can be synchronized with treated-water storage and actual consumption.

The capacity selected is enough for commercial scale output, while treated water production and storage will follow the facility’s production schedule.

Treatment Technology

The RO process with the proper pre-treatment technology represents the main treatment process adopted in the plant.

Reverse osmosis is a method that uses pressure to push feed water through a special membrane to extract some of the water. This results in two streams of water, the purified water or permeate, and a more concentrated stream of water called the concentrate or reject water, which contains the dissolved substances that were not purified. RO is a membrane-separation technology capable of separating a wide spectrum of dissolved contaminants and salts.

But RO membranes should not be fed inadequately treated feed water. Scaling compounds, suspended matter, and chlorine and organics may have an impact on membrane life and performance.

Influent Characteristics

Incoming water quality is one of the most crucial factors to consider while designing any commercial RO plant.

Dissolved salt, minerals which form hardness, suspended solids, turbidity, chlorine and organic matter can be found in varying amounts in commercial feed water.

The treatment system was designed to address the key parameters, which typically affect commercial RO operation, such as:

Total dissolved solids, hardness, suspended particles, turbidity, scaling potential and contaminants that could impact the performance of the membrane.

Pretreatment is particularly important because it is not only to enhance the quality of the feed water, but to avoid fouling or scaling of RO membranes before they are used. DuPont says proper pretreatment ensures good RO performance and that the pretreatment required is a function of the chemistry of the raw water and the purpose of the treated water.

If the water is to be used for drinking, it is prudent to test its final quality with the right tests. The drinking-water specification of Bureau of Indian Standards (BIS) IS 10500:2012 suggests that the acceptable range for TDS is 500 mg/L and permissible range is 2,000 mg/L without any source. This same standard establishes acceptable hardness levels between 6.5 and 8.5, as well as limits for chloride, fluoride, nitrate and many other parameters.

BIS IS 10500:2012 Parameter Value
TDS – Acceptable Range 500 mg/L
TDS – Permissible Range (No source) 2,000 mg/L
Acceptable Level 6.5 to 8.5


Treatment Process

The 2000 LPH Commercial RO Plant is designed to pass through a series of treatment stages that help prevent damage to the membranes and assure a consistent product-water quality.

The raw water is pumped into pretreatment section first. The suspended matter is filtered out initially and the load is reduced to the later filter elements.

The water is then filtered through media filters. This stage is useful in controlling turbidity, suspended impurities, colour, odour and substances which may affect the operation of the RO membrane depending on the nature of the raw water.

When incorporated, activated carbon treatment acts as an important barrier to protect the membranes from the presence of chlorine and some of the organic compounds before they reach the membranes. This is especially important since improper feed-water conditions can adversely affect the performance of the membrane.

Fine cartridge filtration is another physical barrier to small suspended particles that is offered before membrane treatment.

A high-pressure pump is used to pump the pretreated water to the RO section. Reverse osmosis requires pressure due to the natural tendency of dissolved salts to move across a semi-permeable membrane.

The feed flows inside the RO membrane housing, splitting into a product water and a concentrate stream. Water passing through the membrane becomes the product water and continues to treated water storage, while a higher concentration reject water stream removes a significant amount of the dissolved substances separated.

During operation, flow and pressure parameters are monitored along with water quality parameters to detect any abnormal conditions and correct them.

Major Equipment

The main components needed for the pretreatment, membrane purification, monitoring and controlled operation were set up in the commercial RO system.

The major functional equipment consisted of:

Equipment
Arrangements for feeding raw water and water feeding pump.
Pressure/media filtration system
Activated Carbon Treatment, when needed based on feed-water conditions
Antiscalant dosing arrangement
Micron/cartridge filtration
High-pressure RO pump
Monitoring of product-water and reject-water flow.
Temperature and operating controls
Electrical control panel
Interconnection of piping, fittings and valves.
RO-treated-water outlet/storage connection


The equipment size was scaled to the product water requirement of 2000 LPH and operating condition.

The design also took ease of operation and maintenance into account since the installation of successful commercial water treatment relies not only on a good installation, but also regular monitoring, changing filters, maintaining membranes and timely servicing.

Installation Process

Installation started by surveying the plant space and existing utility services.

RO skid and pretreatment equipment were located for good accessibility for future maintenance and filter change out. The positioning of equipment is especially critical in commercial installations as the layout could become unnecessarily complicated to service the equipment routinely.

The inlet plumbing for raw water was connected to the pretreatment system, and connections between the treatment stages were made. Careful checks were made on the high pressure line, membrane housings, product-water outlet and reject water discharge line.

Pumping and dosing equipment and the control panel were electrically connected. The system was then checked for correct positioning of the valves, piping alignment and leaks.

With mechanical and electrical connections checked, individual system sections were ready for flushing and start-up.

Installation method – The approach was designed to reduce disruption to the client’s existing operations and provide easy access to the water-treatment equipment for future maintenance.

Plant Commissioning

Commissioning is one of the most important phases of a commercial RO project as good installation does not guarantee good operation.

The system was initially flushed to clear any loose material that may have been encountered during installation, and to ready the filters and membrane system for use.

The pumps were then gradually started and increased pressure applied in a controlled manner. The feed-water flow, product-water flow and reject-water flow were monitored as the system approached normal operating conditions.

The team inspected the system for leaks, abnormal pump performance, pressure and flow blockages during the commissioning. RO operating parameters were optimized for stable operation, while avoiding undue stress to the membranes.

The product-water output has been validated with the desired capacity of the plant, namely 2000 LPH subject to the condition of operating conditions and the quality of feed-water.

Routine startup and shut down, pressure monitoring, cartridge-filter replacement, chemical dosing, membrane cleaning indicators and preventive maintenance were also discussed with the operators.

Treated Water Reuse

The water that is treated through RO system can be stored in a separate tank, and can be pumped to specific locations where the facility needs low TDS water.

RO treated water can be used to prepare drinking water, to meet pantry needs, for utility uses and for appropriate process water needs based on the client’s internal water-management plan, where controlled dissolved-solids levels are desired.

For any end use, the distribution should be the same as the required water quality specification. If the water is used for drinking, the proper post-treatment, hygienic storage and regular microbiological and chemical testing are essential.

Concentrate management is also responsible for RO concentrate. Facilities may consider whether they can make a suitable non-potable use of the reject-water stream depending on its quality and the local needs. Testing and the needs of the intended use should be considered when making a reuse decision.

Results and Performance

The installation and commissioning of 2000LPH Commercial RO Plant at Boutique International, Gurgaon was a great success, it gave the facility its own high capacity treatment system to produce purified water there.

The main aim of the project, which was to set up a reliable RO water production system with a rated capacity of around 2000 litres per hour was achieved.

After commissioning, the stable operation of the system with controlled feed pressure, product-water generation, and reject flow were identified. The RO membrane stage achieved high removal of dissolved mineral matter from the feed water, and pretreatment prevented particulate and scaling loading of the membrane system.

The primary operational advantages of the installation are the assured commercial scale water production, reduced reliance on small-scale purification units, ability to control the availability of treated-water, improved management of the dissolved solids and hardness, and the plant configuration which allows for easy monitoring of system performance and for routine service.

RO membrane technology is a proven technology for commercial and industrial water treatment. Commercial RO membranes are utilized in a wide variety of applications, from restaurants and hotels to medical and scientific facilities.

The finished project provided Boutique International with a new facility water-treatment asset on top of its current facility infrastructure.

Customer Feedback / Testimonial

Installation was finished with special consideration for the performance of the plants, ease of access and ease of operation. The system was tested during commissioning and the operating procedures were discussed to the facility staff.

The 2000 LPH Commercial RO Plant has been installed at our facility in Gurgaon and we are pleased with the professional installation and commissioning of the RO Plant. The RO Plant is working as per our water-treatment requirement and the Technical team provided us the required support during installation, testing and handover.

In execution of this project success highlights the needs of using proper plant capacity together with proper pretreatment, reliable equipment, proper installation and technical support.

Call to Action

When it comes to selecting the best commercial RO Plant Manufacturer in Gurgaon, the decision is crucial if you have a factory, office, hotel, hospital, school, institution, warehouse or commercial facility which needs a reliable water-treatment plant.

A commercial RO system should be configured based on your specific water analysis, your daily water demand, the number of hours the system will be used, available space and the specific quality of water you want to produce—rather than just picking a capacity from a standard capacity chart.

We design, manufacture, install and commission the commercial RO plants for various water needs and operating conditions. The treatment configuration can be designed depending on the application and feed-water characteristics, if you need a 500 LPH, 1000 LPH, 2000 LPH, 3000 LPH, 5000 LPH or a customised commercial RO plant.

Available Capacities
500 LPH
1000 LPH
2000 LPH
3000 LPH
5000 LPH
Customised commercial RO plant


Services offered range from requirement assessment to designing the water-treatment system, selecting the equipment, manufacturing the RO plants, commissioning and training the operators, troubleshooting and providing equipment maintenance support and replacement of consumables and membranes.

The installation of a 2000 LPH Commercial RO plant at Boutique International, Gurgaon, showcases our capability to take on commercial water-treatment projects from system design to final commissioning.

Looking for a reliable Commercial RO Plant Manufacturer in Gurgaon? Contact us today and speak about your water requirement.

Provide us with your raw-water test report and daily water demand and our technical team will be able to suggest the capacity and treatment configuration of the RO plant required for your facility.

Read some interesting information for the Commercial RO Plant Manufacturer in Faridabad

Conclusion

The Boutique International project did not just use the RO membrane but included all the components of a complete treatment process, such as pretreatment, fine filtration, pressure generation, membrane separation, monitoring, commissioning and operational guidance. This is significant because the performance and life of the membrane is highly dependent on the quality of the water treated and the quality of pretreatment.

The system installed has a capacity of 2000 litres per hour and enables the Boutique International‘s Gurgaon facility to have a significant treatment water production capacity with the help of installed system. Reliable long term operation is also achieved through correct installation, system commissioning and equipment arrangement which is easy to access.

If any organisation is planning to install a similar RO Plant in Gurgaon, it is advisable to choose a Commercial RO Plant Manufacturer in Gurgaon to ensure that plant capacity, water chemistry, pretreatment and operational requirements are all taken care.

A business where treated water availability is a constant requirement can turn to a professionally engineered commercial RO plant for a reliable solution that is scalable and can provide them with the water they need.

Contact Netsol Water at:

Contact Details
Phone +91-9650608473
Email enquiry@netsolwater.com


What-are-the-Applications-of-Commercial-Water-Softeners-1.webp

August 12, 2026by Netsol Water

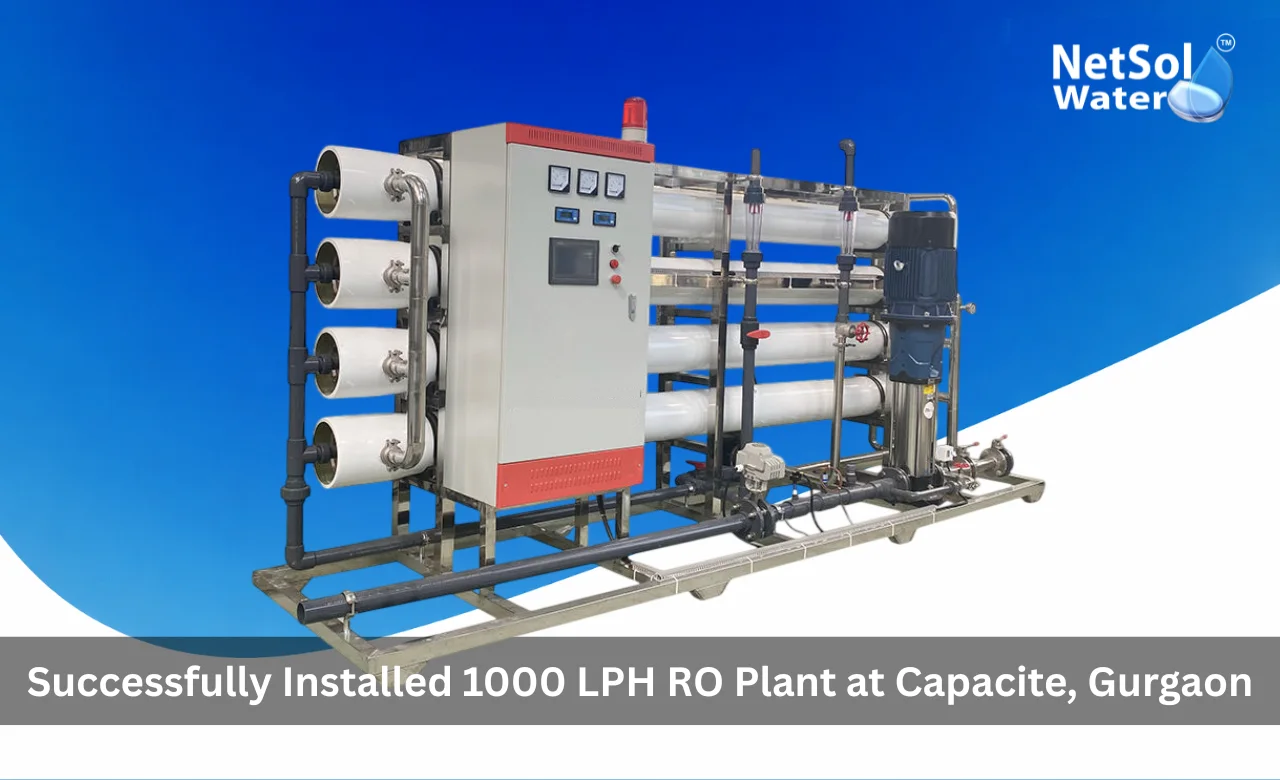
Successfully Installed 1000 LPH RO Plant at Capacite, Gurgaon

Purified water is important to commercial buildings, offices, construction sites, industrial sites, institutions and large workplaces. Raw water may contain dissolved salts, hardness, suspended particles, unpleasant taste or smell and other contaminants that are not desirable for direct use. A properly designed RO plant provides an effective solution by combining pre-treatment, membrane separation, process control, and water-quality monitoring.

Netsol Water has installed a 1000 LPH RO Plant at Capacite, Gurgaon, which is a commercial and industrial water purification plant that can produce high purity water. The installation illustrates the ability of the right size RO plant to satisfy the daily purified water need of a commercial water facility in a compact and manageable treatment setup.

This project serves as an excellent example of how plant capacity, treatment stages, equipment selection, installation, and commissioning can be linked to create an effective water-treatment system.

Project Overview

The project was the installation of Capacite 1000 litres per hour (LPH) RO plant in Gurgaon, Haryana. The primary goal was to obtain a dependable system for producing purified water on site for the facility rather than relying on the untreated incoming water or the supply of purified water from outside.

The product water capacity for a 1000 LPH plant is about 1,000 litres per hour per operating hour. The actual amount of production possible depends on the number of hours the plant is operating, the quality of the raw water, the feed pressure, the condition of the membranes, their maintenance, and the plant’s demand.

Netsol Water‘s commercial RO solutions rely on several treatment stages and not just the RO membrane. It has been documented that its commercial RO process encompasses the removal of suspended solids, treatment with activated-carbon, fine cartridge filtration, high pressure pumping, membrane separation, management of reject water, dosing, instrumentation and provisions for membrane cleaning.

The Capacite project is an important installation for Netsol Water as it further strengthens its reputation as a leading Commercial RO Plant Manufacturer in Gurgaon and the Delhi NCR region.

Client Details

The client for the project was the Capacit’e Infraprojects which is a company that is engaged in construction activities. It defines its sectoral presence as total contracting, general contracting and design-and-build services for such projects as high-rise buildings, super-high-rise buildings, commercial and office buildings, institutional buildings, hospitals, hotels, data centres, industrial buildings, mass housing, and other large projects.

Water availability becomes significant for the construction and commercial development, as well as infrastructure sectors, not just in providing drinking water, but also some functions within project offices and facilities.

A commercial RO system must then be tough enough to use regularly, and be easy to operate and maintain.

Project Location

The RO plant was setup in Capacite, Gurgaon. Gurgaon is among the important commercial and corporate cities of Delhi-NCR, which has a large number of offices, housing societies, hotels, institutions, construction sites, industrial units, etc. These facilities may need special water treatment facilities when the quality of the water is not satisfactory for the intended purpose.

Netsol Water in particular in Gurgaon offers commercial RO solutions and emphasizes the need for choosing a plant based on the number of users, water source parameters, water required capacity, installation site and maintenance needs.

Plant Capacity

The RO plant installed has the capacity of:

Parameter Value
Plant Capacity 1000 LPH
Equivalent Product-Water Output 1 m³/h


This is a capability that makes the system appealing to facilities that need a significant amount of purified water over the course of a workday, but the amount is not too much to handle.

The rated capacity, for instance, refers to the theoretical capacity that the plant can achieve, for example, at 8 hours operating time it can deliver around 8000 litres, at 10 hours it can deliver around 10000 litres subject to actual operating conditions and availability of feed-water.

The sizing of plants is an important engineering design decision. Both an undersized and an oversized RO plant can have drawbacks in terms of meeting peak consumption and/or operating the plant efficiently. The 1000 LPH capacity offers a realistic compromise between capability, size, usage and commercial water demand.

Treatment Technology

RO is the main treatment technology being utilized in the project.

RO is a membrane separation technique where the pretreated water is subjected to pressures and allowed to flow through semi-permeable RO membranes. The water molecules traverse the membrane as purified permeate while a large percentage of the dissolved salts and other constituents that are not allowed to pass through are left on the concentrate side of the membrane and exit through the reject line.

But this successful RO performance relies on proper pre-treatment. If the untreated water is fed directly to RO membrane, it may lead to fouling, scaling, pressure demand, frequent cleaning and deterioration of the membrane.

The commercial RO treatment unit by Netsol Water, therefore, includes several treatment mechanisms, namely the sand filter, the activated carbon filter, the micron filter, the high pressure pump, the membrane, the dosing system, the instrumentation and the cleaning system.

This multi-stage approach is designed to help protect and stabilize the system performance of the membrane.

Influent Characteristics

One of the key components of commercial RO design is influent assessment. The following are some of the parameters that are usually assessed prior to the finalization of an RO system:

Influent Parameter
Total Dissolved Solids (TDS)
Electrical conductivity
pH
Total hardness
Calcium and magnesium
Chloride
Sulphate
Alkalinity
Turbidity
Suspended matter
Iron, where relevant
Organic matter


Depending on the water source, microbiological contamination occurs.

Water-quality parameters like pH, EC, TDS, total hardness, calcium, magnesium, alkalinity, chloride, sulphate, nitrate, fluoride, sodium and potassium are also listed as important water-quality parameters in Haryana’s water quality testing infrastructure.

This treatment system was designed to solve the larger problem of the conversion of the incoming water into a reliable high purity product-water supply, for the Capacite project, rather than simply basic filtration.

Treatment Process

The treatment sequence is in accordance with the multi-stage treatment principle proven in the commercial RO systems of Netsol Water.

A system for removing dissolved solids from raw water that includes feed pump, pressure sand filter, activated carbon filter, micron filter, scale control, high pressure pump, RO membranes, storage and use.

Stage 1: Raw Water Feeding

Water is pumped into the plant by means of a feed pump at the appropriate flow and pressure into the pre-treatment system.

Stage 2: Pressure Sand Filtration

Water is first filtered in the sand filter stage. This will help to remove any suspended solids or larger particulate matter that might enter the cartridge filters and/or RO membranes.

Stage 3: Activated Carbon Filtration

Activated-carbon treatment is the next step. Activated carbon is part of its commercial sequence for dechlorination by Netsol Water. Another property that can be modified by carbon treatment is the water properties, by removing some of the organic compounds that cause undesirable taste and odour.

Stage 4: Micron Cartridge Filtration

Fine filter before high pressure section, with a micron filter. It is a secondary barrier to smaller suspended particles.

Stage 5: Dosing and scale protection

The use of the proper chemicals allows control of scaling at the surface of the membranes. Often, the membrane is scaled and this can lead to lower permeate flow and higher operating pressure, which require protection for the long-term stable operation.

Stage 6: High-Pressure Pumping

The pre-treated water is pressurised by the high-pressure pump. The purified water must be pushed through the RO membrane against the osmotic pressure which requires adequate pressure.

Stage 7: Reverse Osmosis Membrane Separation

The water is split into two streams within the membrane system:

Stream Description
Product water Water that has been treated to be used for various purposes.
Rejected/Concentrated Water with a greater concentration of rejected dissolved materials.


The permeate is directed to a storage tank or used as is, with the concentrate being directed to the reject or recycle system, depending on the plant design. Netsol Water refers to the same general process when referring to its commercial RO systems.

Major Equipment

The key equipment of a commercial RO system of this kind is:

Equipment
Raw-water/feed pump
Pressure sand filter
Activated carbon filter
Micron cartridge filter housing
Chemical/anti-scalant dosing arrangement
High-pressure RO pump
RO membrane housings
Reverse osmosis membranes
Flow meters
Pressure gauges
Conductivity/TDS monitoring instruments
Level-control switches
Control panel
Product-water line
Reject-water line
Installing piping and valves between different units.
Connecting pipes and valves between units.
Structural/skid arrangement


Netsol Water specifically records pressure gauges, flow meters, conductivity sensors and level switches for monitoring the performance of commercial RO systems and provides a description of a CIP system for maintaining the membranes.

These components combine to give not just filtration, but an environmentally regulated water-treatment process.

Installation Process

Installing an RO plant is no simple task; it must be done successfully. Mechanical, Electrical, Hydraulic, and Control components should function in a coordinated manner.

Netsol Water has confirmed success with 1000 LPH installation on the Capacite project.

A commercial structured RO installation would involve determining the space for the plant, positioning the filtration vessels and the RO skid, installing pipelines for raw water and product water, routing the reject line, connecting the pumps and the control panel, instrumenting and installing dosing lines, inspecting valves and pressure points, and ensuring product-water storage.

After mechanical erection pipelines and electrical connections are checked prior to controlled plant start-up.

This is especially crucial for organizations choosing a Commercial RO Plant Manufacturer in Gurgaon, as product supply without proper installation and commissioning could lead to varying plant performance.

Plant Commissioning

Commissioning is a process that transforms an installed RO plant to an operating treatment plant.

The commissioning process includes feed-water availability, correct pump rotation and pressure, flushing of the treatment system, checking filters, setting chemical dosing, checking for leakages, checking flow through the RO membranes, observing permeate and reject streams, checking instrumentation and automatic controls.

Pressure, flow, conductivity and water-quality behaviour are monitored during initial operation. Stable plant conditions can then be obtained by making adjustments.

Netsol Water has successfully completed many commercial RO installations, and all of these are instrumented to track both water quality and operating conditions, such as pressure gauges, flow meters, conductivity sensors and level switches.

The installation at Capacite is the successful completion of going from the equipment deployment stage to an operational purification system of 1000 LPH.

Treated Water Reuse and Utilisation

The design of the RO plant was aimed to produce high purity water for commercial and industrial use, and Netsol Water‘s project announcement was dedicated to the industries, offices, and commercial complexes.

Purified RO water can have applications where controlled water quality is required at a facility like Capacite provided the final water specification for the product is acceptable and the internal water-distribution system is acceptable.

Producing purified water on site, instead of having to bring the purified water into the site, may also help to minimise reliance on external supply of purified water, and enable the site to have more control over the water supply for the day.

Quality of the RO reject stream should always be managed based on the site requirements and quality of the RO reject stream. Where technically feasible, reject water can also be assessed for non-potable purposes, rather than be needlessly wasted.

Results and Performance

The successful installation of a rated 1000 LPH commercial and industrial RO plant at Capacite, Gurgaon, was the main outcome of the project.

The key results of the major project are:

Result
The installation of an on-site water purification system is made possible.
Dedicated water purification system on-site is enabled.
Purified-water production capacity of 1000 LPH (litre per hour) rated water.
1000 LPH (litre per hour) rated water for purification.
Treatment in multiple stages instead of one stage
The protection of RO membrane pre-treatment.
The separation of concentrated reject water and purified permeate.
Operational monitoring is provided.
A small system for commercial applications
Minimized reliance on untreated water supply for purified water uses
A treatment plan that is systematic and can be maintained and serviced over time


Customer Feedback and Project Acceptance

The importance of this ongoing relationship is that acceptance of a project in the commercial water-treatment industry involves not just providing equipment, but also engineering services, installation, service responsiveness, and confidence in ongoing support.

The Capacite is thus an important reference project for companies looking at the Commercial RO Plant Manufacturer in Gurgaon, Netsol Water.

How Netsol Water is Considered as a Leading Commercial RO Plant Manufacturer in Gurgaon?

The first step in plant selection is not necessarily to look at price or nominal capacity, but to consider what the requirement for the water is.

Netsol Water is producing commercial RO plants in various capacities and states and claims to offer customisable systems as per the customer’s requirement. It has documented treatment process that includes pre-filtration, activated-carbon treatment, cartridge filtration, high-pressure RO membranes, dosing, instrumentation and membrane-cleaning provisions.

Netsol Water also covers Gurgaon in the list where it supplies water-treatment plants and also provides commercial RO plants for various applications such as industries, commercial water plants, institutions, housing societies, hostels, restaurants, hospitals etc.

The successful installation of a 1000 LPH Commercial RO Plant in Capacite is a testament to Netsol Water‘s ability to transform a commercial water requirement into a treatment solution that is installed on-site.

Read some interesting information for the Sewage Treatment Plant Manufacturer in Faridabad

Call to Action!

When your office, commercial complex, hotel, hospital, educational institution, housing society, construction project or industrial facility needs a reliable RO water-treatment system, Netsol Water has the answer to find a plant of your choice that meets your raw water quality, required purified water capacity, operating hours, available installation space, and intended water application.

Selecting the right system configuration can provide you with better water quality and save downstream applications while also ensuring a reliable supply of purified water, whether you need a 500 LPH, 1000 LPH or a higher capacity commercial RO plant.

Are you searching for a reputed Commercial RO Plant Manufacturer in Gurgaon?

For consultation, water analysis, selection, design, manufacture, installation, commissioning and post installation support for water systems contact Netsol Water.

Contact Details
Call +91 9650608473
Email enquiry@netsolwater.com