RO Plant Commissioning - Sewage Treatment Plant Manufacturers

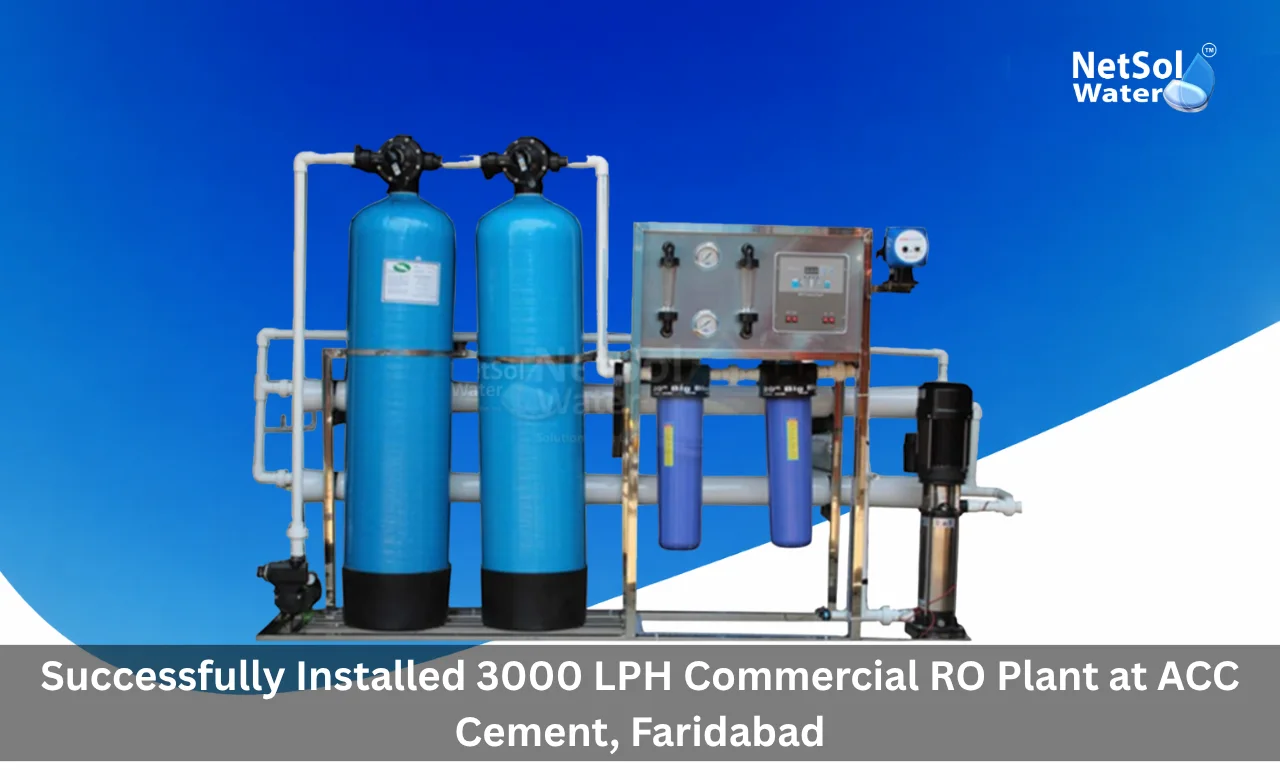
Successfully-Installed-3000-LPH-Commercial-RO-Plant-at-ACC-Cement-Faridabad.webp

September 21, 2026by Netsol Water

Successfully Installed 3000 LPH Commercial RO Plant at ACC Cement, Faridabad

Water quality plays an important role in maintaining suitable water use across industrial and commercial facilities. When incoming water contains unwanted dissolved salts and other impurities, the facility needs a treatment plant that can produce water suitable for its intended use. The requirement becomes more important when the plant needs a steady supply of treated water for routine operations. In this project, ACC Cement, Faridabad required a commercial RO plant to address its water treatment needs. We completed the installation of a 3000 LPH Commercial RO Plant for the facility.

The project focused on providing a treatment solution that could process incoming water through reverse osmosis and supply treated water at the required plant capacity. A 3000 LPH system offers a defined treatment rate that can support planned water requirements when the operating conditions match the design basis. The installation also required proper placement of the treatment equipment and suitable system connections so that the plant could operate as an integrated unit.

The project demonstrates how a carefully selected RO plant can support water treatment requirements within an industrial facility. It also reflects the role of experienced execution in taking a treatment system from installation through commissioning and regular operation.

Project Overview

A water treatment project becomes useful only when the treatment capacity and process meet the actual requirement of the facility. For that reason the planning stage must focus on the purpose of the system and the quality of water that needs treatment. In the Faridabad installation the client required an RO-based treatment plant with a capacity of 3000 litres per hour. The project therefore focused on the installation of a commercial RO system that could provide treated water at the specified production rate.

The objective was to establish a dedicated water treatment setup that could process the incoming water through reverse osmosis. RO treatment works by using pressure to move water through a semi-permeable membrane. The membrane allows water to pass while rejecting a significant portion of dissolved substances and other unwanted components. This makes RO suitable for applications where dissolved impurities need to be reduced rather than simply removed through basic physical filtration.

The scope of the project included the installation of the treatment plant at the client’s facility and the necessary work required to bring the system into operating condition. The project also involved arranging the equipment in a practical sequence so that water could move through the treatment stages in the intended order.

Selecting the right treatment approach was only one part of the work. The plant also needed proper installation and testing so that the final system could function as planned. This created a direct connection between the project requirement, the treatment technology and the execution work completed at the site.

Client Details

ACC Cement was the client for this installation in Faridabad. The project details identify the facility as an ACC Cement site that required a commercial RO plant for its water treatment requirement.

For any facility that needs treated water, the quality of the incoming source can affect the selection of the treatment process. Water may contain dissolved salts and other impurities that are not adequately addressed through simple filtration. When the intended application requires lower dissolved solids or improved water quality, reverse osmosis can become an important treatment stage.

In this project the confirmed requirement was a 3000 LPH commercial RO plant. The capacity gives the facility a defined treatment rate while the RO process provides the central treatment function. The system was therefore selected and installed around the need to process incoming water and produce treated water at the specified capacity.

The client’s requirement also highlights an important part of commercial water treatment planning. A treatment system must fit the site requirement rather than simply provide a generic filtration arrangement. Capacity, process suitability, installation conditions and operating requirements all need to work together. The successful completion of the installation reflects that project-focused approach.

Detail Information
Client ACC Cement
Project Location Faridabad
System Installed Commercial RO Plant
Executed By Netsol Water

Project Location

The project was completed at ACC Cement in Faridabad. Project location matters because a treatment plant must fit the physical and operating conditions of the site where it will be installed. Even when the treatment process remains the same, the installation approach may depend on available space, equipment positioning and the way the system connects with the site’s existing water arrangement.

Faridabad is an established industrial area and facilities operating there may require organized water treatment systems to support their operational needs. The important point for this installation is that the treatment plant had to function within the client’s Faridabad facility. The equipment therefore needed suitable placement and connection so that the water treatment process could move from raw water entry through RO treatment and onward to treated water collection.

A site-specific installation also requires attention to practical execution. Equipment must occupy an appropriate area while allowing access for operation and maintenance. Connections must be arranged correctly and the treatment train must remain easy to understand for the operating team. These considerations connect directly with the plant capacity and technology selected for the project.

Plant Capacity

Plant capacity determines how much water a treatment system can process over a given period. Choosing the correct capacity helps a facility match the treatment plant with its intended requirement.

For this project the installed plant capacity was 3000 LPH, which means 3000 litres per hour as the stated treatment capacity. The capacity provides a clear operating reference for the system and forms a central part of the project specification.

A capacity of 3000 LPH allows the plant to process water at a controlled treatment rate. In practical operation the actual output can depend on feed water conditions, operating pressure, membrane condition and other design factors.

The capacity also helps the client plan treated water production around the operating schedule of the facility. A defined treatment rate makes it easier to understand how much water the plant is intended to process during its operating hours. It also provides a useful reference during commissioning when the team checks whether the system operates according to the project requirement.

The installation of a 3000 LPH RO plant therefore addressed the project’s central capacity requirement while providing the treatment technology needed to reduce dissolved impurities from the incoming water.

Specification Value
Plant Capacity 3000 LPH (Litres Per Hour)
Treatment Technology Reverse Osmosis (RO)
Output Streams Permeate (Treated Water) and Reject
Key Influencing Factors Feed water conditions, operating pressure, membrane condition

Treatment Technology

Treatment technology determines how the plant converts incoming water into water with improved quality. For this project the selected technology was Reverse Osmosis, commonly known as RO. The technology is widely used where water contains dissolved salts and other substances that need to be reduced through membrane separation.

The installed system was designed around RO treatment at a stated capacity of 3000 LPH. To understand how the plant supports the client’s requirement, it helps to look at the basic working principle of reverse osmosis and how it fits into a complete treatment sequence.

1. Reverse Osmosis Process

Reverse osmosis uses pressure to push feed water through a semi-permeable membrane. This membrane has very small passageways that allow water molecules to move through while restricting many dissolved substances. The result is a treated water stream known as permeate and a separate stream that carries the rejected portion of the feed.

The RO membrane does not work as a simple sieve for visible particles. Its main purpose is to reduce dissolved substances through membrane separation. For this reason the feed water generally needs suitable conditioning and filtration before it reaches the membrane.

The treatment result depends on the quality of the incoming water and the way the RO system operates. Pressure, membrane condition, feed composition and operating controls all affect the treatment process. A properly installed system provides the operating structure needed to keep these factors within the intended design range.

2. Role of Pretreatment

Pretreatment supports RO membrane operation by reducing materials that could damage, block or foul the membrane. In a typical RO system the feed water passes through appropriate filtration and conditioning stages before reaching the membrane assembly.

3. Membrane Separation

Once conditioned feed water reaches the RO membrane under pressure, the membrane separates the water into a permeate stream and a reject stream. The permeate becomes the treated water produced by the system. The reject carries the concentrated portion of substances retained by the membrane.

This separation stage forms the core of the treatment process. It is also one of the main reasons why RO plants are selected for water treatment requirements that involve dissolved impurities.

Influent Characteristics

Understanding incoming water quality is important before operating any RO plant because membrane performance depends on the nature of the feed water. Factors such as dissolved solids, hardness, turbidity, iron and biological content can influence pretreatment needs and membrane operation. A proper design normally uses water analysis to determine the treatment arrangement and operating conditions.

1. Importance of TDS

Total Dissolved Solids, or TDS, indicates the concentration of dissolved substances in water. RO systems are commonly used when the treatment objective includes reducing dissolved solids. The difference between feed water TDS and treated water TDS can also serve as an important operational indicator during plant monitoring.

2. Hardness and Scaling

Hardness can affect RO operation because certain dissolved minerals may form deposits on membrane surfaces under suitable conditions. Scaling can reduce membrane performance and increase cleaning requirements. This is one reason why feed water characteristics matter when preparing the treatment process.

3. Turbidity and Suspended Matter

Turbidity indicates the presence of suspended material that makes water appear cloudy. These materials can interfere with downstream membrane operation when the feed receives insufficient pretreatment. Appropriate filtration helps reduce the load reaching the RO membrane.

4. Other Feed Water Parameters

Iron and microbial content can also influence treatment design. High iron levels may create deposits while biological growth can affect membrane surfaces and system hygiene. The actual significance of these parameters depends on the measured feed water quality.

Feed Water Parameter Relevance to RO Operation
TDS (Total Dissolved Solids) Indicates concentration of dissolved substances; key monitoring indicator
Hardness May cause scaling/deposits on membrane surfaces
Turbidity Suspended material that can interfere with membrane operation
Iron High levels may create deposits
Microbial/Biological Content Can affect membrane surfaces and system hygiene

Treatment Process

A proper treatment sequence ensures that each stage prepares the water for the stage that follows it. In an RO plant the process usually begins with raw water feeding and moves through filtration and membrane treatment before treated water is collected. The precise arrangement depends on the design and feed water conditions. For the installed plant at ACC Cement the treatment technology is reverse osmosis with a treatment capacity of 3000 LPH.

1. Raw Water Entry

The treatment journey starts when incoming water enters the plant. The feed water carries the dissolved and suspended constituents that the treatment system needs to manage. The raw water feed arrangement provides a controlled supply to the treatment train.

A stable feed is important because the downstream stages need water within their intended operating range. Consistent flow also helps the plant move through the treatment stages in an organized manner.

2. Pretreatment and Filtration

Before water reaches the RO membrane, the system normally reduces suspended solids and other contaminants that could affect membrane operation. Filtration helps protect the membrane by lowering the amount of material that reaches the high-pressure stage.

3. Pressure Feed to RO

After suitable pretreatment, the feed water enters the RO stage under pressure. The pressure enables water to pass through the semi-permeable membrane against the natural direction of osmosis.

This stage requires controlled hydraulic conditions so that the membrane can perform its separation function. The high-pressure section therefore forms an essential link between pretreatment and final treated water production.

4. Membrane Separation

At the RO membrane the feed stream separates into permeate and reject. The permeate contains water that has passed through the membrane while the reject contains a greater concentration of the substances that the membrane has held back.

The permeate then moves toward treated water collection. The reject stream follows the system’s designated reject handling arrangement.

5. Treated Water Collection

The treated water produced by the membrane reaches the collection side of the system. This stage marks the completion of the main RO treatment sequence.

The treatment journey can therefore be viewed as a linked process in which raw water enters the system, receives suitable conditioning, passes through pressure-driven membrane separation and emerges as treated water at the plant’s specified capacity.

Stage Function
Raw Water Entry Controlled supply of incoming feed water to the treatment train
Pretreatment and Filtration Reduces suspended solids/contaminants before RO membrane
Pressure Feed to RO Applies pressure to push water through the semi-permeable membrane
Membrane Separation Splits feed into permeate (treated) and reject streams
Treated Water Collection Collects the final treated water (permeate) output

Major Equipment

Equipment selection has a direct effect on how a treatment plant operates because every component must support the treatment sequence. A well-organized plant uses equipment that moves water through the process in a controlled manner while supporting routine operation and maintenance.

1. Feed and Water Transfer Arrangement

The feed section moves incoming water toward the treatment stages. This part of the system provides the initial connection between the site’s water supply and the RO plant. Controlled water movement helps maintain a stable treatment sequence.

2. Filtration Arrangement

Filtration forms the protective stage before RO treatment. It helps remove or reduce suspended material that could otherwise reach the membrane section.

3. High-Pressure Pump

The RO membrane requires pressure for the separation process. A high-pressure pump supplies this operating pressure to the feed stream before membrane treatment. Its role is essential because membrane separation cannot proceed in the required manner without suitable pressure.

4. RO Membrane Assembly

The membrane assembly performs the main separation function. It receives pressurized feed water and separates the flow into permeate and reject. This component represents the core of the reverse osmosis process and directly supports the plant’s water treatment objective.

5. Control and Monitoring Arrangement

An RO system also needs a control arrangement that allows the operator to start, stop and monitor the plant. Monitoring supports stable operation by helping the operator observe important process conditions.

6. Treated Water and Reject Connections

The final part of the system requires suitable connections for treated water and reject streams. These connections help direct each water stream to its intended destination and keep the process flow organized.

Together these functional components form the treatment framework needed to operate the commercial RO system at the specified 3000 LPH capacity.

Equipment Role in the Treatment Sequence
Feed and Water Transfer Arrangement Connects site water supply to the RO plant
Filtration Arrangement Protective stage that removes suspended material before RO
High-Pressure Pump Supplies operating pressure required for membrane separation
RO Membrane Assembly Performs the core reverse osmosis separation function
Control and Monitoring Arrangement Enables start/stop control and process monitoring
Treated Water and Reject Connections Directs treated water and reject streams to their destinations

Installation Process

Successful installation depends on careful planning because a treatment plant must fit the site while maintaining the correct water flow between process stages. Equipment positioning, piping connections and electrical integration must all follow the intended process arrangement.

The installation at ACC Cement, Faridabad began with attention to the site location and the space available for the plant. The treatment equipment needed to occupy a suitable area that allowed the system to operate and gave operators reasonable access for routine inspection and maintenance.

Once the installation area was prepared, the equipment was positioned according to the process sequence. Proper alignment helps maintain a clear path from raw water entry through pretreatment and RO treatment to treated water collection.

The next stage involved connecting the relevant water lines so that each treatment section could receive and discharge water correctly. The feed line had to connect with the incoming water arrangement while the treated and reject streams required their corresponding outlets.

Electrical connections also formed an important part of the installation because the pumps and control arrangements require a reliable power connection for operation. The installation team needed to ensure that the electrical system matched the treatment plant’s operating arrangement.

After the main connections were completed, the system required inspection before commissioning. The team could then move from physical installation to operational testing. This sequence reduced the risk of starting the plant before the basic installation work was complete.

The complete installation process therefore connected the physical equipment with the site’s water and power arrangements and prepared the system for controlled commissioning.

Plant Commissioning

Commissioning confirms that an installed treatment plant can operate as intended. It provides an opportunity to test the water flow, equipment response and treatment sequence before the plant enters normal operation.

Following installation the RO plant was checked as an operating system rather than only as a collection of individual components. The team examined the connections and prepared the system for startup so that water could move through the treatment sequence in the intended direction.

During commissioning the feed arrangement was checked to ensure that water could enter the plant correctly. The treatment stages were then reviewed while the system was brought into operation. The pressure stage and membrane section required particular attention because these components directly support the RO process.

The team also needed to observe the treated water path and confirm that the system separated the permeate and reject streams correctly. Any leakage, incorrect connection or abnormal operating response could be identified during this stage and corrected before regular operation.

Commissioning also provides a basis for checking whether the plant is operating against its specified capacity. In this project the confirmed plant capacity was 3000 LPH. The commissioning stage completed the transition from installation to operation. By checking the system under working conditions the project team could confirm that the installed plant was ready to serve the client’s intended water treatment requirement.

Treated Water Reuse

Treating water creates value only when the facility can use the produced water in line with its requirements. The purpose of installing the RO plant at the ACC Cement facility was to provide treated water through the installed 3000 LPH treatment system.

From a treatment perspective, the RO system provides treated water after the membrane separation stage. The treated stream can then move to the designated collection or use point according to the facility’s operating arrangement.

Effective treated water management also depends on proper storage and distribution after treatment. The water produced by the RO plant must remain protected from contamination if the final application requires maintained quality. The treatment plant therefore represents one part of a broader water-use arrangement within the facility.

The key project outcome is the availability of an installed RO treatment system that can produce treated water at the specified 3000 LPH capacity.


Results and Performance

Project results show whether the installed treatment system has addressed the requirement for which it was selected.

The most important confirmed outcome is the successful installation of a 3000 LPH commercial RO plant at ACC Cement in Faridabad. The project established a dedicated reverse osmosis treatment system at the client’s facility and brought the plant through installation and commissioning.

From a treatment perspective the RO process provides membrane-based separation of dissolved substances from the feed water. This gives the facility a treatment route designed to improve the quality of incoming water through reverse osmosis.

The stated capacity of 3000 LPH also provides a defined treatment rate for the project. This gives the client a clear basis for planning the operation of the water treatment system and for monitoring the plant against its intended capacity.

The installation also creates an organized treatment sequence in which incoming water moves through the relevant stages before treated water reaches the collection side. Proper commissioning supports operational readiness by checking the system under working conditions.

Customer Feedback/Testimonial

Customer feedback provides useful insight into how a completed treatment project is received at the site level. It can help readers understand the practical experience of working with the installation team and the response to the completed system.

Read some interesting information for the Effluent Treatment Plant Manufacturer

Conclusion

A well-planned water treatment system can help industrial and commercial facilities manage their water quality requirements through a process suited to their actual needs. The successful installation of the 3000 LPH RO plant at ACC Cement in Faridabad shows the practical value of selecting a defined treatment capacity and implementing the system with proper installation and commissioning.

Businesses that need a commercial RO system should begin with a clear understanding of their water source, treatment objective and required capacity. These factors help determine the appropriate treatment approach and support better planning for installation, operation and maintenance.

Netsol Water provides commercial and industrial water treatment solutions for different water treatment requirements. As a commercial RO plant manufacturer in Faridabad, Netsol Water can support clients who are evaluating RO-based treatment systems for their facilities.

Every water source has its own characteristics and every facility has its own treatment requirement. Businesses looking for a 3000 LPH RO system or another commercial water treatment capacity can discuss their requirement with Netsol Water to understand the suitable treatment approach.

For more information about commercial RO plants, plant capacity selection and installation requirements, contact Netsol Water and request a consultation for your specific water treatment application.

Contact

Phone: +91-9650608473

Email: enquiry@netsolwater.com
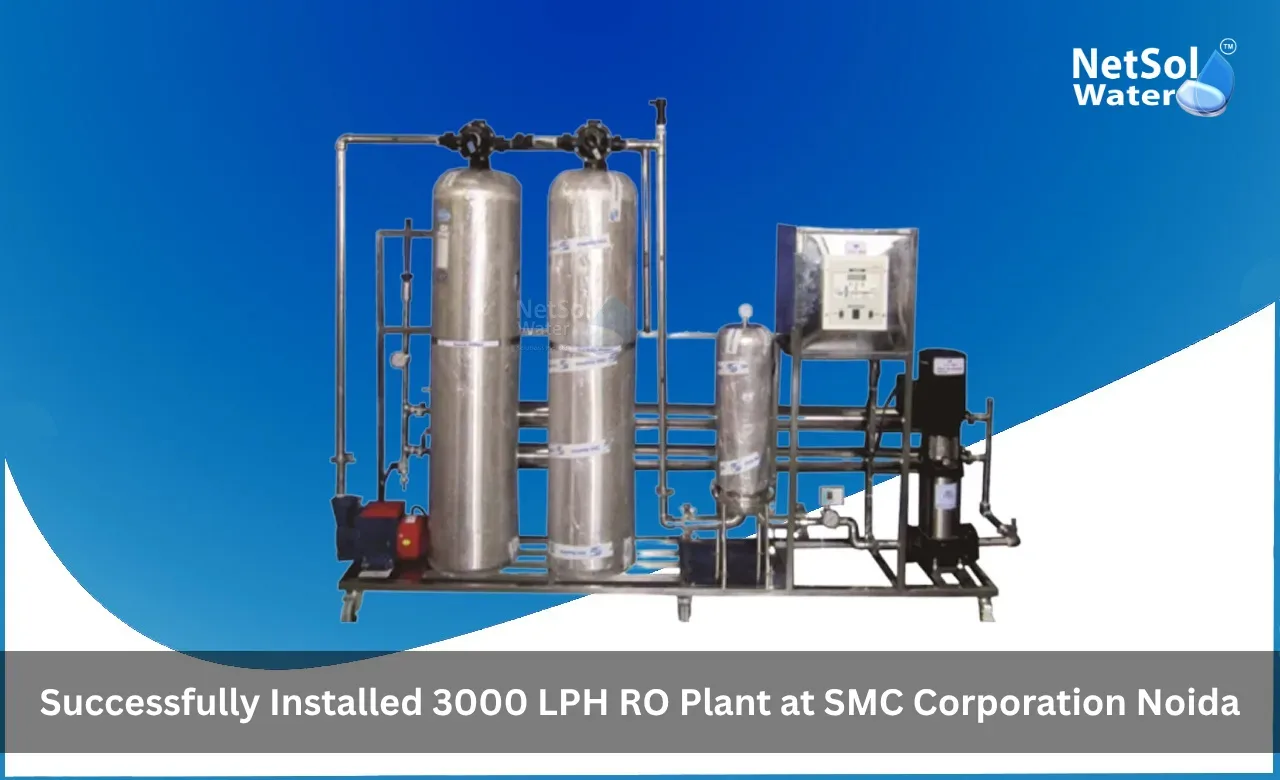

Successfully-Installed-3000-LPH-RO-Plant-at-SMC-Corporation-Noida.webp

August 25, 2026by Netsol Water

Successfully Installed 3000 LPH RO Plant at SMC Corporation Noida

Reliable water treatment plays an important role in facilities where a regular supply of suitable-quality water is needed for day-to-day operations. For SMC Corporation in Noida, the requirement was to install a commercial RO plant that could provide treated water at a suitable operating capacity. To meet this need, Netsol Water completed the installation of a 3000 LPH RO plant at the client’s Noida facility.

Netsol Water is a leading water and wastewater treatment company in the Noida region. The company manufactures commercial and industrial RO plants in different capacities and provides design, installation and commissioning support for water treatment projects.

The project focused on providing SMC Corporation with an RO-based water treatment solution that could support its operational water requirements. A properly selected RO system helps reduce dissolved impurities from feed water and produces treated water for suitable applications. The 3000 LPH capacity also provided a defined treatment rate for the facility. This project shows how a Commercial RO Plant Manufacturer in Noida can support a commercial facility through planned system selection, installation and commissioning.

Project Overview

A commercial water treatment project requires more than the supply of an RO machine. The treatment capacity must match the intended demand and the system must fit the available facility and operating conditions. The installation at SMC Corporation was planned around these basic requirements.

The project involved the installation of a 3000 LPH Reverse Osmosis plant at SMC Corporation in Noida. The main objective was to provide a dedicated water treatment system that could process incoming water and produce treated water through the RO process. The selected capacity gave the facility a treatment output of up to 3,000 litres per hour under the rated operating conditions of the plant.

The scope of the project centred on the installation of the RO treatment plant and the activities required to bring the plant into operation. This included positioning the treatment equipment, completing the required connections and carrying out testing before regular operation. Since water treatment performance depends on correct installation as well as the treatment process itself, the project required attention to both equipment setup and commissioning.

Netsol Water‘s commercial RO systems are offered across a wide range of capacities. Its published commercial RO range includes systems from small commercial units to much larger installations. The 3000 LPH plant selected for this project therefore formed part of a broader commercial water treatment capability.

Client Details

SMC Corporation is the Indian subsidiary of SMC Corporation Japan and operates in the field of pneumatic and automation technology. SMC India was incorporated in 1995 and has its head office at A-4, Sector-88, Noida. The company operates manufacturing facilities in India and maintains a network that supports its industrial customers.

The Noida facility provides an industrial setting where a dependable utility water supply can support normal facility operations. In such an environment, water quality must be considered when selecting a treatment system because untreated water may contain dissolved salts, suspended matter or other impurities that make it unsuitable for a specific application.

The project information available for this installation does not provide detailed information about SMC Corporation‘s exact end use of the RO water. Therefore, it would not be correct to assign a specific application such as drinking, process water, boiler feed or cleaning water without supporting documentation. The confirmed requirement was the installation of a 3000 LPH RO plant at the client’s Noida facility.

With the client requirement established, the location became an important part of the project planning and execution.

Project Location

The project was carried out at SMC Corporation, A-4, Sector-88, Noida. SMC Corporation‘s official corporate information identifies this address as its Noida head office and factory location.

Noida is a major industrial and commercial area within the Delhi-NCR region. An industrial facility in this setting may have continuous utility requirements and limited tolerance for interruptions in essential services. Water treatment equipment must therefore be installed in a way that suits the available site and allows the system to operate as intended.

The project location also offered a practical advantage for Netsol Water because the company operates in Noida and the wider Delhi-NCR region. Netsol Water is a water and wastewater treatment company and provides commercial RO solutions for customers in the region.

With the site and facility requirements understood, the next consideration was choosing a treatment capacity that matched the intended demand.

Plant Capacity

Plant capacity determines how much water a treatment system can process within a given period. Selecting an appropriate capacity helps ensure that the system can support the required water demand without being significantly undersized or unnecessarily oversized.

For this project, Netsol Water installed a 3000 LPH RO plant, where LPH means litres per hour. At its rated capacity, the system is designed to treat up to 3,000 litres of feed water per hour. If operated continuously at its rated flow, this corresponds to a theoretical gross treatment throughput of 72,000 litres over 24 hours. Actual daily production can vary according to operating hours, feed-water conditions, recovery, membrane performance, cleaning cycles and other plant conditions.

Parameter Value
Rated Capacity 3000 LPH (Litres Per Hour)
Theoretical Gross Throughput (24 hrs continuous) 72,000 litres


The 3000 LPH specification provided SMC Corporation with a defined treatment capacity for its facility. It also established a clear operating benchmark for the installed equipment.

Netsol Water‘s published commercial RO range includes capacities from 50 LPH to 10,000 LPH and beyond for larger requirements, showing that commercial systems can be selected according to the expected water demand.

Capacity alone, however, does not determine treatment performance. The quality of the incoming water and the selected treatment technology also influence the design.

Treatment Technology

Reverse Osmosis is widely used when a water treatment system needs to reduce dissolved salts and other impurities from water. The process uses pressure to push feed water through a semi-permeable membrane. Water passes through the membrane while a significant portion of dissolved substances and other contaminants remains in the reject stream.

For the SMC Corporation project, the selected technology was Reverse Osmosis. The basic purpose of the RO stage was to convert incoming feed water into treated water through membrane-based separation.

1. Reverse Osmosis Working Principle

The RO process starts when feed water reaches the membrane under pressure. The pressure must be sufficient to overcome the natural osmotic pressure of the feed water. As the pressurised water moves across the membrane surface, water molecules pass through the membrane while many dissolved salts and other unwanted substances are retained.

This process makes RO different from simple filtration. A conventional filter mainly removes suspended particles based on their physical size. RO also addresses many dissolved impurities that cannot be removed through ordinary mechanical filtration.

Netsol Water explains that its RO plants use membrane treatment to reduce impurities from incoming water and produce purified water.

2. Importance of Pretreatment

RO membranes need suitable feed-water conditions to maintain performance. Suspended particles, excess turbidity, chlorine and other substances can affect membrane life and operating efficiency. For this reason, commercial RO plants commonly use suitable pretreatment before water reaches the RO membrane.

The exact pretreatment arrangement installed at SMC Corporation has not been provided in the available project information. Therefore, specific filter models, dosing arrangements, membrane models or chemical treatment values cannot be confirmed for this project. The treatment discussion remains focused on the confirmed RO technology and the normal role of pretreatment in protecting the membrane.

Influent Characteristics

Understanding the incoming water quality is an important part of RO system planning. Water sources can contain different levels of dissolved solids, hardness, turbidity, iron, organic matter and microbial content. The treatment design should consider these characteristics before the equipment is selected and commissioned.

For this project, no detailed feed-water laboratory report or exact influent values have been provided. There are therefore no confirmed project-specific figures for TDS, hardness, turbidity, iron, pH or microbial load that can be reported.

The absence of these figures does not change the purpose of the installed RO system. Rather, it means that the case study should not assign numerical values that have not been documented. In a normal RO design process, these parameters help determine pretreatment requirements, membrane selection, operating pressure and expected performance.

The incoming water first needs suitable conditioning so that it can enter the membrane stage under appropriate conditions. From there, the treatment process can continue toward the production of treated water.

Treatment Process

A successful RO installation depends on a properly arranged treatment sequence. Each stage supports the next by preparing the water for the following treatment step. This reduces the load placed on the RO membrane and supports stable operation.

1. Raw Water Entry and Pretreatment

The treatment journey begins when raw or feed water enters the treatment system. Before the water reaches the RO membrane, the system normally prepares the feed through pretreatment. This stage can remove suspended matter and reduce substances that may create problems for the membrane.

The exact pretreatment equipment used at SMC Corporation has not been specified in the project details. However, the principle remains the same. Water must reach the membrane in a condition suitable for RO operation.

2. Pressure and Membrane Treatment

After the necessary pretreatment, feed water moves toward the high-pressure section of the RO system. The pump provides the pressure needed to drive water through the semi-permeable RO membrane.

The membrane separates the incoming stream into two paths. The permeate contains the water that passes through the membrane. The reject stream carries a higher concentration of retained dissolved substances and does not form part of the treated-water output.

3. Treated Water Collection

The permeate then moves toward the treated-water collection or subsequent use point. The final arrangement depends on the site’s piping and storage configuration.

This sequence provides a clear connection between the raw water source and the treated-water output. Proper operation of each stage helps the plant maintain the intended treatment function.

Major Equipment

Proper equipment selection supports consistent plant operation. An RO plant needs several components to move water, condition the feed, apply pressure and carry out membrane separation.

For this project, the confirmed major treatment equipment is the 3000 LPH RO plant itself. The plant includes the RO treatment assembly required to process feed water at its rated capacity. Netsol Water‘s commercial RO systems commonly use components such as membranes, high-pressure pumps, pressure vessels, control panels and dosing pumps, depending on the plant configuration.

Equipment Function
RO Membrane Assembly Performs the main separation process. It allows water to pass through under pressure while retaining a substantial portion of dissolved impurities.
High-Pressure Pump Provides the pressure needed for membrane separation. Its operation is directly linked to maintaining the pressure conditions required by the RO process.
Control Panel Helps the operator manage the plant and monitor its operating sequence. The exact control philosophy and automation level installed at SMC Corporation have not been provided.
Pretreatment and Supporting Components Protects the RO membrane and helps prepare the feed water. The specific filter vessels, dosing units, valves and instruments used for this project are not documented in the information available.


As a result, no unverified equipment list is presented as a project fact.

Installation Process

Plant installation requires careful planning because the equipment must fit the site while maintaining proper connections between the different treatment stages. The work should also allow operators to access the system for normal inspection and maintenance.

The installation at SMC Corporation involved placing the 3000 LPH RO system at the client’s Noida facility and preparing it for operation. The equipment had to be positioned appropriately before the required piping, water connections and electrical connections could be completed.

Once the equipment position was established, the installation team could connect the treatment sections so that water could move through the intended process. Electrical and control connections were also required to prepare the plant for testing.

The final stage of installation involved checking the physical setup and confirming that the system was ready for commissioning. This step was important because a treatment plant must be mechanically and electrically prepared before performance testing can begin.

Plant Commissioning

Commissioning confirms whether an installed treatment system is ready for regular operation. It provides an opportunity to check the plant under operating conditions and identify installation issues before the system enters normal service.

After installation, the RO plant was prepared for testing and commissioning. The commissioning process involved checking the operating sequence and confirming that the equipment could function as intended. Water movement through the treatment system had to be verified along with the operation of the principal components.

The commissioning stage also provided an opportunity to observe the plant’s treatment behaviour at its intended operating capacity. A proper commissioning process helps confirm that the system is connected correctly and that the plant can move from installation into routine operation.

The available project information does not include detailed commissioning readings such as recovery percentage, feed pressure, permeate TDS or hourly production records. These figures have therefore not been added to the project results.

Treated Water Reuse

Treating water becomes more useful when the resulting water can support an appropriate application within the facility. RO-treated water can be directed to a designated use point depending on the quality requirement and the site’s internal water management arrangement.

For the SMC Corporation project, the confirmed scope establishes the installation of a 3000 LPH RO plant but does not specify the exact final use of the treated water. It would therefore be inappropriate to state that the water was used for a particular process without supporting information.

The practical value of the system lies in creating a dedicated source of treated water for the client’s identified requirement. When used appropriately, such a system can help provide greater control over the quality of water supplied to the intended application.

Results and Performance

Project results provide a practical measure of whether the installed system met its intended purpose. In this installation, the major confirmed outcome was the successful installation and commissioning of a 3000 LPH RO plant at SMC Corporation‘s Noida facility.

The system established a dedicated RO-based treatment capacity of 3,000 litres per hour. This provided the client with a defined water treatment system rather than depending only on untreated incoming water for the relevant requirement.

The treatment technology also created a process for reducing dissolved impurities through membrane separation. Netsol Water identifies RO as one of its core commercial water treatment solutions and offers commercial systems in different capacities for varied applications.

No project-specific laboratory figures, before-and-after water quality results or long-term operating data were provided. The performance discussion is therefore limited to the confirmed installation, capacity and successful movement of the plant into operation. This approach keeps the project record factual and avoids presenting unverified performance claims.

Customer Feedback/Testimonial

Customer feedback helps demonstrate how a completed project performs from the client’s perspective. It can also provide useful information about installation quality, plant operation and overall project satisfaction. The 3000 LPH RO plant was successfully installed at the specified Noida facility and taken through the required commissioning stage.

Read some interesting information for the Industrial RO Plant Manufacturer in Gurgaon

Call to Action

Netsol Water‘s completed installation at SMC Corporation shows how a properly selected RO system can provide a dedicated water treatment solution for a commercial facility. The project combined a defined treatment capacity with membrane-based purification and onsite installation support. Netsol Water operates from the Noida region and provides commercial RO systems in a range of capacities for different water treatment requirements.

Businesses looking for a Commercial RO Plant Manufacturer in Noida can consult Netsol Water to discuss their feed-water source, treatment capacity and application requirements. A suitable system should always be selected after understanding the site’s water quality and expected demand rather than simply choosing a standard capacity.

Netsol Water is the leading commercial RO plant manufacturer, supplier and exporter based in Noida, according to its published company information, and provides commercial RO systems across a broad capacity range.

For organisations planning a new RO installation or upgrading an existing water treatment system, professional consultation can help define the right treatment approach. Contact Netsol Water to discuss your requirement and request a suitable commercial RO plant solution for your facility.

Contact Netsol Water at:

Contact Details
Phone +91-9650608473
Email enquiry@netsolwater.com


What-are-the-Applications-of-Commercial-Water-Softeners-3.webp

August 17, 2026by Netsol Water

Successfully Installed 1000 LPH Commercial RO Plant at Skylark, Gurgaon

Commercial offices, infrastructure companies, manufacturing facilities, institutions and hotels need reliable access to appropriately treated water. The incoming water may have excessive dissolved salts, hardness, suspended particles or other undesirable constituents; a properly designed commercial RO system can help maintain the necessary treated-water quality. We installed and commissioned a 1000 LPH Commercial RO Plant at Skylark, Gurgaon for its production of about 1000 litres of RO treated water per hour with the specified operating conditions. The project embodies our work as a reputed Commercial RO Plant Manufacturer in Gurgaon.

Project Overview

The main goal of this project was to set up a commercial water treatment system which would produce about 1000 LPH of RO treated water at Skylark‘s Gurgaon site.

The water-treatment systems used in commercial facilities are different to those in small domestic RO units. The equipment should be able to process greater flow rates, operate longer hours and process different feed-water characteristics, and be easy to operate and maintain.

The treatment system was designed for a 1000 LPH commercial RO plant with appropriate pre-treatment stages for this project. The goal was to not only install RO membranes, but to design an entire treatment sequence that would safeguard the membranes and ensure consistent output.

The overall work involved in the installation comprised assessment of the area, equipment planning, plant fabrication and assembly, plant transportation, positioning of the plant equipment, plant plumbing connections, electrical connections, plant pretreatment setup, plant RO membrane installation, testing, plant flushing, plant trial operation and final plant commissioning.

The final product was a water-treatment system that satisfied the commercial need of Skylark with a convenient access path for future inspection and maintenance of the major components of the system.

Client Details

The project was for Skylark, Gurgaon as a client. It has EPC, mining, toll collection and highway maintenance as its major business segments.

The company’s operations feature large-scale infrastructure activities, and a significant employee base. Such an organisation needs reliable utility services capable of supporting the normal running of business.

One of these utilities is water-treatment infrastructure. An appropriate size commercial RO plant can process water at a central location, and the purified water can be stored for use as required at the facility, rather than using small purification units.

Thus the 1000LPH Commercial RO Plant was selected which proved to be a good solution for the site with a relatively small footprint for the system.

Project Location

The RO plant installed at Skylark, Gurgaon, Haryana. Their address in Gurgaon is: 267, Udyog Vihar, Phase IV, Gurgaon – 122015, Haryana, India.

One of the prominent commercial and industrial hubs of Gurgaon, Udyog Vihar is home to offices, manufacturing units, warehouses and corporate establishments in the various stages.

Water supply to commercial establishments in Gurgaon may be from various sources and the water quality may vary depending on the source and local conditions. Therefore, it is best to choose the water-treatment equipment based on the water’s feed-water quality, not just on the basis of its LPH rating.

Therefore, as a Commercial RO Plant Manufacturer in Gurgaon, our emphasis is on the capacity of the RO Plant and the number of treatment stages that will be required for a particular application as well as the quality of the water source.

Plant Capacity

The commercial RO system installed has a product water capacity of:

Parameter Value
Product Water Capacity 1000 Litres Per Hour (LPH)


This implies it is capable of delivering about 1,000 litres per hour of RO water under the plant’s operating and feed-water conditions.

Capacity must be determined based on a number of considerations such as:

Capacity Consideration
Daily treated-water requirement
Peak water demand
Number of operating hours
Available raw-water storage
Treated-water storage capacity
Feed-water quality
Membrane performance
Required product-water characteristics


A theoretical yield can be calculated: For a 1000 LPH plant, if it is able to work for 8 hours, then the theoretical output is about 8,000 litres. The theoretical production at the same time of effective operation is about 10,000 litres.

The actual production may change depending on the feed-water temperature, pressure, condition of the membrane, concentration of dissolved-solids, fouling, maintenance and other operating conditions.

This means that Skylark is able to deliver commercial scale water production with a 1000 LPH capacity, but not with a much larger treatment plant.

Treatment Technology

The key purification technology applied in the project is Reverse Osmosis (RO) together with the appropriate pre-treatment.

Reverse osmosis is a pressure driven membrane separation process. The water is pushed across a semi-permeable membrane, creating product water or permeate and reject water or concentrate, which is a concentrated stream.

The pretreatment decreases the loading rate on the membranes, fine filtration gives further protection against particulates, the high-pressure pump creates the pressure for membrane separation, and the RO membranes decrease the concentration of dissolved material in the product-water stream.

The plant can be systematically maintained and a practical solution for commercial water treatment is possible.

Influent Characteristics

An RO plant‘s performance is highly dependent upon the properties of the influent, or raw water entering the plant.

For commercial RO systems, some key feed-water parameters that are normally considered in designing and operating systems are:

Influent Parameter
Total Dissolved Solids (TDS)
Total hardness
Calcium and magnesium
Turbidity
Suspended matter
pH
Chloride
Alkalinity
Iron, where present
Hard Minerals (Silica, etc.)
Organic matter
Microbiological Condition


Treatment Process

The 1000 LPH Commercial RO Plant consists of a series of treatment units that work together in a coordinated manner.

1. Raw-Water Feeding

Raw water is initially delivered to the pretreatment part by the feed line. Flow of feed is essential as subsequent equipment relies on a steady supply of feed water.

2. Pressure/Media Filtration

The primary filtration section filters out suspended impurities and turbidity.

Particulate loading is reduced at this stage which leads to less loading of fine filters or RO membranes.

3. Activated Carbon Treatment

Activated carbon treatment is available to remove chlorine, odour and some organic material in feed water if needed.

Granular activated carbon is widely utilised in water treatment applications for the adsorption of taste and odour-causing compounds and a number of organic contaminants.

4. Antiscalant Dosing

If scaling has the potential to occur, controlled antiscalant dosing can decrease the growth of mineral deposits on membrane surfaces.

As scaling builds up it can decrease membrane output, increase differential pressure, and over time increase maintenance needs.

5. Micron/Cartridge Filtration

Water flows through fine cartridge filtration before going to the high pressure RO section.

This provides another protection to keep small suspended particles away from the membrane elements.

6. High-Pressure Pumping

This high-pressure pump raises the water pressure to the amount necessary for a good reverse osmosis.

The RO process is dependent on pressure and requires it to push water through the semi-permeable membrane.

7. RO Membrane Separation

Water is split into two streams in the membrane housings.

These are referred to as RO permeate, which flows through the membrane at much lower levels of many dissolved substances.

The second is the concentrate or reject stream that contains more of the substances that are rejected by the membrane.

The EPA also explains RO as generating a permeate/product water stream and a reject/concentrate stream.

8. Treated-Water Collection

The RO permeate is finally channeled to the intended treated water storage facility for distribution and use.

Major Equipment

Skylark Gurgaon‘s 1000 LPH Commercial RO Plant features all necessary equipment needed for a commercial water treatment system.

The main functional elements are:

Equipment
Raw-water feed arrangement
Feed-water pump
Pressure/media filtration system
Activated carbon filtration is used
Antiscalant dosing system
Micron cartridge filter
High-pressure pump
Commercial RO membrane elements.
Membrane pressure housings
Pressure gauges
Product-water flow monitoring
Reject-water flow monitoring
TDS/water-quality monitoring arrangement
Control panel
Valves and inter-connections pipelines
Treated-water outlet arrangement
Reject-water discharge arrangement


Equipment was set up both to be functional and accessible.

Maintenance or inspection of parts such as filter elements, dosing equipment, membrane housings, pumps and instruments requires regularity, particularly in a commercial RO plant, where accessibility is of paramount importance.

A quality commercial RO system should therefore be capable of yielding treated water, but also be designed to serve a long time.

Installation Process

The installation process was systematically conducted so that the RO plant is able to function after its commissioning.

A review of the available installation area and the selection of suitable locations for the RO skid and pretreatment equipment was the first step.

Wherever possible, working space was kept clear around the treatment units to enable routine changes of the filters, pressure checks and maintenance to be carried out conveniently.

Post equipment positioning, the raw water line was hooked up to the feed section and interconnections between the pretreatment components and the RO system were made.

The product-water piping and reject-water piping were not connected to each other so as to avoid mixing of the two streams.

Electrical connections to the feed pump and the high-pressure pump were then made, along with the feed pump, dosing system and control panel.

The installation team preperformed the following checks before starting the plant:

Pre-Startup Check
Pipe connections
Valve positions
Electrical connections
Pump direction
Filter installation
Membrane housing connections
Pressure lines
Conveying product and reject outlets
Potential leakage points


The process of installation was systematic which facilitated controlled startup and commissioning of the system.

Plant Commissioning

Commissioning of plants is the point where the installed equipment is tested as a whole water-treatment system.

Firstly, the 1000 LPH RO plant was flushed to prepare the filtration section and membrane section for normal operation.

Feed pump was then operated and then low pressure section was started in a controlled way.

The technical team was monitoring the operating condition such as feed-flow, pressure, product-water generation, reject-water discharge etc. during the commissioning.

Leaks were tested and the pressure and operation of the pumps were monitored for any abnormality.

The plant was slowly ramped up to operating conditions to avoid unnecessary hydraulic stressing of the plant.

The treated water production rate was verified against the desired plant capacity of 1000 LPH

There was also basic operational guidance provided in the commissioning process, such as:

Operational Guidance Topic
Plant startup
Plant shutdown
Pressure observation
Product-water monitoring
Cartridge-filter replacement
Chemical dosing
Membrane maintenance
The detection of abnormal flow and/or pressure.
Preventive maintenance requirements


Following successful testing and adjustment, the plant was made ready for routine operation.

Treated Water Reuse

The treated water from the plant can be stored in a separate treated water tank until such treated water is required for Skylark‘s own water usage.

Depending on the quality needed for each application, treated water can be used for:

Treated Water Use
After required final treatment and verification, drinking-water supply.
A full pantry and kitchen will be supplied.
A well-equipped kitchen and pantry will be provided.
Office utility requirements
Appropriate equipment or process applications
Other purposes with relatively lower TDS water


The actual end use should always determine the required final water-quality specification.

If treated water is to be used for human consumption, then hygienic storage and disinfection as required, and routine laboratory testing should be observed. IS 10500:2012 specifies requirements for drinking water in India, which can be used to evaluate the water quality parameters relevant to it.

The reject water from RO system should be disposed properly. The EPA states that the concentrate stream will include salts and other materials that are trapped by the membrane, and therefore, should be treated appropriately before being discharged or managed.

Only the reject water’s quality and the needs of the intended non-potable use should be taken into account when considering possible reuse.

Results and Performance

The successful installation and commissioning of the 1000 LPH Commercial RO Plant at Skylark Gurgaon has enabled the facility to have a dedicated on-site water-treatment system which can provide about 1,000 litres of RO water per hour under its specified operating conditions.

The project was successful in achieving the project objective of having a stable commercial scale production of treated water using a structured pretreatment and membrane-separation process.

The main results are:

Result Description
Well defined treated water production The plant offers treated water as a separate source of water rather than relying only on smaller point-of-use water purifiers.
Commercial scale capacity A rated capacity of 1000 LPH is considered a reasonable scale of production/capacity to install.
Removal of dissolved mineral content RO Membrane technology is used specifically for the removal of a variety of inorganic constituents and dissolved solids.
Pretreatment for membrane protection Proper filtration prior to the RO stage can minimise fouling and plugging, which are known operational issues of membrane treatment.
Easy system monitoring Pressure monitoring points, flow monitoring points and water-quality monitoring points allow system operators to monitor plant operation during regular operation.
Sustainable equipment layout System installed to allow convenient access to consumables and major equipment needing routine maintenance.


This overall installation thus provides both 1000LPH purification capacity and a complete commercial treatment solution including pretreatment, membrane separation, monitoring and the collection of treated water.

Customer Feedback / Testimonial

Installing and commissioning processes were executed professionally, keeping in mind operational ease and system reliability.

After commissioning, basic maintenance and operation of the plant was demonstrated to the concerned personnel.

As a result of not having received an independently verified customer quotation for this case study a direct statement must not be attributed to Skylark without permission.

The installation and commissioning of the 1000 LPH Commercial RO Plant in our Gurgaon facility is done professionally and the plant is functioning well as per our water treatment requirement and the technical team gave us proper guidance about the operation and routine maintenance of this plant.

Looking for a trustworthy Commercial RO Plant Manufacturer in Gurgaon for your office, factory, hotel, school, hospital, warehouse, commercial complex or industrial plant?

Some of the points to consider in a well-designed system:

Design Consideration
Raw-water quality
Daily water requirement
Peak demand
Required treated-water quality
Available operating hours
A space that allows for the installation of equipment.
An area that can accommodate equipment.
Pretreatment requirements
Water storage
Maintenance requirements
Intended treated-water application


We supply complete solution from the designing to manufacturing, installation and commissioning of RO Plant for Commercial applications in Gurgaon for various capacities.

Commercial RO plant can be designed in various capacities like:

Available Capacities
500 LPH
1000 LPH
2000 LPH
3000 LPH
5000 LPH
10,000 LPH and customised capacities


Our services include water-treatment requirement assessment, system design, equipment selection, RO plant manufacturing, installation, commissioning, operator guidance, membrane replacement, filter replacement, troubleshooting and preventive maintenance support.

Our track record of delivering water-treatment projects from conception to commissioning, such as the 1000 LPH Commercial RO Plant at Skylark Gurgaon, showcases our capabilities in delivering commercial water-treatment projects.

If you require a dependable Commercial RO Plant Manufacturer in Gurgaon, contact our technical team.

Read some interesting information for the Effluent Treatment Plant Manufacturer in Faridabad

Conclusion

The 1000 LPH (Commercial RO Plant) installed at Skylark Gurgaon is testament to the significance of selecting the right plant capacity, pretreatment, membrane technology and professional commissioning under one umbrella solution.

Skylark is an infrastructure and engineering company that has offices in EPC (Engineering, Procurement, and Construction) and other sectors such as mines, tolls, and highways.

When a commercial facility is being used, the reliability of the water treatment will not only be determined by the rated capacity of the RO plant but also by factors such as incoming water condition, pretreatment performance, proper operating pressure, membrane condition and periodic maintenance.

The 1000 LPH system meets these needs with a series of systematic treatment processes that involve raw-water feeding, pretreatment, fine filtration, high-pressure pumping, and RO membrane separation and output of product water.

While RO is an established membrane separation process for decreasing dissolved solids and a host of other contaminants, system pretreatment and concentrate management are important factors in proper system operation.

As a Commercial RO Plant Manufacturer in Gurgaon, the project has also provided another hands-on example to understand our capability to deliver commercially appropriate water-treatment systems based on capacity, water quality, and operational requirements.

For businesses planning a new RO installation or upgrading an existing treatment facility, a properly engineered commercial RO plant can provide a dependable, scalable and manageable source of treated water for long-term use.

Contact Netsol Water at:

Contact Details
Phone +91-9650608473
Email enquiry@netsolwater.com


What-are-the-Applications-of-Commercial-Water-Softeners-2.webp

August 13, 2026by Netsol Water

Successfully Installed 2000 LPH Commercial RO Plant at Boutique International, Gurgaon

Consistently treated water is important for commercial and industrial operations that rely on water consistently and continuously. The composition of raw water, including dissolved salts, hardness, suspended matter and other water properties, can vary and impact the usefulness of the raw water for drinking, utilities, processes. The combination of appropriate pretreatment with membrane purification would present an effective solution provided by a suitably designed commercial RO plant. The RO plant of 2000 LPH Commercial RO Plant was successfully installed and commissioned at Boutique International, Gurgaon and they were provided with a reliable source of treated water of about 2000 litres per hour based on the operating conditions provided.

Boutique International is a vertically integrated garment Export Company based in Gurgaon. It has knitting, embroidery, printing and other apparel manufacturing activities and is manufactured in its facility in Gurgaon.

The project reflects our expertise as a Commercial RO Plant Manufacturer in Gurgaon and most importantly, designing treatment systems as per the plant requirements, feed water quality available at the site, output capacity required and operational needs of the client.

Project Overview

The aim of the project was to supply a viable commercial scale water treatment plant for Boutique International that will produce 2,000 litres per hour of treated water.

The quantity of water required is not the only factor to consider before installing a commercial RO plant, the characteristics of the feed water must also be taken into account. RO membranes are primarily meant to separate the dissolved contaminants from water, and pretreatment is used to abate suspended particles, scaling, etc., that can impact the membrane.

Thus, it was decided that the solution will be an integrated treatment system instead of a standalone RO membrane unit. The removal of material from the raw water, generating the pressure, separation in a membrane, monitoring and treating the water out of the membrane were all taken into account, in order to ensure the plant’s operation under commercial conditions.

The project involved site assessment, capacity planning, equipment selection, system fabrication, transportation to the facility, installation, electrical and plumbing connections, flushing, trial operation, parameter adjustment and final commissioning.

The system once installed, gives Boutique International a separate RO water-treatment system of 2000 LPH for assured everyday operation.

Client Details

Boutique International is a garment manufacturing and export company from Gurgaon, Haryana, which was the client for this project.

Boutique International calls itself the star export house for apparel brands in the United States and Europe recognised by the government. The company claims its manufacturing process is vertically integrated, that is all the process from yarn to finished goods are done at the company’s facility. It has the facilities of circular knitting, flat knitting, embroidery and printing.

Infrastructure reliability is crucial in an organisation that operates at this level. All water-treatment facilities need to be able to deliver the treated water needed in the required quantity, and not make routine operation and maintenance unnecessarily complex.

The need was thus for a commercial system, not a small domestic purification system. The chosen capacity of 2000 LPH was deemed to be an appropriate balance of the water demand, operational capability and future utility.

Project Location

The commercial RO plant was installed in Boutique International, Plot No. 553, Pace City 2, Gurgaon, Haryana – 122016.

The town Gurgaon or Gurugram has emerged as a very important business and industrial hub in Delhi NCR region. The nature of water may vary greatly depending on whether it comes from a municipal water supply, a ground water well or a tanker.

So, it is not right to choose commercial RO plants only on the basis of the rated production capacity. The characteristics of the feed-water, treatment time, and pretreatment time, storage facilities, and the water quality to be expected after treatment, must also be taken into account.

As a Commercial RO Plant Manufacturer in Gurgaon, we therefore do not follow a one design fits all principle instead we ensure that the treatment configuration is personalized to fit the actual site needs.

Plant Capacity

The rated treated water production of the installed plant is: 2000L/h (Litres per Hour)

Parameter Value
Rated Treated Water Production 2000 L/h (Litres per Hour)


The system can generate around 2000 litres of RO treated water in an hour when operated at its full capacity. The actual daily production will vary depending on the operating time, feed-water condition, membrane performance, maintenance condition, and water need of the facility.

The theoretical production capacity of a 2000 LPH plant is, for example, about 16 000 litres during a period of 8 effective production hours. But the plant does not have to run around the clock—operation can be synchronized with treated-water storage and actual consumption.

The capacity selected is enough for commercial scale output, while treated water production and storage will follow the facility’s production schedule.

Treatment Technology

The RO process with the proper pre-treatment technology represents the main treatment process adopted in the plant.

Reverse osmosis is a method that uses pressure to push feed water through a special membrane to extract some of the water. This results in two streams of water, the purified water or permeate, and a more concentrated stream of water called the concentrate or reject water, which contains the dissolved substances that were not purified. RO is a membrane-separation technology capable of separating a wide spectrum of dissolved contaminants and salts.

But RO membranes should not be fed inadequately treated feed water. Scaling compounds, suspended matter, and chlorine and organics may have an impact on membrane life and performance.

Influent Characteristics

Incoming water quality is one of the most crucial factors to consider while designing any commercial RO plant.

Dissolved salt, minerals which form hardness, suspended solids, turbidity, chlorine and organic matter can be found in varying amounts in commercial feed water.

The treatment system was designed to address the key parameters, which typically affect commercial RO operation, such as:

Total dissolved solids, hardness, suspended particles, turbidity, scaling potential and contaminants that could impact the performance of the membrane.

Pretreatment is particularly important because it is not only to enhance the quality of the feed water, but to avoid fouling or scaling of RO membranes before they are used. DuPont says proper pretreatment ensures good RO performance and that the pretreatment required is a function of the chemistry of the raw water and the purpose of the treated water.

If the water is to be used for drinking, it is prudent to test its final quality with the right tests. The drinking-water specification of Bureau of Indian Standards (BIS) IS 10500:2012 suggests that the acceptable range for TDS is 500 mg/L and permissible range is 2,000 mg/L without any source. This same standard establishes acceptable hardness levels between 6.5 and 8.5, as well as limits for chloride, fluoride, nitrate and many other parameters.

BIS IS 10500:2012 Parameter Value
TDS – Acceptable Range 500 mg/L
TDS – Permissible Range (No source) 2,000 mg/L
Acceptable Level 6.5 to 8.5


Treatment Process

The 2000 LPH Commercial RO Plant is designed to pass through a series of treatment stages that help prevent damage to the membranes and assure a consistent product-water quality.

The raw water is pumped into pretreatment section first. The suspended matter is filtered out initially and the load is reduced to the later filter elements.

The water is then filtered through media filters. This stage is useful in controlling turbidity, suspended impurities, colour, odour and substances which may affect the operation of the RO membrane depending on the nature of the raw water.

When incorporated, activated carbon treatment acts as an important barrier to protect the membranes from the presence of chlorine and some of the organic compounds before they reach the membranes. This is especially important since improper feed-water conditions can adversely affect the performance of the membrane.

Fine cartridge filtration is another physical barrier to small suspended particles that is offered before membrane treatment.

A high-pressure pump is used to pump the pretreated water to the RO section. Reverse osmosis requires pressure due to the natural tendency of dissolved salts to move across a semi-permeable membrane.

The feed flows inside the RO membrane housing, splitting into a product water and a concentrate stream. Water passing through the membrane becomes the product water and continues to treated water storage, while a higher concentration reject water stream removes a significant amount of the dissolved substances separated.

During operation, flow and pressure parameters are monitored along with water quality parameters to detect any abnormal conditions and correct them.

Major Equipment

The main components needed for the pretreatment, membrane purification, monitoring and controlled operation were set up in the commercial RO system.

The major functional equipment consisted of:

Equipment
Arrangements for feeding raw water and water feeding pump.
Pressure/media filtration system
Activated Carbon Treatment, when needed based on feed-water conditions
Antiscalant dosing arrangement
Micron/cartridge filtration
High-pressure RO pump
Monitoring of product-water and reject-water flow.
Temperature and operating controls
Electrical control panel
Interconnection of piping, fittings and valves.
RO-treated-water outlet/storage connection


The equipment size was scaled to the product water requirement of 2000 LPH and operating condition.

The design also took ease of operation and maintenance into account since the installation of successful commercial water treatment relies not only on a good installation, but also regular monitoring, changing filters, maintaining membranes and timely servicing.

Installation Process

Installation started by surveying the plant space and existing utility services.

RO skid and pretreatment equipment were located for good accessibility for future maintenance and filter change out. The positioning of equipment is especially critical in commercial installations as the layout could become unnecessarily complicated to service the equipment routinely.

The inlet plumbing for raw water was connected to the pretreatment system, and connections between the treatment stages were made. Careful checks were made on the high pressure line, membrane housings, product-water outlet and reject water discharge line.

Pumping and dosing equipment and the control panel were electrically connected. The system was then checked for correct positioning of the valves, piping alignment and leaks.

With mechanical and electrical connections checked, individual system sections were ready for flushing and start-up.

Installation method – The approach was designed to reduce disruption to the client’s existing operations and provide easy access to the water-treatment equipment for future maintenance.

Plant Commissioning

Commissioning is one of the most important phases of a commercial RO project as good installation does not guarantee good operation.

The system was initially flushed to clear any loose material that may have been encountered during installation, and to ready the filters and membrane system for use.

The pumps were then gradually started and increased pressure applied in a controlled manner. The feed-water flow, product-water flow and reject-water flow were monitored as the system approached normal operating conditions.

The team inspected the system for leaks, abnormal pump performance, pressure and flow blockages during the commissioning. RO operating parameters were optimized for stable operation, while avoiding undue stress to the membranes.

The product-water output has been validated with the desired capacity of the plant, namely 2000 LPH subject to the condition of operating conditions and the quality of feed-water.

Routine startup and shut down, pressure monitoring, cartridge-filter replacement, chemical dosing, membrane cleaning indicators and preventive maintenance were also discussed with the operators.

Treated Water Reuse

The water that is treated through RO system can be stored in a separate tank, and can be pumped to specific locations where the facility needs low TDS water.

RO treated water can be used to prepare drinking water, to meet pantry needs, for utility uses and for appropriate process water needs based on the client’s internal water-management plan, where controlled dissolved-solids levels are desired.

For any end use, the distribution should be the same as the required water quality specification. If the water is used for drinking, the proper post-treatment, hygienic storage and regular microbiological and chemical testing are essential.

Concentrate management is also responsible for RO concentrate. Facilities may consider whether they can make a suitable non-potable use of the reject-water stream depending on its quality and the local needs. Testing and the needs of the intended use should be considered when making a reuse decision.

Results and Performance

The installation and commissioning of 2000LPH Commercial RO Plant at Boutique International, Gurgaon was a great success, it gave the facility its own high capacity treatment system to produce purified water there.

The main aim of the project, which was to set up a reliable RO water production system with a rated capacity of around 2000 litres per hour was achieved.

After commissioning, the stable operation of the system with controlled feed pressure, product-water generation, and reject flow were identified. The RO membrane stage achieved high removal of dissolved mineral matter from the feed water, and pretreatment prevented particulate and scaling loading of the membrane system.

The primary operational advantages of the installation are the assured commercial scale water production, reduced reliance on small-scale purification units, ability to control the availability of treated-water, improved management of the dissolved solids and hardness, and the plant configuration which allows for easy monitoring of system performance and for routine service.

RO membrane technology is a proven technology for commercial and industrial water treatment. Commercial RO membranes are utilized in a wide variety of applications, from restaurants and hotels to medical and scientific facilities.

The finished project provided Boutique International with a new facility water-treatment asset on top of its current facility infrastructure.

Customer Feedback / Testimonial

Installation was finished with special consideration for the performance of the plants, ease of access and ease of operation. The system was tested during commissioning and the operating procedures were discussed to the facility staff.

The 2000 LPH Commercial RO Plant has been installed at our facility in Gurgaon and we are pleased with the professional installation and commissioning of the RO Plant. The RO Plant is working as per our water-treatment requirement and the Technical team provided us the required support during installation, testing and handover.

In execution of this project success highlights the needs of using proper plant capacity together with proper pretreatment, reliable equipment, proper installation and technical support.

Call to Action

When it comes to selecting the best commercial RO Plant Manufacturer in Gurgaon, the decision is crucial if you have a factory, office, hotel, hospital, school, institution, warehouse or commercial facility which needs a reliable water-treatment plant.

A commercial RO system should be configured based on your specific water analysis, your daily water demand, the number of hours the system will be used, available space and the specific quality of water you want to produce—rather than just picking a capacity from a standard capacity chart.

We design, manufacture, install and commission the commercial RO plants for various water needs and operating conditions. The treatment configuration can be designed depending on the application and feed-water characteristics, if you need a 500 LPH, 1000 LPH, 2000 LPH, 3000 LPH, 5000 LPH or a customised commercial RO plant.

Available Capacities
500 LPH
1000 LPH
2000 LPH
3000 LPH
5000 LPH
Customised commercial RO plant


Services offered range from requirement assessment to designing the water-treatment system, selecting the equipment, manufacturing the RO plants, commissioning and training the operators, troubleshooting and providing equipment maintenance support and replacement of consumables and membranes.

The installation of a 2000 LPH Commercial RO plant at Boutique International, Gurgaon, showcases our capability to take on commercial water-treatment projects from system design to final commissioning.

Looking for a reliable Commercial RO Plant Manufacturer in Gurgaon? Contact us today and speak about your water requirement.

Provide us with your raw-water test report and daily water demand and our technical team will be able to suggest the capacity and treatment configuration of the RO plant required for your facility.

Read some interesting information for the Commercial RO Plant Manufacturer in Faridabad

Conclusion

The Boutique International project did not just use the RO membrane but included all the components of a complete treatment process, such as pretreatment, fine filtration, pressure generation, membrane separation, monitoring, commissioning and operational guidance. This is significant because the performance and life of the membrane is highly dependent on the quality of the water treated and the quality of pretreatment.

The system installed has a capacity of 2000 litres per hour and enables the Boutique International‘s Gurgaon facility to have a significant treatment water production capacity with the help of installed system. Reliable long term operation is also achieved through correct installation, system commissioning and equipment arrangement which is easy to access.

If any organisation is planning to install a similar RO Plant in Gurgaon, it is advisable to choose a Commercial RO Plant Manufacturer in Gurgaon to ensure that plant capacity, water chemistry, pretreatment and operational requirements are all taken care.

A business where treated water availability is a constant requirement can turn to a professionally engineered commercial RO plant for a reliable solution that is scalable and can provide them with the water they need.

Contact Netsol Water at:

Contact Details
Phone +91-9650608473
Email enquiry@netsolwater.com